Cost-Effective PCB Solutions: Choosing the Right Process
PCB cost control starts long before a quotation arrives. The process you choose fixes material spend, yield, and the amount of inspection the job needs. Many teams worry that a lower-cost route will weaken reliability, while a premium route will break the budget. In practice, the right answer depends on the application, the volume, and the performance the product truly needs. Matching the process to those three factors usually delivers both stable quality and a sensible price.
A common mistake is treating every board as if it must survive the harshest environment. That habit adds plating thickness, tighter tolerances, and extra test steps that the product never uses. Each addition raises cost and lengthens the schedule. A better approach is to define the real operating conditions first, then select materials and processes that meet them with margin. This article explains how to make that choice across standard, medium-performance, and small-batch work, and what buyers should verify before release.
Starting With Application Requirements
Begin with the environment and the duty cycle. A household appliance board sees modest heat and gentle thermal cycling. An industrial controller may face vibration, humidity, and wide temperature swings. Those differences change the material grade, the surface finish, and the layer count you should plan for. Writing the conditions down before design review keeps the process choice grounded in facts rather than habit.
Electrical requirements matter just as much. Signal speed, current density, and impedance control decide whether a simple two-layer board will work or a multilayer stackup is needed. Insulation distance and creepage rules also shape the layout. Engineers who settle these points early avoid late redesigns that inflate cost. The same discipline applies to PCB design and layout, where small decisions about pad size and spacing carry straight into fabrication price.
Production volume completes the picture. A design that is cheap at ten thousand units may be expensive at fifty. Tooling, stencil cost, and setup time spread differently across lot sizes. Buyers should share a realistic forecast, not just the first order quantity. Suppliers can then propose a process that fits the ramp rather than one that only suits the prototype stage.
Standard Boards and Material Choice
Consumer electronics, home appliances, and general control boards rarely need exotic materials. Standard FR-4 offers good insulation, mechanical strength, and thermal stability at a mature supply position. Its wide availability shortens procurement and keeps lead times predictable. For most of these products, FR-4 with a conventional finish covers the requirement comfortably.
Process complexity is the next lever. If the design does not call for fine-line traces, standard etching accuracy is enough. Choosing advanced imaging adds cost without adding function. Similarly, panel utilization affects material waste more than many buyers expect. Adjusting board dimensions or panel layout to fit the working area can cut scrap and improve throughput without touching the circuit itself.
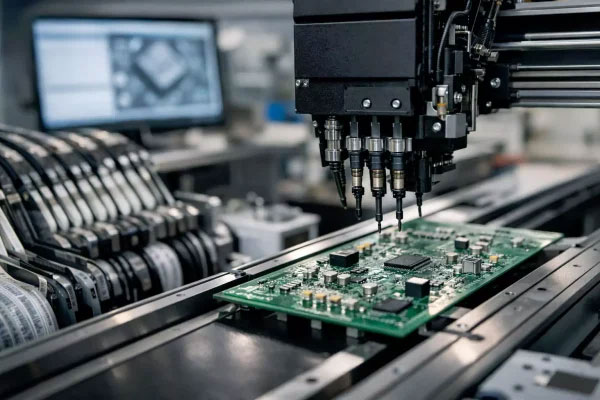
Assembly choices follow the same logic. A single-sided build with through-hole parts may suit a simple controller, while a mixed board needs reflow and selective soldering. Planning the PCB assembly route alongside fabrication prevents surprises at the line. When both steps are quoted together, the buyer sees the true cost of the finished board rather than a partial figure.
Surface Finish Tradeoffs
For industrial and automotive-style products, reliability and environmental resistance rise in importance. These boards still do not always need the most advanced technology. Surface finish is often the clearest cost decision. Hot air solder leveling costs less but can struggle with fine-pitch components because the pad surface is less flat. It remains a sound choice for coarser designs.
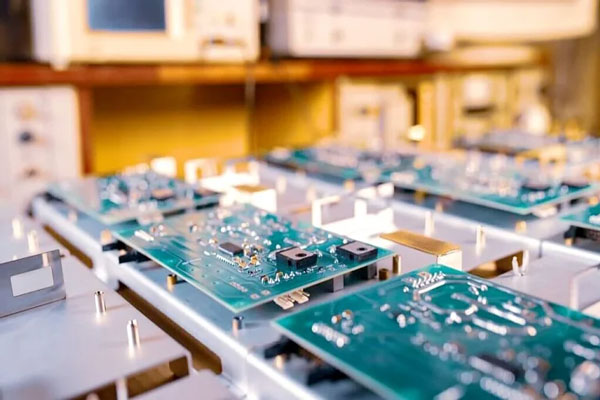
Electroless nickel immersion gold gives excellent flatness and oxidation resistance, which helps fine-pitch assembly and long storage. That performance carries a higher price. Immersion tin and immersion silver sit between the two, offering good solderability with moderate cost. The right pick depends on component pitch, storage time, and the number of reflow cycles the board will see.
Finishes also interact with test and handling. A flat finish supports reliable probe contact and consistent paste release. A rougher surface may need tighter process windows. Buyers should ask which finish the assembly house prefers for the given pitch, then confirm the fabrication quote matches that choice. Mismatches here are a quiet source of yield loss.
Storage conditions deserve a place in that decision. A finish chosen for long shelf life still fails if panels sit in humid air without protection. Ask how boards are packed, how long they may wait before assembly, and whether a bake is required. These details cost little to settle early and prevent solderability complaints that appear only after the first reflow pass.
Layer Count and Stackup Planning
More layers do not automatically mean better performance. Extra layers add material, drilling, and lamination steps, and each step carries a yield risk. Careful component placement and routing can often meet the electrical requirement with fewer layers. Engineers should challenge the stackup before release rather than after the first batch.
When a multilayer board is genuinely needed, the stackup should be planned as a system. Signal layers, ground planes, and power planes each have a role. Symmetry matters for warp control during lamination. Buyers reviewing a high-volume PCB assembly program should confirm the stackup is fixed early, because stackup changes late in the project reset tooling and qualification.
Impedance targets, if any, must be stated with tolerance. A vague requirement forces the fabricator to guess, and guessing usually means over-engineering. Clear numbers let the supplier choose a dielectric and trace width that meet the target without excess margin. That clarity lowers cost and reduces the chance of a redesign.
Drilling is where a tight stackup often shows its cost. Smaller holes and thicker boards raise the aspect ratio, which makes plating coverage harder to hold. A design that keeps holes within a comfortable ratio avoids extra process control and scrap. Buyers should ask the fabricator to confirm the aspect ratio and the minimum annular ring before tooling begins, not after panels are cut.
Small Batches and Process Reuse
Startups, research groups, and pilot lines often assume small orders must carry high unit prices. That is not always true. Combining requirements across projects, planning inventory sensibly, and scheduling production to fill capacity can improve utilization. The buyer gains a better unit cost without changing the design or the quality target.
Reusing proven designs is another strong lever. Standard board outlines, hole sizes, and material selections reduce engineering changes. Each change triggers new checks, new tooling, and new documentation. A validated design that moves from prototype to production with minimal edits avoids that overhead. It also shortens the development cycle, which matters when a launch date is fixed.
Prototype work should be treated as part of the plan, not an extra cost. Early samples reveal pad geometry issues, component tolerance problems, and process behavior before volume is committed. Teams that invest in this stage usually reach production faster. Linking prototype and volume under turnkey PCB assembly keeps the process settings consistent from the first panel to the full run.
Cost Drivers Buyers Should Verify
Price per board is only one number. Setup charges, stencil cost, test coverage, and component sourcing decide the real cost of ownership. A quote that omits test may look low until defects appear in the field. Buyers should ask what inspection and electrical test are included, and whether first-article approval is part of the scope.
Material sourcing deserves the same scrutiny. Component availability can shift a schedule more than any fabrication step. A supplier that checks alternates and lead times before release protects the build. The wider view of this work is set out under component procurement, where sourcing and fabrication are planned together rather than in sequence.
Documentation is the last check. The drawing, process sheet, and inspection plan should agree before release. Any deviation found during the run should be closed before the next build. Repeat orders then start from a known baseline. That habit keeps cost stable across batches and makes future quotes comparable.
Yield data is the other number worth requesting. A supplier that tracks scrap by process step can explain where cost sits and where it could fall. Without that record, a low quote simply hides the loss until a later lot. Ask for first-pass yield on similar boards and for the main defect categories. The answer shows whether the price reflects a stable process or an optimistic estimate.
Practical Takeaway
Cost-effective PCB work comes from matching process to purpose. Define the environment, the electrical need, and the volume first. Then choose material, finish, and layer count to meet those needs with sensible margin. Avoid complexity the product does not use, and plan assembly and sourcing alongside fabrication. Buyers who verify test coverage and documentation before release get predictable pricing and fewer surprises after the first lot.