PCB Demand Trends in Electronics Manufacturing
PCB buying has changed. Boards are no longer ordered as generic substrates with a standard layer count and a fixed tolerance. Automotive, medical, industrial, server and consumer programs now pull fabrication in different directions at the same time. Each segment asks for its own mix of reliability, density, signal quality and thermal control. This article explains what those demands do to the manufacturing process and what buyers should verify before releasing an order.
Demand shifts matter because they reach the factory floor. A tighter impedance window changes the stackup. A smaller package changes the stencil and the placement program. A higher current path changes copper weight and drilling. Engineers who understand the direction of demand can plan tooling, materials and inspection earlier. Buyers who understand it can ask better questions during supplier comparison. The result is fewer surprises between the prototype and the production lot.
Application Specific Boards
General-purpose boards still exist, but they cover a shrinking share of volume. Most new programs define electrical, thermal and mechanical limits before the layout starts. Those limits come from the enclosure, the power budget, the operating environment and the product lifetime. Two boards with the same dimensions can therefore need different materials and different process controls. Treating them as interchangeable is the fastest way to lose yield in production.
Application-specific demand also changes the quotation. A supplier must review the drawing, the stackup and the test plan before quoting a real number. A price built on a generic board tells the buyer nothing about the actual job. Buyers should send the full data package and ask which process steps the quote includes. That answer separates a serious fabrication partner from a broker who forwards files without reading them.
One failure mode appears when a program copies a stackup from an older product without rechecking the current load. The copper weight may be adequate for the previous current, but the new design adds a power stage or a denser connector. The board then runs warmer and the plated holes see more stress. Buyers should ask for the current and thermal assumptions behind the stackup, not just the layer count.
Automotive Reliability Demands
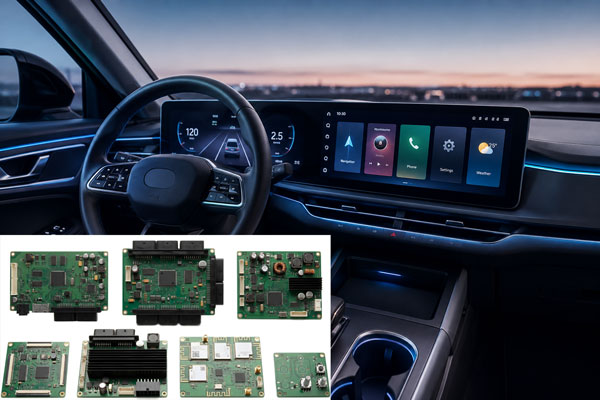
Automotive electronics sit in one of the toughest environments for any board. Battery management, control units, sensors and power stages see temperature cycling, vibration, humidity and long operating hours. Each of these stresses attacks a different part of the board. Thermal cycling works on plated holes and solder joints. Vibration works on connectors and heavy components. Humidity works on insulation and surface finish.
Suppliers respond with tighter process control rather than a single special material. Copper thickness, hole wall quality, surface finish and lamination all need to hold across the lot. Buyers should ask how the factory records these parameters and how it handles a deviation. A board that passes the first article but drifts in the fifth lot is a field failure waiting to happen. Consistency is the product automotive customers actually buy.
Hole wall quality is a common weak point. A thin plating in a high-aspect-ratio hole can crack after repeated thermal cycles, and the crack may not show until the board is in the field. Buyers should ask how the factory checks plating thickness and how it monitors the plating bath. A recorded trend line for each lot is more useful than a single pass certificate from one build.
Medical Miniaturization Pressure
Portable diagnostics, monitors and laboratory instruments keep shrinking while adding functions. That combination pushes component density up and board area down. Fine-pitch packages, smaller vias and tighter spacing become normal rather than special. The fabrication process must then hold registration and plating quality across features that leave little room for error. Solder mask dams and annular rings become thin enough to matter.
Medical demand also raises the bar on process cleanliness and documentation. Contamination control and traceability matter as much as electrical performance. Buyers should separate device regulation from board specification. Standards such as IEC 60601 apply to the equipment and its manufacturing system, not to every bare board as a universal certificate. The board spec should follow the finished device requirements and the applicable regulatory path, not a marketing claim on a website.
Registration error is the failure mode to watch. When layers shift, the annular ring on a small via narrows on one side and the connection becomes marginal. The defect may pass electrical test at the factory and open later under thermal stress. Buyers should ask how the supplier measures layer-to-layer registration and what limit it holds on the panel, not only on the sample.
Consumer Cost And Speed
Consumer products compete on price, differentiation and time to market. Buyers want customization in dimensions, layer count, finish and mechanical fit, but they cannot pay for technology the product does not use. Choosing an unnecessarily advanced board structure raises cost without improving the user experience. The better approach is to match the stackup and material to the real electrical and mechanical need.
Speed adds another constraint. Tooling, first article and assembly must fit a short development window. Suppliers who review files early and flag risks before tooling help here. A question raised at file review costs a message. A guess discovered at assembly costs a week. Buyers should confirm the review step exists and that engineering answers arrive before the production slot is booked.
High Speed And Thermal Loads
AI computing, data centers and networking equipment push data rates higher every cycle. At those rates, the board stops being a passive carrier. Dielectric properties, trace geometry, reference planes and via structures all shape the signal. Impedance control must hold across the panel, not just on the test coupon. Material choice is one input, and stackup design is another.
The same systems generate serious heat. High processor and power density demand copper areas, thermal vias and suitable materials to spread heat away from hot spots. Signal integrity and thermal design interact, so they should be solved together. A stackup tuned only for loss may leave the board too hot. A stackup tuned only for heat may spoil the impedance. Buyers should ask how the supplier balances both.
Impedance drift is a quiet failure. If the dielectric thickness varies across the panel, the trace impedance moves with it, and the link may work on the bench but fail at speed. Buyers should ask how the factory controls lamination thickness and how it measures impedance on production panels. A coupon result from one corner of the panel does not prove the whole panel.
Procurement And Assembly Scope
Procurement teams now compare more than unit price. They look at engineering support, material control, lead time and production flexibility. They also ask whether fabrication and PCB assembly can run under one roof. A coordinated flow reduces handoffs, shortens the feedback loop and keeps one team responsible for the finished board. That matters most when a design change lands between the bare board and the assembly stage.
Component supply adds risk of its own. A part that changes plating or a reel stored in humidity can shift the process without any machine alarm. Linking component procurement to the build plan keeps sourcing, inspection and assembly working from the same data. Buyers should ask who checks incoming parts and how alternates are approved. Those answers reveal whether the supply chain is managed or simply passed along.
Handoff errors are the failure mode here. When fabrication and assembly sit with separate vendors, a revised Gerber or a changed bill of materials can reach one side and not the other. The board is built to the old revision and the parts are kitted to the new one. Buyers should ask how revisions are controlled across both stages and who signs off before the lot is released.
What Buyers Should Verify
Start with the data package. A supplier should review the Gerber files, the stackup and the bill of materials before quoting. Ask which process steps the price covers and which tests are included. Confirm that PCB design and layout support is available when the file needs correction. A supplier who reads the files will raise questions, and those questions are a good sign rather than a delay.
Next, ask how the factory holds consistency across lots. Material control, calibrated equipment and recorded process parameters decide whether the fifth order matches the first. Request inspection data and test reports with the shipment. For programs that need both fabrication and assembly, compare a turnkey PCB assembly flow against separate vendors. When volumes grow, confirm the partner can scale into high-volume PCB assembly without changing the process that was qualified.
The practical takeaway is simple. Demand is moving toward specialized boards, so the supplier comparison should move with it. Match the stackup to the application, record the agreed limits, and verify them again in production. Ask for the documents that prove the process, not just the price that wins the order. A partner who reviews files early, reports risks honestly and keeps records will cost less over the product life than one who quotes low and surprises later.