Zhanjiang SMT Processing: Coastal Manufacturing
Zhanjiang sits on the western edge of Guangdong, close to the Leizhou Peninsula and the sea. Electronics buyers often ask what that geography means for a surface mount order. The answer is practical rather than romantic. Coastal air, humidity swings and a long supply chain into the Pearl River Delta all shape how a factory runs its line, and how it protects the boards it builds.
This guide looks at Zhanjiang SMT processing from the floor upward. It covers the process chain, the checks that catch defects, the environmental controls a coastal plant needs and the questions a buyer should ask before releasing a program. The goal is a repeatable result, not a slogan about location.
The Process Chain
What you get at the end comes from the entire chain, not from any one machine. The board design fixes pad sizes and spacing, the printer controls the solder volume, the placement machine positions every component and the reflow oven forms the joints. Each step feeds the next one, so the work should be reviewed as one complete process instead of a set of separate operations. A weak link anywhere shows up at final test.
Good PCB design and layout sets the starting conditions. Pads that are too small starve a joint, and pads that are too large let the part float during reflow. Spacing between pads decides whether the stencil can release paste cleanly. Engineers who review these details before tooling avoid most of the rework that appears later on the line.
Humidity on the Coast
Coastal air carries moisture, and moisture changes how solder paste behaves. A paste that sits in a humid room absorbs water, and the print becomes sticky and prone to slumping. Factories near the sea usually store paste in sealed jars, let it warm in a controlled way and track its working life. Simple discipline here prevents defects that no machine setting can fix.
Moisture sensitive devices need the same care. Components absorb water during storage, and that water turns to steam inside the package during reflow. The result can be a crack that passes inspection and fails in the field. Dry cabinets, humidity indicators and a written bake schedule keep this risk under control through the wet season.
Print and Placement Control
The stencil and the printer decide how much paste lands on each pad. Aperture size, stencil thickness and squeegee pressure all interact. A thicker stencil may fix an open joint and cause a bridge on a fine pitch part, so the choice must match the board. Solder paste inspection after printing catches volume errors before expensive components are placed.
Placement accuracy matters most on fine pitch and small chip parts. The machine must hold position across a full panel and across a long shift. Nozzle condition, feeder setup and vision alignment all affect the result. A factory that checks placement data daily spots drift early, while one that waits for a customer complaint learns about it too late.
Reflow and Profiling
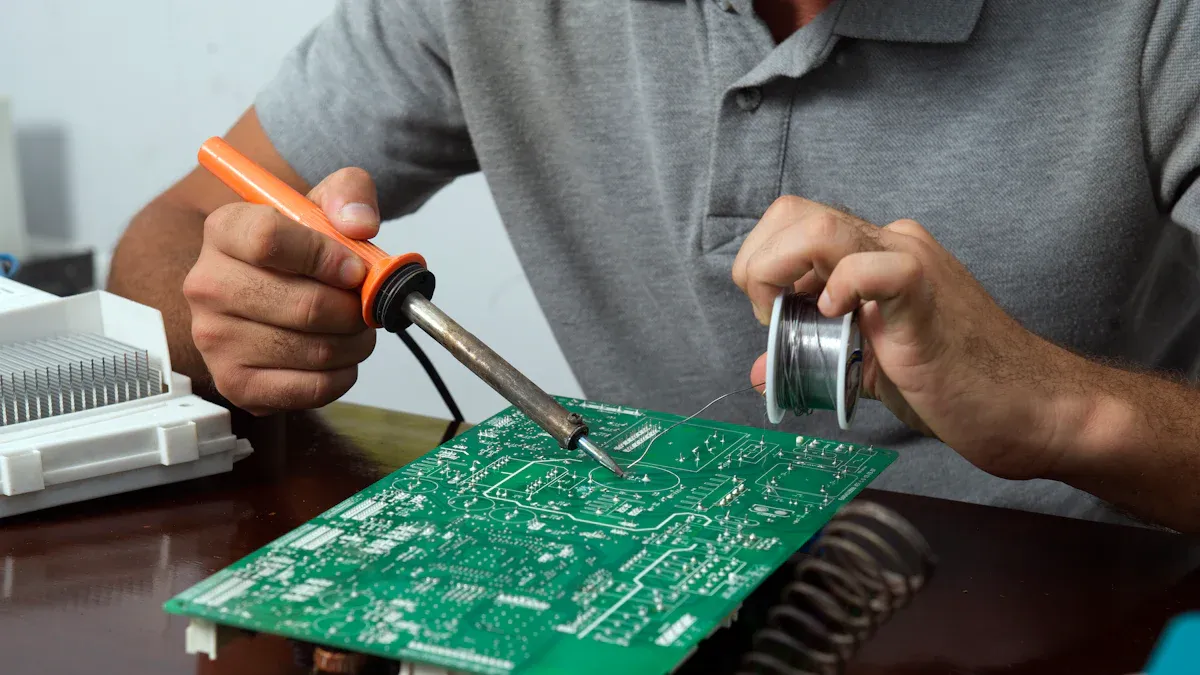
The reflow profile turns paste into a reliable joint. Ramp rate, soak time, peak temperature and cooling all influence grain structure and voiding. A profile built for one board rarely suits another, so each program needs its own thermal measurement. Thermocouples placed on real joints give better data than a profile copied from a similar product.
Coastal plants also watch ambient conditions during reflow. Room temperature and draughts near the oven can shift the profile slightly, and small shifts add up over a long run. Enclosed ovens and stable room conditions keep the profile repeatable from morning to night and from one season to the next.
Inspection and Test
At the beginning of each order, first article inspection has a role that is particularly important. A detailed check of the first board is made against the design. Component values, orientation, polarity and solder quality are verified before the line continues. This single step prevents a whole batch from inheriting a setup error, and it gives the customer a documented starting point.
Once the run is complete, automated optical inspection checks each board, and samples then proceed to electrical test. Optical inspection finds missing parts, shifts and bridges, while electrical test proves the circuit works under power. Together they cover the defects that visual checks miss, including cracked joints and wrong values that look correct.
Traceability turns good intentions into proof. The factory records which program ran, which reels of paste and components were used, which operator handled the job and what inspection found. When a field return appears months later, that record offers the fastest route to the root cause. Buyers should ask for these records as a routine part of every order, not as a special request.
Materials and Partners
Suppliers carry risks of their own. A component that quietly changes its plating, a paste batch with different viscosity or a reel stored in humidity can shift the process without any machine warning. Professional factories qualify materials, check certificates of analysis and approve alternates in advance. Solid component procurement keeps a supply change from becoming a quality incident.
Most boards are built by specialists rather than in house. The investment in printers, placement machines, reflow ovens and inspection equipment is large, and the engineering time to keep the process stable is easy to underestimate. A partner spreads that cost across many programs and brings the same discipline to each one. Services such as turnkey PCB assembly and high-volume PCB assembly can sit under one roof.
What really decides which supplier you pick is how they act when things get difficult. How a factory answers a design question, handles a shortage or responds to a defect tells more than a brochure. Ask for defect data, test coverage and references, and confirm the quality plan in writing before you commit a program. A partner that reviews files early and reports risks honestly is cheaper over a full project.
Training and Improvement
Every person touching the process needs training. Before making any adjustment, operators need to understand the reason a parameter window is in place. Inspectors must know what a real defect looks like. Engineers need to be capable of explaining why the data has changed. Factories that invest in training get faster answers to problems and fewer repeated mistakes, because knowledge on the floor turns written procedures into daily practice.
Nothing is decided once and forgotten. Parameters drift, materials change and operators rotate, so the factory reviews its data continuously. It identifies the most significant defects and then eliminates them individually, one after another. Factories that follow this discipline lower defect rates and shorten lead times, while factories without data repeat the same mistakes at the same cost. Keeping the same metrics under monthly review makes it possible to see whether progress is being maintained.
Prototypes are the cheapest place to make mistakes. Before thousands of boards are committed, the first small batch exposes pad geometry issues, component tolerances, and process behavior. The design review and the pilot run belong to the project, not to an extra budget line. Buyers who invest at this stage usually reach volume faster and with fewer surprises than those who rush to the big order.
Buyer Checklist
Before placing an order, confirm how the factory controls humidity and static. Ask where paste is stored and how working life is tracked. Check whether each program has its own measured reflow profile. Request the first article report and a sample of the traceability record. These questions cost nothing and reveal whether the process is documented or improvised.
Then confirm the commercial side. A clear quote should state what is included in PCB assembly, from tooling and stencils to test coverage and packing. Ask who owns the component risk when a part changes. Agree the inspection standard and the acceptance criteria in writing. A short written agreement at the start prevents most disputes later, when a batch is already built.
The takeaway is simple. Coastal conditions add real process variables, and a factory that manages them builds the same board in July as in January. Ask for the records, visit the line if you can, and judge the answers rather than the price alone. Preparation at the quotation stage is the cheapest quality tool a buyer has.