Automatic SMT Placement Line: Automation in Action
An automatic SMT placement line turns a stencil print and a reel of parts into a populated board with very little hand contact. The machine does the picking, the vision system does the aligning, and the conveyor does the moving. What stays human is the setup, the programming and the decision about whether the process is still in control. This review looks at where automation actually helps and where engineers must still watch closely.
The placement head is the visible part of the line, but it depends on everything around it. Paste height, fiducial quality, feeder condition and nozzle health all decide whether a fast machine produces good boards or scrap. Buyers who understand that chain ask better questions during a supplier audit. They stop comparing headline placement speeds and start comparing the controls that keep those speeds repeatable across a full shift.
What the Line Does
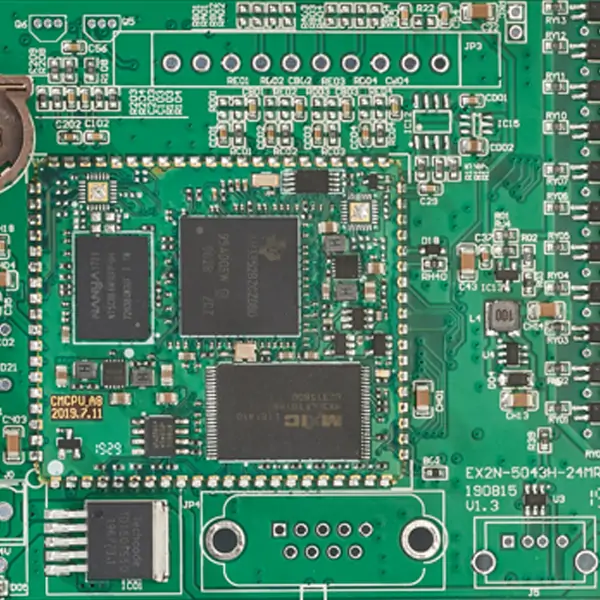
An automatic placement line loads panels, reads fiducials, picks components from feeders and places them on printed pads. Vision cameras check part orientation and lead position before the nozzle releases. The machine then moves to the next position at high speed and repeats the cycle. Modern heads place small chip parts and fine pitch devices on the same pass. The whole sequence runs from a program built from the CAD placement data.
Automation matters most when part counts rise. A manual bench cannot keep pace with thousands of placements per panel, and hand placement introduces variation that shows up later at inspection. The machine repeats the same motion with the same force and the same alignment tolerance every time. That repeatability is the real product of automation, not raw speed. It is also what makes a stable reflow profile possible downstream.
Programming and Setup Checks
The program starts with the centroid file, the bill of materials and the approved footprint library. An engineer maps each reference designator to a feeder position and a nozzle type. Rotation offsets and package variants cause most of the early errors, so they deserve a careful check before the first panel. A wrong rotation on a diode or an IC can survive printing and placement and only fail at test. Reviewing the program against the design data is cheaper than finding it later.
Fiducials deserve their own attention. Global fiducials align the panel, and local fiducials align fine pitch parts. If the fiducial is covered by solder mask, has poor contrast or sits too close to copper, the camera may fail to lock. The machine then places with an offset that grows across the panel. Good PCB design and layout practice keeps fiducials clear, unplated and consistent, which saves setup time on every run.
Feeder and Nozzle Control
Feeders are the quiet source of many placement defects. A worn feeder advances the tape by a fraction of a pitch, and the nozzle picks the part slightly off center. The vision system may correct it, or it may reject it and slow the line. Tape splices, empty pockets and misloaded reels create similar symptoms. Factories that track feeder performance by position find these faults quickly. They also keep spare feeders ready so a failure does not stop the shift.
Nozzles wear in a way that is easy to miss. A chipped tip or a clogged bore changes the vacuum, and small parts start to shift or drop. The machine may report a pickup error, or it may place the part with a small offset that passes visual inspection. A scheduled nozzle check and a clean routine protect the process. So does a vacuum level test at the start of each shift, which catches wear before it reaches the boards.
Placement Force and Accuracy
Placement force matters more as parts get thinner. Too much force can crack a ceramic capacitor or push paste out from under a pad. Too little force leaves the part sitting on top of the paste, where it can tombstone during reflow. The machine lets engineers set force per package type, and that setting should match the part and the paste. A single global force setting is a shortcut that usually costs yield on mixed boards.
Accuracy claims need context. A machine rated for a fine tolerance may only reach it under specific conditions, with slow speed, good fiducials and a stable environment. At full speed the same head may place within a wider window. Engineers should check the actual process capability for the smallest part on the board, not the brochure figure. That number decides whether the design fits the line or needs a different approach.
Paste Printing Comes First
Placement quality cannot rescue a bad print. The stencil aperture, the squeegee pressure and the separation speed set the paste volume that the part will sit on. A print that is slightly heavy causes bridging on fine pitch parts, while a light print causes opens after reflow. The placement machine places parts into whatever paste it receives, so print control is the first lever on the line. Solder paste inspection gives the data to adjust it.
Stencil cleaning frequency belongs in the process plan. Paste dries in apertures and reduces transfer over time, so the line needs a defined cleaning interval. Under-wiping slows the line, while skipping wipes lets defects build. The right interval depends on the paste, the aperture size and the board volume. Factories that log print results and cleaning events can tune the interval with evidence. That is a practical example of automation supported by process discipline.
Inspection and Test Coverage
Automated optical inspection follows placement and reflow, checking presence, position, polarity and solder shape. It catches the errors that the machine cannot see, such as a part placed correctly but soldered poorly. The data from inspection feeds back to the placement and print steps. When the same defect appears at the same position, the engineer knows where to look. That closed loop is what keeps a fast line from producing fast scrap.
Electrical test adds the check that vision cannot make. A cracked joint or a wrong value may look fine under a camera and fail under power. In-circuit test, functional test and boundary scan each cover different risks, and the mix should match the product. A structured PCBA testing plan states which tests run, on which boards and at what stage. Buyers should ask for that plan before the order, not after the first failure.
Materials and Environment
Components and paste carry risks that no machine setting can remove. A part with a different plating finish, a paste batch with changed viscosity or a reel stored in humidity can shift the process without warning. Qualified suppliers, incoming checks and approved alternates keep that risk contained. Moisture sensitive devices need dry storage and a controlled floor life before reflow. These steps are simple, but they fail quietly when nobody owns them.
The assembly area itself affects the result. Temperature and humidity change how paste behaves on the stencil and how it flows in reflow. Static discharge can damage sensitive parts without a visible mark, so grounding and ionized air belong in the plan. A line that runs well in winter may drift in a humid summer if the environment is not controlled. Buyers rarely see these details in a quote, yet they decide whether yield holds all year.
Buying the Right Partner
A dedicated line only pays for itself when it runs constantly. Keeping programs current, calibrating machines and maintaining quality records takes engineering time that is easy to underestimate. Most product companies therefore work with a partner that spreads that investment across many customers. Services such as turnkey PCB assembly and component sourcing under one roof reduce the number of handoffs. Fewer handoffs mean fewer places for a setup error to hide.
When suppliers are compared, price per board should never be the only number. Process controls, inspection equipment, component sourcing, and communication are what actually determine the real cost. A partner that reviews files before production, reports risks honestly and keeps delivery promises will cost less over a project than one that quotes low and surprises later. Ask how the supplier measures placement yield and what happens when a feeder or nozzle fails mid-run. The answers show whether automation is truly in action.
gopcb runs SMT PCB assembly lines supported by paste inspection, optical inspection and functional test in one facility. Engineers review Gerber files and the BOM before production and discuss the process options that fit the design. Boards ship with test records that support field confidence. For teams planning a new product or moving a design to volume, the useful step is to send the files and requirements for a manufacturability review.
A clear quote and a planned schedule follow, with PCB assembly steps stated in the breakdown so the buyer knows what is included.