Line Changeover and Setup Verification
Most assembly defects are introduced during changeover, when the line is reconfigured for a different product and the checks that ran during production are paused. The changeover is therefore the moment that deserves the most discipline and usually receives the least.
What a Changeover Involves
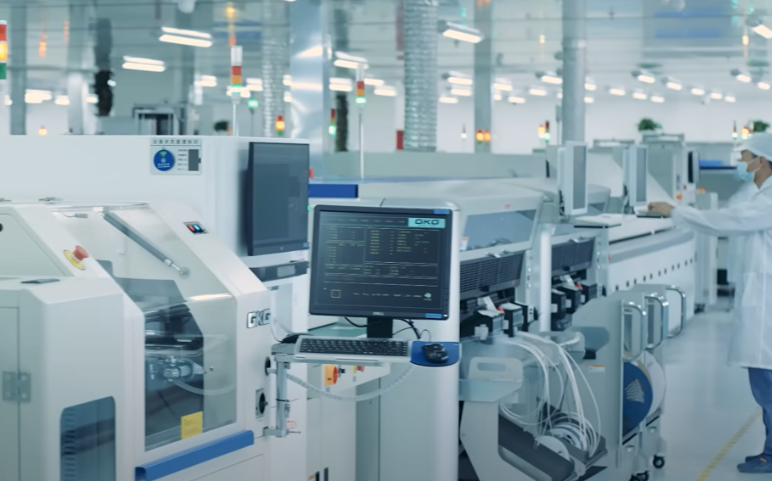
The feeders are removed and the new ones loaded, the stencil is changed, the printer parameters are recalled, the placement program is loaded, the oven program is selected and the inspection programs are changed.
Each of those steps is a place where a mistake can be made, and each has a verification that takes seconds. The purpose of a changeover procedure is to make those verifications automatic rather than dependent on memory.
The procedure should list the steps in order and name the checks that must be signed off, and it should be the same document every time rather than a verbal instruction.
Feeder and Material Verification
Each feeder must be loaded with the correct part, and the part must be verified rather than assumed from the label. A reel that is placed in the wrong slot produces a board full of the wrong component, which is expensive.
The feeder setup sheet should list the slot, the part number and the reel quantity, and the check compares the sheet against the physical line. The check is fast and it catches the error that would otherwise be found at test.
Where two parts have similar part numbers, the check should include the physical marking on the reel and not only the number. Our component selection notes describe how parts with similar designations are distinguished.
Stencil and Printer Setup
The stencil must be the correct revision for the product, and it should be verified against the documentation rather than by matching a name. Two revisions of a stencil can differ by a single aperture.
The printer parameters are recalled from the program, and the paste is checked for its lot, its age and its condition. A paste that has been open too long behaves differently from fresh material.
The first print after the changeover should be measured rather than only inspected. Our paste inspection notes describe the measurement and the reference it is compared against.
<img src="https://www.gopcba.com/wp-content/uploads/2026/08/RoHS-Circuit-Boards-1536×640.jpg.webp" alt="First article board after a line changeover” />
Program and Profile Selection
The placement program, the conveyor width, the support pins or pallet, and the oven profile must all correspond to the product being built. A program that is one revision old places parts correctly for the previous design.
Where the board has been redesigned, the support pins must be repositioned, because a pin under a component is worse than no pin at all. The support plan should be part of the program rather than improvised.
The oven program selection is a common error, because two profiles for similar products look alike. The profile should be identified by the product and the revision in its name. Our design release checklist notes where the profile is recorded.
The First Article
The first article inspection is the verification that the changeover succeeded, and it should cover the items most likely to be wrong: the paste deposits, the placement positions, the orientation of polarised parts and the joint formation.
The inspection should be performed against the assembly drawing and not against the previous build, because the drawing is the current requirement and the previous build may carry an error forward.
Production should not resume until the first article has been accepted and the result recorded. The temptation to run boards while the inspection is completed is the reason a changeover error reaches the customer. Our inspection notes describe how the automated checks complement the manual one.
Reducing the Changeover Time
The time can be reduced by preparing the next product’s feeders and stencil while the current product runs. The preparation is offline and it removes the largest part of the downtime.
Standardising the feeder types, the support systems and the pallets across products reduces the number of setup steps and the number of opportunities for error.
Where the changeover is frequent, the investment in offline preparation is recovered quickly, and the error rate falls because fewer steps are performed under time pressure.
Records and Learning
The changeover record should note the product, the time, the operator, the checks completed and the first article result. Over time the record shows which products take longest and which checks are consistently skipped.
A changeover that produced a defect should be reviewed and the procedure updated, so that the same mistake does not recur. The review is short and it is the mechanism by which the process improves.
The records also support the traceability requirement, since they tie a unit to the configuration under which it was built. Our quality notes describe how the records are filed with the lot.
Process Control and Verification
Running a first article through the same checks as the production panel confirms that the two agree, and that comparison is the cheapest form of process control available at prototype stage. Keeping a sample from the panel turns a dispute into a measurement, because the same coupon can be re-examined by both parties without rebuilding the batch.
Reviewing the design before the data is released is cheaper than correcting it after the panel is in the tank, because every step downstream inherits the decision made at the front end.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
Verification and Records
A parameter that is set once and never re verified drifts, and the drift is usually discovered by a defect rather than by the record.
FAQ
Is a first article necessary after every changeover? Yes, and it can be brief where the changeover is simple. The alternative is to find the error at test, which costs more.
Who should perform the verification? Someone other than the person who made the change where the volume allows, since an independent check catches errors that the person who made them cannot see.
What does gopcb provide for changeover control? We provide documented changeover procedures with sign off, offline feeder and stencil preparation, first article inspection against the current drawing, automated inspection programs matched to the product, and records that tie each unit to its build configuration.