PCB OSP Finish Defects: What Goes Wrong on the Line
OSP is a thin organic layer that protects bare copper before soldering. It has no metal to hide behind, so any process slip shows up fast. A board that looks fine after finishing can still fail at assembly or in the field. This article explains where OSP defects start, how they are detected and what a buyer should verify before releasing a lot.
The finish itself is simple in principle. A clean copper surface is treated so it stays solderable for a defined storage period. The difficulty sits in the cleaning that comes before and the handling that follows. Both steps are invisible in a quotation, yet they decide whether the finish survives the trip to the assembly line. Engineers who understand this chain ask better questions during supplier selection.
What OSP Actually Protects
OSP means organic solderability preservative. It forms a very thin film over exposed copper and keeps oxides from growing. Unlike gold or tin finishes, it adds almost no thickness and no metal. That is good for fine pitch and for flat pads. It also means the copper underneath must be clean and uniform before the film is applied, because the film only follows what it finds.
The film is not a permanent coating. It protects the copper during storage and through the first soldering cycle. Once flux and heat remove it, the copper must solder cleanly. If the film was applied over contamination, the flux cannot reach the metal properly. The result is a joint that looks acceptable but carries poor wetting and weak strength.
Cleaning Sets the Base
Most OSP defects trace back to surface preparation. Copper that carries oxide, oil or residue will not accept an even film. The cleaner must remove both organic soil and oxide without attacking the copper itself. Micro-etch depth matters here, because too little leaves oxide and too much roughens the surface unevenly. Both conditions produce patchy coverage that inspection may not catch.
Rinse quality is equally important. Water carried from one tank to the next can leave salts that interfere with the film. Conductivity and flow need checking on a routine schedule, not only when a defect appears. Drying is the last chance to avoid stains, because trapped water under the film leaves marks that later block wetting. A buyer should ask how these three steps are monitored.
Etch bath life is a common blind spot. Copper builds up in the solution as panels pass through, and the etch rate falls quietly over time. Operators who top up chemistry without checking dissolved copper can run a bath that still looks correct but no longer cleans evenly. Logging bath age, copper load and etch rate together gives a far clearer picture than any single reading taken on its own.
Application and Coverage
The OSP chemistry must wet every copper surface, including hole walls and tight pad gaps. Concentration, temperature and dwell time each shift the film thickness. A film that is too thin offers weak oxidation protection. A film that is too thick can fail to clear during soldering, which leaves residues that disturb wetting. The supplier should hold all three parameters inside a written window and log them per batch.
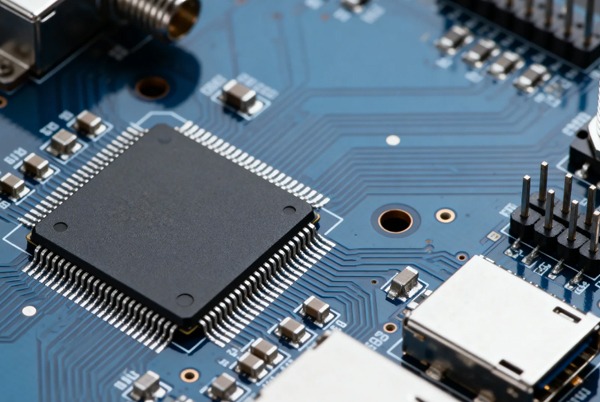
Coverage problems often appear on large copper areas and on isolated pads at the same time. That pattern points to flow or wetting rather than to chemistry. Board orientation in the tank and the spacing between panels change how fresh solution reaches the surface. Engineers reviewing a defect should look at the pattern across the panel, because a local cluster and a random scatter have different causes.
Solution drag-out and replenishment deserve the same attention. Chemistry carried out on the panels must be replaced at a rate the bath can tolerate, or concentration drifts downward through the shift. Automatic dosing helps, but only when the controller is calibrated and the pump delivers what it reports. A manual check of concentration against a titration result at shift start and end catches most of these slow drifts before they reach a customer lot.
Storage and Handling Risk
OSP protects copper for a limited period, and that period depends on how the boards are stored. Heat and humidity speed oxidation under the film. Stacking boards without interleaving can scratch the surface. Handling with bare fingers leaves oils that resist the film and later disturb solder. These are simple points, but they account for a large share of complaints that arrive weeks after delivery.
Packaging should suit the finish. Moisture barrier bags with desiccant and a humidity indicator give the buyer a way to check storage conditions on arrival. The shelf life clock should start from the finishing date, not from the order date. Buyers planning a slow build should confirm the remaining life before the panels reach the SMT PCB assembly line, because an expired surface cannot be recovered by a stronger flux.
Solderability and Assembly Effects
OSP interacts directly with paste and flux. A finish that has oxidized will not wet in the reflow window, and the joint may show as a non-wet open or a weak fillet. Paste chemistry matters too, because some fluxes clear OSP films more effectively than others. When a defect appears, the first question should be whether the finish changed or the assembly materials changed.
Multiple reflow cycles put extra stress on the surface. The first pass removes the film on exposed pads, and the copper begins to oxidize before the second pass. Boards that need two or three passes deserve a tighter storage and handling plan between runs. Nitrogen in the oven can help margin, but it does not fix a contaminated surface. Process order and time between passes are the real controls.
Selective solder and rework add another exposure. A pad that has already been heated once carries no fresh film, so a second operation depends on flux activity and on how quickly the board moves through the line. Hand soldering at a bench is the usual place where this gap appears, because the interval between reflow and touch-up is rarely measured. Buyers with mixed technology boards should ask how that interval is limited and recorded.
Detection and Test Coverage
OSP defects are hard to see. A discolored pad may be harmless and a clean pad may be contaminated, so visual inspection alone is weak. Solderability testing on coupons gives a direct answer about wetting. Ionic contamination testing shows whether cleaning left residues behind. Both tests cost little compared with a field return, and both should appear in the quality plan.
Inspection data becomes useful only when it feeds back into the process. When a wetting failure appears, the engineer should trace it to cleaning, film application or storage, then correct that step. That closed loop is what a real quality management system supports. Buyers should ask for the test method, the sampling plan and the reaction plan, not just a pass certificate.
Coupon placement matters as much as the test itself. A coupon cut from a panel edge may see different flow than a coupon from the center, so the sample location should be stated and kept consistent between lots. When results are compared over months, a change in sampling position can look like a process shift. Recording where each coupon came from keeps the trend honest and makes a real drift easier to spot.
Supplier Checks That Matter
Questions asked before the order prevent most trouble. Ask how copper cleaning is controlled, how the film parameters are logged and how shelf life is marked. Ask what happens when a batch fails solderability testing. A supplier with clear answers usually has a stable line. A supplier that answers in general terms may be relying on luck rather than on control.
For new designs, a small pilot lot is the cheapest way to learn. The first panels reveal how the finish behaves with your paste, your stencil and your oven profile. That early evidence supports rapid PCBA prototyping without committing a full order. Buyers who test the surface early reach high-volume PCB assembly with fewer surprises and a settled process window.
Material sourcing belongs in the same conversation. A paste or flux change can alter how the film clears, even when the finish itself is unchanged. Suppliers who qualify materials and keep approved alternates reduce that risk. A component procurement process that tracks certificates and storage conditions closes the last gap. Finish quality is a chain, and every link deserves a check before the lot is released.