PCB Conformal Coating Limits: Where the Edges Are
Conformal coating looks simple on a drawing: cover the board, cure it, ship it. On the line, the real question is where the coating must stop. Connectors, test points, relays, and press-fit pins all need clear space. So do keep-out zones around screw holes and board edges. Those boundaries are the limits, and they decide whether the coating protects a product or quietly blocks service access later.
A coating that creeps into a connector body can cause intermittent contact. A coating that stops too far from a component leaves a gap where moisture collects. Both failures pass visual inspection and appear months later in the field. This review sets out where the edges are, how process choices move them, and what a buyer should confirm before approving a coated build.
What the Limits Cover
The limits of a coating process cover more than a single keep-out line. They include the surfaces that must stay bare, the areas that must be fully covered, and the tolerance on both. They also include the coating thickness window, the cure window, and the handling time between steps. Each limit has a reason, and each reason connects to how the product is used and serviced.
Masking defines most of these edges in practice. Tape, plugs, and boots protect connectors and test pads during spray or dip. The mask must seal cleanly, survive the coating and cure, and peel without residue. A mask that lifts at one corner lets coating wick under the tape. That leak is hard to see and easy to miss at final inspection.
Coating type sets the rest. Acrylic, silicone, polyurethane, and parylene behave differently at edges. Some flow and thin out near a mask line, while others build a thicker ridge. The material choice should follow the environment, the rework plan, and the temperature range the board will see. It should not follow habit alone.
Masking and Keep-Out Zones
Every keep-out zone costs time on the line. Each one needs a mask, a check, and a removal step. Engineers should therefore place keep-outs only where function or service demands them. A test pad that is never probed after coating may not need protection. A connector that is mated in the field almost always does, because coating on the pins changes contact resistance.
The board outline matters too. Coating that reaches the edge can interfere with card guides, chassis slots, and mounting hardware. A defined edge clearance keeps the cured film away from surfaces that must slide or seat. It also reduces the chance of coating flaking during insertion, which leaves loose fragments inside an enclosure.
Good PCB design and layout makes these zones visible early. When keep-outs sit on the fabrication drawing and the assembly drawing, the coating house can plan masks before tooling. When they appear only as a note in an email, the line improvises, and improvisation is where edge defects start.
Thickness and Cure Windows
Coating thickness is a range, not a single number. Too thin a film leaves pinholes and poor coverage over sharp features. Too thick a film can crack during thermal cycling, trap solvent, or stress delicate parts. The window should come from the material datasheet and the product requirement, then be proven on real boards.
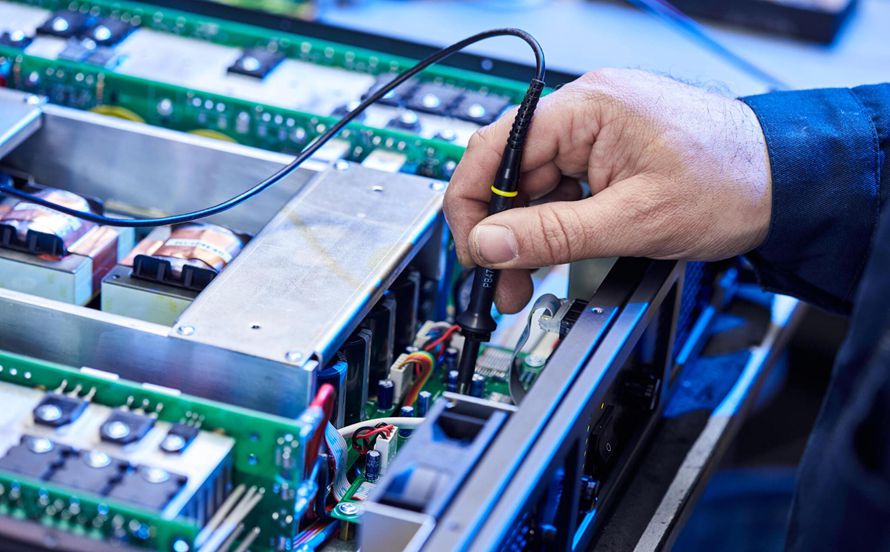
Cure conditions decide how that film behaves at the edges. An under-cured coating stays tacky, attracts dust, and may not reach full adhesion near a mask line. An over-cured coating can become brittle and chip when a connector is inserted. The oven profile should be recorded, and the cure should be verified rather than assumed from a timer.
Thickness measurement deserves a defined method. Measuring on a flat coupon is not the same as measuring over a component lead or beside a mask edge. Buyers should ask where the measurement is taken, how many points are checked, and what happens when a reading falls outside the window. A clear answer here separates a controlled process from a hopeful one.
Spray, Dip, and Selective Coating
Spray coating suits many boards because it is fast and flexible. It also creates overspray that can reach areas the mask does not cover. Operators must control angle, distance, and pass count, or the film will vary across the panel. Edges near tall components are the first place this variation shows up.
Dip coating gives good coverage over complex shapes, but it wets everything it touches. Masking must be complete before the board enters the bath, and drainage must be controlled so coating does not pool. Pools near a connector or a screw hole become thick ridges that crack or block assembly later.
Selective coating uses programmed paths to apply material only where it is wanted. It reduces masking and improves repeatability, but the program must be correct. A path that misses a component leaves a bare area, and a path that drifts coats a keep-out. The machine follows the program exactly, so the program carries the responsibility.
Inspection and Test Coverage
Coated boards are harder to inspect than bare ones. The film hides solder joints, obscures markings, and softens the contrast that optical systems rely on. Inspection must therefore happen before coating as well as after. Any defect that would be hidden by the film should be found and fixed while the board is still accessible.
Ultraviolet light helps confirm coverage, because many coatings fluoresce. A dark patch under UV suggests a thin spot or a missed area, especially near mask edges and component shadows. The check is quick, but it only works when the inspection area is dark and the operator knows what full coverage looks like.
Electrical test still has to run after cure. A coating that bridges two test points or insulates a contact will only show under power. A structured quality management approach ties the coverage check, the thickness data, and the electrical results into one record, so a drift in any of them is caught before the lot ships.
Rework at the Edges
Rework is where coating limits cause the most friction. Removing cured material from a small area without damaging the board takes skill and the right tools. Acrylic coatings soften with suitable solvents, while silicone and polyurethane resist them. Parylene is harder still, because it must usually be abraded or cut away.
The rework plan should be agreed before production, not after a failure. It should name the areas that may be repaired, the method for each coating type, and the inspection that follows. A repaired area needs new coating, and that patch must bond to the old film. A poor bond creates a seam where moisture can enter.
Component replacement near a keep-out is a separate risk. Heat from a soldering iron can lift coating and damage nearby parts. The technician must know which areas are sensitive and which are expendable. Training and clear work instructions matter more here than any machine on the line.
Buyer Checks Before Release
A buyer reviewing a coated build should ask for the coating specification in writing. It should state the material, the target thickness range, the cure conditions, and the list of keep-out areas. A specification that says only that the board is coated gives the line nothing to measure against and the buyer nothing to verify.
Ask how masking is verified before coating and how it is removed afterward. Ask for coverage records, thickness readings, and cure data. Ask what happens when a reading falls outside the window, and who decides whether the lot is released. These questions cost little and reveal whether the process is documented or improvised.
For projects moving toward volume, high-volume PCB assembly adds pressure on every edge decision. Masking time scales with quantity, so a design with many keep-outs becomes expensive to run. Early samples through rapid PCBA prototyping show which edges cause trouble before tooling is committed. Component procurement also matters, because a substitute part with a different height or body shape can change how coating flows at a boundary.
The practical takeaway is simple. Define every coating edge on the drawing, prove the mask and the cure on a small batch, and record the measurements for each lot. Coating protects a board only when its boundaries are as carefully controlled as its coverage. Treat the keep-outs as engineering features, not as line notes, and the coated product will hold up in service and remain serviceable when it returns.