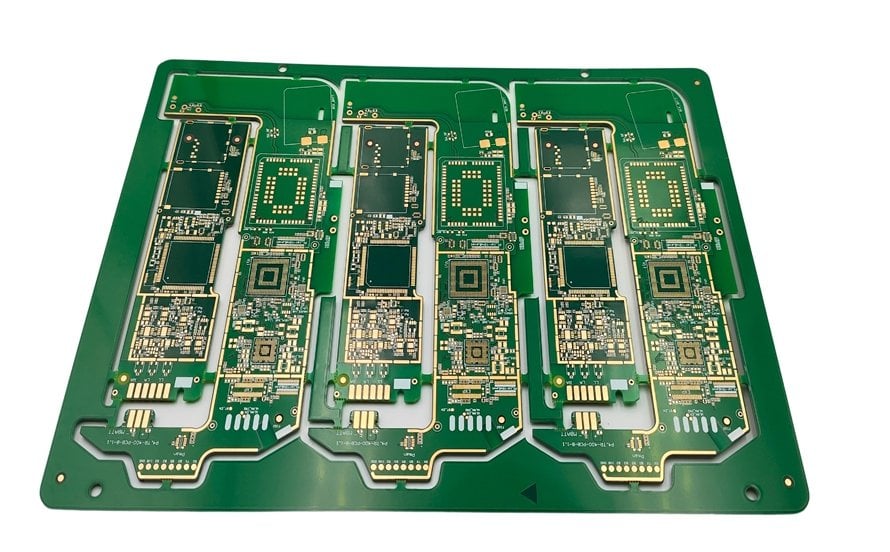
PCB Incoming Inspection Sample: Checking a Small Piece
A small incoming inspection sample can tell you more about a supplier than a full page of certificates. The sample is a physical board pulled from a delivered lot and checked against the drawing, the stackup and the finish. It shows whether the factory built what the file asked for, and whether the process holds from panel to panel. This article explains what to check on that piece, why the checks matter, and how to read the results before you release the rest of the lot.
What the Sample Represents
An incoming sample is not a random courtesy board. It is a controlled piece taken from a defined lot, with the lot number, date code and panel position recorded. That record lets you trace any finding back to the build conditions. When a defect appears, the trace tells you whether it is isolated or spread across the panel. A sample without that trace is just a loose board, and it proves very little about the lot behind it.
The sample size should match the risk of the order. A first article from a new supplier deserves more pieces than a repeat lot from a proven line. Critical products may need samples from several panel positions, because plating and etching vary across a panel. The goal is coverage, not volume. A few well-chosen pieces from different positions usually reveal more than many pieces from the same corner.
Visual Checks That Matter
Start with the features that are easy to see and hard to fix later. Check the board outline, the hole pattern and the registration of the solder mask against the copper. Look for mask slivers, exposed copper near pads and residue on the surface finish. These findings are cheap to catch at incoming and expensive to discover after assembly. A small piece under good light and low magnification shows most of them.
Marking deserves its own pass. Check the date code, the lot code, the UL marking and any customer-specific label against the purchase order. A missing or wrong marking can stop a line just as surely as a bad pad. Ask the supplier to state which marking method it uses, because ink and laser marks age differently. The sample should show the marking you will see on every board in the lot.
Stackup and Material Evidence
The sample is also your only physical evidence of the stackup. Measure the finished thickness at several points and compare it with the drawing. Check the copper weight on outer layers where the design exposes it, and confirm the surface finish by appearance and, where needed, by a simple test. If the order specifies impedance control, ask for the coupon data that belongs to the same lot. The piece in your hand should match the paperwork that came with it.
Material claims are harder to verify from one board. Ask for the laminate certificate and the prepreg lot used for the build. Check that the Tg and the dielectric values on the certificate match the design intent. If the supplier cannot link the certificate to the lot, treat the material claim as unproven. A sample plus a linked certificate is a much stronger position than a sample alone.
Dimensional and Hole Checks
Measure the critical dimensions on the sample, not every dimension on the drawing. Focus on connector spacing, mounting holes, board thickness and the distance from the edge to the first pad. These features drive assembly fit and tooling. A small error in a mounting hole can stop a whole build. Record the measured values against the drawing so the next lot can be compared with the same numbers.
Hole quality matters as much as hole position. Look at the wall condition, the annular ring and the breakout on the sample. A thin ring or a rough wall will cause problems at assembly and in the field. If the design uses small vias, check that the sample shows full plating and no voids at the surface. These are visual signs of a drilling and plating process that is under control.
Solderability and Finish Condition
Surface finish condition decides how the board behaves in the assembly line. Check for oxidation, contamination, scratches and handling marks on the pads. Ask how the supplier packs and stores finished boards, because a good finish can degrade in poor packaging. Where the product is sensitive, a solderability test on the sample gives direct evidence. The result should be recorded and kept with the lot file for later reference.
Finish thickness is worth confirming on critical boards. Ask for the measurement method and the values from the same lot. Thin finish can cause soldering problems, and thick finish can affect fine-pitch printing. The sample should carry the same finish as the production boards, applied by the same line. If the supplier changes its finish source, ask for a new sample before the next order runs.
Linking the Sample to Records
A sample is only useful when it connects to records. Ask for the lot traveler, the inspection report and the test coupon results for the same build. Check that the lot number on the board matches the number on the documents. When a finding appears, the record shows whether the cause is a one-off or a process trend. Buyers who ask for this link early usually avoid arguments later, because the evidence is already in hand.
Keep the sample and its records together in your own files. A dated piece with its report becomes a reference for future lots and for supplier reviews. When a new lot arrives, compare it with the retained sample under the same light. Differences in color, marking or finish show up quickly this way. This simple habit supports a working quality management routine without adding much time to receiving.
Working With Your Supplier
Share the checklist with the supplier before the first order. A factory that knows which features you will measure tends to control those features more carefully. Ask for the sample to be pulled after final inspection, not before, so it represents what will actually ship. Agree on how findings are reported and how quickly corrective action is expected. Clear expectations at the start reduce disputes when a lot arrives with a problem.
Use the sample review to test communication as well as hardware. A supplier that answers technical questions with data is easier to work with than one that answers with reassurance. Ask how the factory handles a change in material or process, and whether you will be told before the next lot ships. These answers predict how the relationship will run over many orders. The sample is the first test of that relationship, so treat the review as a two-way conversation.
Where the Sample Fits
The incoming sample sits between fabrication and assembly, and it protects both. It catches fabrication problems before they reach the SMT PCB assembly line, where rework costs more. It also gives the assembly team a known-good reference for setup and first article checks. When the sample passes, the line starts with confidence. When it fails, the problem is fixed before paste is printed, which saves time, material and schedule pressure for everyone involved.
For new designs, the sample review pairs well with rapid PCBA prototyping. A prototype lot lets you check the sample against real assembly behavior while changes are still cheap. Findings from the prototype sample can feed back into the fabrication file before volume begins. That loop shortens the path to a stable build and reduces the chance of a costly surprise at the volume order. Treat the sample as part of the development process, not as a separate purchasing step.
At volume, the sample review becomes a routine gate. Each lot gets a quick check against the retained reference, and any difference is raised before release. This keeps drift visible without slowing the line. A short, consistent check is more useful than a long, occasional audit. The discipline of checking a small piece every time is what keeps a long production program predictable, and it gives the buyer a simple way to hold the supplier to the agreed standard.
When you plan the next order, decide the sample size, the checks and the records before the purchase order goes out. State the drawing revision, the finish and the marking you expect. Ask for the lot link and the coupon data with the shipment. Then check the piece when it arrives, record the result and keep it. That routine turns a small board into a reliable gate for the whole lot, and it supports a stronger PCB assembly flow from the first delivery onward.
Suppliers who expect this review often build better records, because they know the sample will be checked against them. That pressure improves the whole chain, from lamination to final packing. Buyers who skip the check rely on luck and on the supplier’s own word. The difference shows up in yield, in schedule and in the cost of rework. A small piece, checked well and linked to its records, is one of the cheapest controls available to any electronics program.
For teams that need test evidence as well, pair the sample review with a defined PCBA testing plan. The plan should state what is tested, at which stage and what record is kept. The sample then becomes the physical anchor for that plan, because it shows the board the tests will run on. When the sample, the records and the test plan agree, the buyer has a clear basis for release and a fast way to trace any later field issue back to a specific lot.
The takeaway is simple. Pull a defined piece, check the features that drive fit and assembly, and tie the result to the lot records. Do this before every release, not only at the start of a program. The cost is small and the information is direct. A buyer who can show a dated sample and its report holds a stronger position than one who holds only a promise, and the supplier knows it.