PCB Sampling Plan Review: A Second Look at the Line
A sampling plan decides how many boards leave a line unchecked. That single number shapes the defect risk a buyer carries and the cost the factory absorbs. A second look at the plan asks whether the sample size still matches the process, the product and the customer’s tolerance for escapes. This review treats the plan as a living document rather than a fixed clause in a quotation.
Most plans are written once, during the first order, and then never reopened. The line changes, the component mix shifts and the defect profile moves, yet the sample size stays frozen. A structured second look corrects that drift before it reaches the field. It also gives the buyer a concrete basis for comparing two factories that quote the same board.
What the Plan Actually Covers
A sampling plan sets three things: the lot size, the sample size and the acceptance rule. Together they define how much evidence the factory collects before it releases a batch. The plan also names the inspection stages where that evidence is gathered. Without a written plan, each shift makes its own judgement, and the release decision becomes a matter of habit rather than data.
The plan should state which characteristics are sampled and which are checked on every board. Solder joint quality, placement accuracy and polarity are common sample items. Electrical function often runs at full coverage because the test is fast and automated. Mixing sample checks with full checks is normal, but the boundary must be written down so nobody assumes coverage that does not exist.
Reading the Plan Against the Process
A sample size only means something when the process is stable. If the printer drifts through a shift, a sample drawn at the start proves little about boards built at the end. The second look therefore pairs the plan with process data. Print reports, placement statistics and oven profiles show whether the line held its window while the sample was taken.
This is where many audits find the real gap. The plan looks reasonable on paper, but the records cannot show that the sampled boards represent the lot. A buyer should ask for the trend data, not just the pass count. When the trend is flat, a modest sample carries real weight. When the trend wanders, a larger sample only hides the problem.
Where Sampling Limits Appear
Sampling cannot prove a lot is free of defects. It estimates risk, and the estimate has a floor set by the sample size. A small sample will miss a low defect rate, and no acceptance rule can change that arithmetic. Engineers should know the escape rate the plan implies before they sign it, because the customer carries that risk in the field.
The tradeoff is straightforward. Larger samples cost inspection time and slow the release. Smaller samples save hours but raise the chance that a bad board ships. The right balance depends on the product. A consumer accessory and a control board for industrial equipment do not deserve the same plan, and treating them alike wastes money on one side and invites risk on the other.
Checks That Keep the Plan Honest
First article inspection anchors the plan at the start of every order. Before production carries on, a thorough comparison of the initial board with the design is performed. Values, orientation, polarity and solder quality are confirmed, so a setup error cannot spread through the batch. The sample checks that follow rest on that foundation, and they mean little if the first article was rushed.
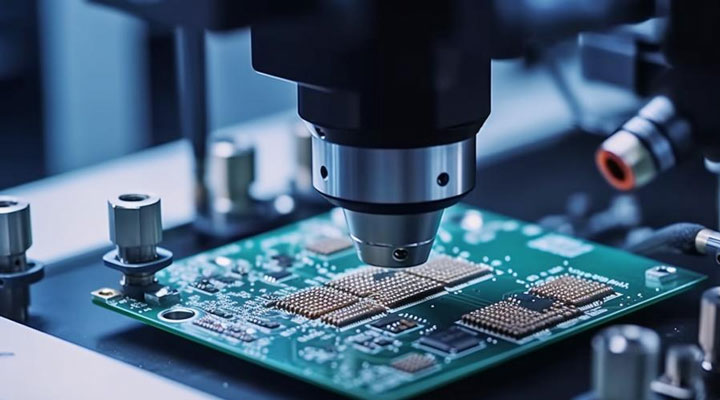
After the run, automated optical inspection screens every board, and samples move to electrical test. That pairing proves both the joint and the circuit before packing, and it forms the core of a practical PCBA testing plan. Traceability closes the loop. The factory records the program, the material reels, the operator and the findings, so a field return months later can be traced to its cause.
Sampling Across the Build Route
The plan must follow the board through every stage, not just the final one. A mixed-technology board passes through paste print, placement, reflow and often through-hole work. Each stage adds its own defect modes, and each deserves its own sample point. A plan that samples only at the end will detect problems late, when rework is expensive and the cause is hard to isolate.
This is why the second look maps the plan onto the actual route. If a board runs through PCB assembly with selective soldering, the plan should sample that step too. Buyers who receive a plan without a route map should ask for one. The map shows where evidence is collected and where the batch is released on trust.
Setting Sample Sizes With Evidence
Sample sizes should follow from the defect history, not from a template. A process with a stable record can justify a smaller sample than one still finding its window. The second look compares the current plan with the last few months of inspection data. If the defect rate has fallen, the sample may be trimmed. If it has risen, the plan should tighten before volume grows.
The review should also check who signs the release. A named owner makes the plan enforceable, and it fixes responsibility when an escape occurs. When the owner changes, the plan should be re-read rather than inherited. Small governance details like this decide whether the document guides the floor or sits unopened in a folder.
Buying Decisions Around the Plan
When two factories quote the same board, the sampling plan is a fair way to compare them. A supplier that shows a written plan, the route map and the trend data is offering evidence. One that answers with a general assurance is offering a promise. The difference matters most on repeat orders, where the plan is the main control between audits.
Buyers should also ask how the factory handles a failed sample. A clear rule matters more than a strict one. The plan should say whether the lot is screened, reworked or rejected, and who decides. A factory that answers this without hesitation has used its plan. One that improvises has a document, not a control. For projects that need sourcing and assembly under one roof, turnkey PCB assembly keeps the plan and the material records in the same system.
Details That Shift the Result
Environment and material quietly change what a sample means. Solder paste behaves differently in humid air, and a component with altered plating can shift wetting without any machine alarm. A sample drawn after such a change may pass while the process has already moved. The review should confirm that material certificates and storage conditions are checked alongside the inspection data.
Training belongs here as well. An inspector who knows what a real defect looks like will catch more than one following a picture card. The plan assumes competent judgement at the bench, and that assumption needs support. Buyers can ask how inspectors are qualified and how often they are re-checked. The answer tells you whether the sample data can be trusted.
Design choices also set what sampling can achieve. Pad geometry and spacing decide how forgiving the process is, so a layout review before tooling removes defect modes that sampling would otherwise chase. Teams that invest in PCB design and layout review usually find their sampling plan easier to meet. The plan then confirms a sound process instead of compensating for a difficult one.
Keeping the Plan Current
A sampling plan should be reviewed on a schedule, not only when a customer complains. A quarterly look at defect data, sample sizes and escape reports keeps the document aligned with the line. The review should include the people who run the process, because they see drift before the reports do. Short meetings with fixed metrics work better than long audits after a failure.
The output of each review should be a written change, with a date and an owner. Changes to sample size, acceptance rules or inspection points all deserve a record. That history shows a buyer how the factory learns. It also protects the factory when a customer questions a release decision made months earlier under a plan that has since moved on.
Component supply belongs in the same cycle. A new supplier or an approved alternate can change the process, so the plan should be re-checked when the bill of materials changes. Factories that manage component procurement and sampling together catch these shifts early. The buyer then sees fewer surprises at incoming inspection and steadier yields across repeat orders.
The Takeaway for Buyers
Ask for the sampling plan in writing, with the route map, the acceptance rule and the last few months of trend data. Compare those documents across suppliers before you compare price. A plan that matches the process, names an owner and records its changes is worth more than a tighter tolerance printed in a brochure. That is the second look worth taking before the next order is placed.