PCB Sampling Plan Traceability: Following One Board
Traceability sounds abstract until a field return lands on your desk. Then the question becomes concrete: which paste batch, which placement program and which operator produced this board? A sampling plan answers a different question, namely how many boards are checked and how often. Traceability is what makes those checks useful, because a sample result means nothing if you cannot tie it back to the lot it came from.
This guide follows a single board from data release to final test. It explains what a sampling plan should record, where the records usually break down, and what a buyer should verify before approving a supplier. The focus stays on process causes and tradeoffs rather than on slogans. Every claim here rests on general assembly practice, so you can check it against your own build.
What Sampling Traceability Means
A sampling plan defines the lot size, the sample size and the accept and reject limits for each inspection step. Traceability is the chain that connects a sampled board to its material, its machine program and its test result. Without that chain, a failed sample tells you a defect exists but not where it started. With it, the same failure points to a specific paste lot, stencil or reflow profile.
The chain has three parts. The first is physical identity, meaning the panel or serial number marked on the board. The second is the record, meaning the data logged against that identity at each step. The third is the link, meaning the rule that keeps the record attached to the right unit as it moves down the line. Break any one of the three and the sample becomes an anecdote.
Where the Chain Usually Breaks
Most traceability failures happen at handoffs rather than at machines. A panel is split into single boards and the serial number stays on the panel frame. A reel is swapped mid-lot and the new lot number is written on paper but never entered into the system. A rework station repairs a joint and the repair is not linked to the original inspection result.
Each of these gaps is cheap to close and expensive to discover late. The fix is usually a rule plus a check, such as scanning the reel before the feeder is loaded. Buyers should ask how the factory handles panel-to-board identity and mid-lot material changes. The answer reveals whether traceability is a working system or a binder on a shelf.
Stackup and Marking Choices
Traceability starts in the fabrication data, long before assembly. The board outline needs room for a serial number, a date code or a two-dimensional mark. If the design leaves no clear area, the factory will place the mark wherever space allows, and readability suffers. A short review of the fabrication drawing prevents that outcome.
Marking method matters too. Laser marking is durable but needs a suitable surface finish. Labels are easy to apply but can fall off in reflow or cleaning. Etched marks survive the process but take board area. The right choice depends on product life, cleaning steps and how the board will be read in the field.
Process Control on the Line
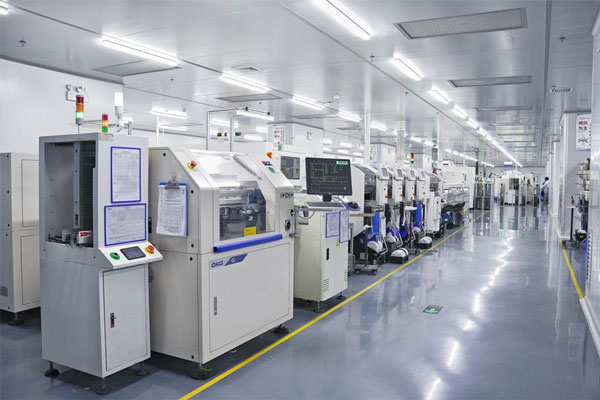
It is the entire chain, rather than any one machine, that determines the result. The design fixes pad sizes and spacing, the printer controls solder volume, the placement machine positions each part and the reflow oven forms the joints. Each step feeds the next, so the sampling plan should cover every step rather than only the final look.
Good SMT PCB assembly ties those steps together with shared data. Solder paste inspection reports volume and offset per pad. Placement data shows feeder errors and nozzle misses. Reflow profiles are logged per product. When these three records share a lot number, an engineer can trace a defect back to its cause in minutes instead of days.
A sampling plan should state which step is sampled, how often and by what method. The plan must also define the outcome in the event that a sample fails. Does the lot get quarantined, reworked or scrapped? Who signs off on the disposition? A plan without a failure rule is only a schedule of inspections, not a control system.
Material and Setup Records
Material records carry as much weight as machine data. A component that quietly changes its plating, a paste batch with different viscosity or a reel stored in humidity can shift the process with no machine warning. The factory should log paste lot, component lot and stencil identity against the build.
Setup records matter for the same reason. Which program ran, which feeders were loaded and who performed the changeover all belong in the batch file. When a field return arrives months later, that file is the fastest route to the cause. As a normal part of each order, buyers should request these records.
Inspection and Test Coverage
Inspection catches defects before they ship, but its real value is the feedback it gives. If a joint fails, the engineer can determine whether the cause was paste print, placement or reflow. That closed loop between inspection and process control is what pushes defect rates down over time. A sampling plan that feeds data back is worth more than one that only sorts good from bad.
Boards that pass visual checks still need electrical verification. A cracked joint or a wrong component often shows up only under power. In-circuit test, functional test and burn-in each add a layer of confidence. A structured PCBA testing program links each result to the board identity, so a failure can be traced to its lot and its process step.
Test coverage is a tradeoff, not a free good. More coverage costs time and fixture expense, while less coverage leaves risk in the field. The right balance depends on product criticality and volume. Buyers should ask which faults the test program can actually detect, and which ones it cannot.
Documentation and Quality System
Documentation matters as much as hardware. The batch record should show the program, the materials, the operator and the inspection findings. It should also show any rework and the test result after rework. Records that are simple to retrieve when requested are usually maintained truthfully throughout production.
A real quality management system keeps these records under revision control. Procedures state who records what and when. Calibration dates are tracked. Nonconforming lots are held until disposition. Buyers can test this by asking for a sample batch file from a recent build and checking whether the entries are complete and consistent.
Improvement should be scheduled rather than triggered by a crisis. Parameters drift, materials change and operators rotate, so the factory should review its data regularly. Ranking the top defects and removing them one at a time lowers defect rates and shortens lead times. Factories without data tend to repeat the same mistakes at the same cost.
Prototype and Volume Planning
Prototypes are the cheapest place to make mistakes. Before thousands of boards are committed, the first small batch shows pad geometry issues, component tolerances, and process behavior. Treat the design review and the pilot run as part of the project rather than as an extra expense. Buyers who invest here usually reach volume faster.
Services such as rapid PCBA prototyping help because they keep the same traceability rules at low volume. A pilot lot that is fully recorded becomes the reference for the volume build. When the process moves to high-volume PCB assembly, the sampling plan can be adjusted for lot size while the record structure stays the same.
Volume changes the sampling math. Larger lots allow smaller sample fractions at the same confidence, but they also raise the cost of a missed defect. The plan should be reviewed when volume changes, not simply copied from the prototype. Ask the supplier how the plan scales and who approves the change.
What to Verify Before You Approve
Start with the marking rule. Confirm that every board carries a unique identity that survives assembly and cleaning. Then ask for the batch file from a recent run and check that materials, programs and test results are all present. Finally, ask what happens when a sample fails, and who has authority to stop the lot.
Training deserves a place on that list. Before adjusting a parameter window, operators need to understand the reason it exists. Inspectors must know what a real defect looks like. Engineers need the ability to give an explanation when something in the data changes. What converts written procedures into daily practice is the knowledge held by people on the floor.
The takeaway for buyers is simple. Ask for one board and its full record, then follow the chain backward from the test result to the paste lot. If every link is present and readable, the sampling plan is doing its job. If a link is missing, fix that before you place the volume order.