PCB Operator Training Review: A Second Look at the Line
Operator training rarely fails loudly. It fails quietly, through a parameter adjusted without reason or a defect passed without recognition. A second look at how a factory trains its people shows whether the written procedure survives contact with a real shift. This review covers what a training program should contain, how to audit it, and which records prove it works. The goal is a line that produces the same result on Monday and on Friday.
Most buyers audit equipment and certificates, then accept training claims at face value. That order is backwards. Machines are calibrated on a schedule, but people make judgment calls every hour. A capable operator catches a drifting paste print before scrap grows. A poorly trained one keeps pressing start. The difference never appears in a quotation, yet it decides yield, rework cost and delivery reliability across the whole program.
What Training Actually Covers
Training is not a single induction session. It divides into machine skills, process understanding and defect recognition, and each needs its own practice time. Machine skills cover setup, program loading and safe operation. Process understanding explains why a parameter window exists. Defect recognition teaches what a real fault looks like under the scope. A program that covers only the first part produces operators who can run a line but cannot protect it.
Process understanding is the part most often skipped. An operator who knows why reflow soak time matters will question a profile that looks wrong. One who has memorized only the numbers will adjust until the screen stops flashing. That difference shows up in how quickly a shift reacts to an alarm. It also shows in how often the same fault returns. Ask during an audit how the reasoning behind a parameter is taught, not just the value.
Auditing the Training Record
A training claim should leave a paper trail. The record usually holds a skills matrix, signed sign offs, dates and the name of the trainer. Check that the matrix matches the stations actually running on the floor. A matrix listing ten trained operators means little if only two are on shift. Look for refresher dates and for re qualification after a process change. Production records tend to be maintained truthfully when they can be readily provided upon request.
Ask to see how a new operator is released to work alone. The strongest factories use a supervised period with a signed checklist and a first article built under observation. The weakest simply pair a newcomer with whoever is free. Neither approach appears in a brochure, but both are visible in a short walk through the plant. The answer tells you more about quality culture than any certificate on the wall.
Setup Discipline on the Floor
Practical control starts before the first board runs. Operators verify the program, the tooling and the materials against the job packet. They confirm the paste lot, the feeder positions and the stencil condition. Engineers then monitor paste volumes, placement offsets and oven temperatures during production rather than waiting for the batch to end. Deviations are corrected while they are still small and cheap to fix.
That routine keeps SMT PCB assembly predictable even when the product mix changes. Changeover is where training shows most clearly. A trained team follows a written sequence, checks the first article and records the result. An untrained team improvises and hopes the next inspection catches problems. Ask how changeover is sequenced and who signs the release. The answer reveals whether setup discipline is a habit or a slogan.
Defect Recognition and Feedback
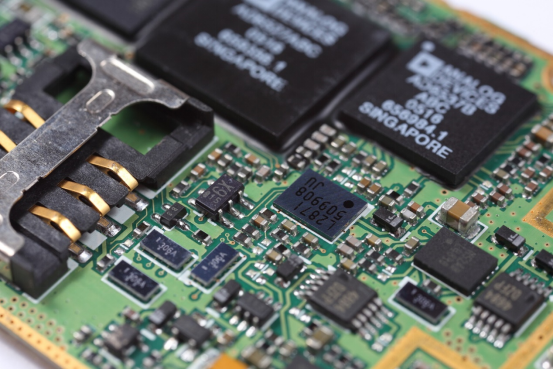
Inspection only works when the person at the scope knows what to reject. Training should include real examples of bridging, tombstoning, insufficient fillet and disturbed joints. Operators need a boundary between a cosmetic mark and a functional fault. Without that boundary, good boards are scrapped and bad ones ship. Both errors cost money, and both trace back to how defect recognition was taught and refreshed.
Feedback closes the loop. When a defect is found, the finding should reach the operator who built the board, not just the quality file. A short daily review of the top defects teaches more than an annual classroom session. Factories that rank defects and remove them one by one gradually lower their rates. Factories without feedback repeat the same mistakes at the same cost, month after month, without noticing.
Materials and Supplier Risk
Suppliers and materials carry risks that no machine alarm will catch. A component that quietly changes its plating, a paste batch with different viscosity or a reel stored in humidity can all shift the process. Trained operators notice these changes because they check labels and certificates as routine. They flag a substitution before it reaches the line. That habit depends on training that explains why material control matters, not just how to scan a barcode.
Professional factories qualify materials, check certificates of analysis and approve alternates in advance. Operators should know where to find that approval and whom to call when a reel does not match. This connects directly to component procurement, because sourcing decisions made weeks earlier land on the line as physical parts. A buyer should confirm that incoming material checks exist and that the floor staff are trained to use them.
Test Coverage and Traceability
Once the run is complete, all boards go through automated optical inspection, and samples are sent for electrical test. First article inspection plays a special role at the start of each order. Detailed checks of the first board against the design cover values, orientation, polarity, and solder quality. By catching a setup error, that check stops the whole batch from being affected by it. It also tests whether the operator understood the job packet, which is a training question as much as a quality one.
Traceability turns good intentions into proof. The factory records which program ran, which reels were used, which operator handled the job and what inspection found. When a field return arrives months later, that record is the fastest route to the cause. It also shows whether the operator on that shift was trained for the station. A documented quality management system depends on these records being complete and honest.
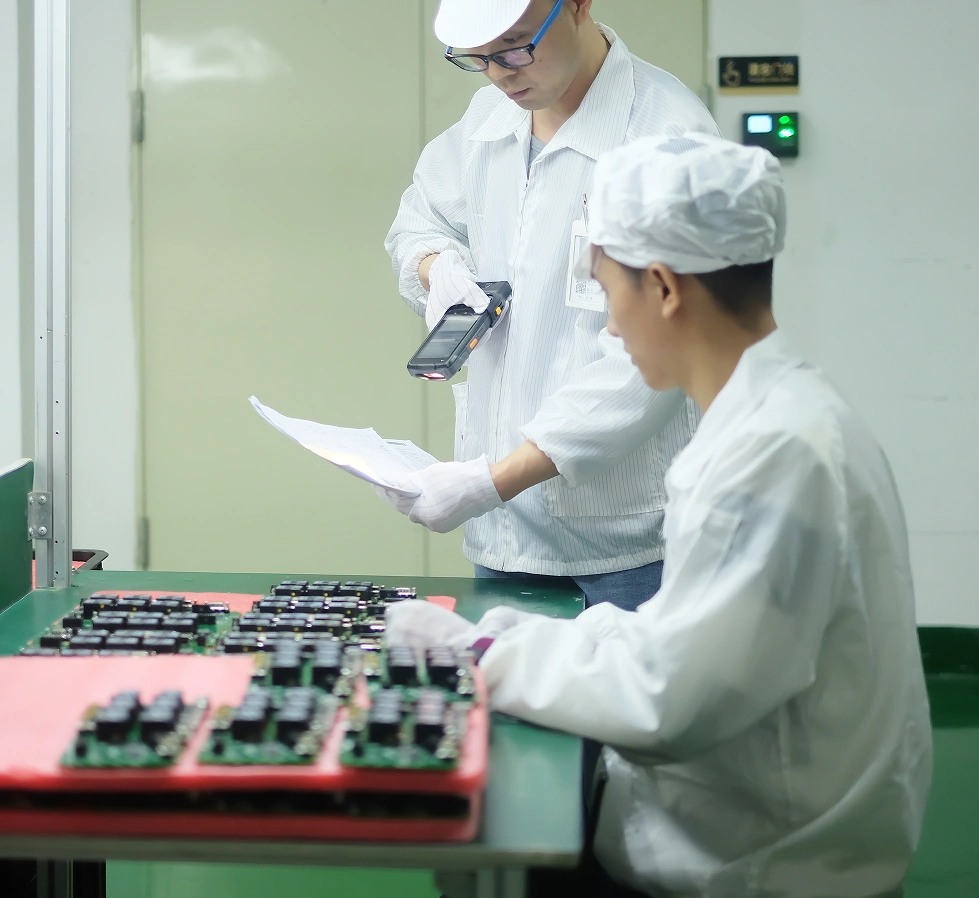
Prototypes as Training Ground
Prototypes are the cheapest place to make mistakes. The first small batch reveals pad geometry issues, component tolerances, and process behavior before thousands of boards are committed. It also reveals training gaps, because a new product forces operators to read a new job packet and apply familiar rules to unfamiliar parts. Consider the pilot run to be part of the project, not an additional cost. Buyers who invest here reach volume faster.
Rapid PCBA prototyping compresses that learning into days instead of weeks. The same operators who will run volume build the pilot, so their questions surface early and the process notes improve before the big order. Ask whether the pilot team stays with the product into production. Continuity matters more than speed alone, because knowledge built during the prototype is wasted if the volume line starts from scratch.
Comparing Suppliers on Training
When suppliers are compared, training should be checked with the same rigor as equipment. Ask for the skills matrix, the release procedure for new operators and the refresher schedule. Ask how process changes are communicated to the floor and how quickly. Ask who signs a first article and what happens when it fails. These questions are easy to answer in a well run factory and awkward in a poorly run one. The hesitation itself is useful information.
Scale matters too. A partner running high-volume PCB assembly trains continuously because shifts rotate and products change. That routine builds a depth of practice a small shop cannot match. The buyer benefits through fewer repeated mistakes and faster response when something drifts. Price per board still matters, but it should be weighed against the cost of rework, field returns and late deliveries that weak training quietly produces.
What to Verify Before You Commit
Before releasing a program, confirm four things in writing. The skills matrix should cover every station in the route. The release procedure for new operators should include supervised work and a signed first article. Refresher training should follow any process or material change. Records should be retained against the part number so a repeat order starts from the same point. None of these items adds significant cost, and each removes a risk from the schedule.
Then walk the floor and watch a changeover. You will see whether the written procedure is followed, whether the job packet is actually read, and whether anyone checks the first board with care. Training is visible in ordinary behavior, not in certificates. A second look at operator training is really a second look at how the factory behaves under normal pressure. That evidence is what a stable supply relationship should be built on.