Flying Probe Test for Irrigation Valve Control Boards
An irrigation valve control board mixes a low-voltage logic section with driver stages that switch solenoids. Flying probe test checks that board without a dedicated fixture, using moving probes to contact pads and vias. That makes it a practical choice for prototypes, small lots and designs that change often. This review covers what the test proves, where it falls short, and what buyers should confirm before release.
The test program decides most of the outcome. Probe coordinates, net lists and pass limits come from the design data, so any gap in that data becomes a gap in coverage. Engineers should treat the program as a deliverable, not an afterthought. A board that passes a weak program still ships with risk attached to it.
What Flying Probe Test Covers
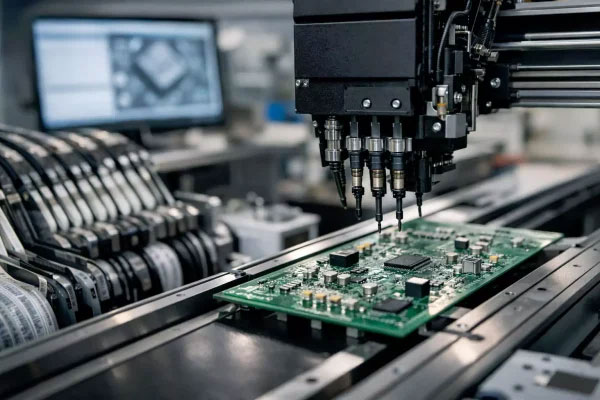
A flying probe system moves a few probes across the board surface under software control. It measures continuity, isolation and component values at defined points. On an irrigation controller, that means checking the valve driver traces, the relay coils, the sensor inputs and the power rails. Opens, shorts and wrong or missing parts show up quickly.
Coverage depends on access. Probe needles need a clean pad or via to land on, and tall components can block the approach. Designers should keep test pads on every net that matters and avoid placing them under connectors. A short review of pad access before fabrication prevents most coverage arguments later.
Where the Method Falls Short
Flying probe test is electrical, not visual. It confirms that a connection exists at the moment of contact, but it cannot see a weak solder joint that fails under heat. It also struggles with fine cracks that open only after thermal cycling. Buyers should pair it with automated optical inspection for solder quality and with functional test under load.
Speed is the other limit. Probing one board at a time suits small and medium volumes, but it becomes a bottleneck on large orders. Above a certain quantity, a fixture-based in-circuit tester usually pays for itself. The crossover point depends on board size, node count and the number of lots per year, so ask for the comparison in writing.
Stackup Choices and Test Access
The layer stack affects how much the probes can reach. A simple two-layer board leaves most nets exposed on the bottom side, which is easy to probe. Multilayer boards bury inner traces and force test points to the outer layers. Each buried net needs a via or pad brought to the surface, and that consumes routing space.
Designers should plan test access alongside routing rather than after it. Adding pads late often pushes traces into tight corners and raises fabrication risk. A clean plan keeps probe targets on a consistent grid, away from tall parts and board edges. It also keeps the probe travel short, which trims test time per board.
Ground and power planes deserve their own review. A probe that lands on a plane pad measures the whole plane, not a single net, so the reading can hide a broken connection elsewhere. Designers should keep plane contacts separate from signal targets and label them clearly in the data. That small habit prevents false passes that look like good boards until the field returns begin.
Program Development and First Article
The test program starts with the net list and the bill of materials. Engineers map each net to a probe target, set pass limits for each component, and define the order of measurements. That work takes time on the first build and less on later revisions. A well-kept program library shortens every future launch.
The first article deserves special attention. One board is probed in full, and every failure is traced to its cause before the line continues. This step catches data errors, wrong component values and missing test points while the fix is still cheap. Skipping it often means the same fault repeats across the whole lot.
Probe maintenance belongs in the same schedule. Needles wear, bend and pick up solder debris, and a dull tip makes poor contact on small pads. A factory should log probe cleaning and replacement against the test results, because a sudden rise in false failures often points to the hardware. Buyers can ask for that log and compare it with the failure trend.
Debugging Valve Driver Faults
Driver stages are the usual source of trouble on these boards. A solenoid channel may read correct at low current and fail when the coil energizes. Flying probe test can confirm the driver transistor and its gate resistor, but it cannot prove the channel under real load. A powered functional check closes that gap.
Engineers should define which channels get a load test and which get only a static check. The choice depends on how the valve is used in the field. A channel that switches often deserves more scrutiny than one that stays closed. Writing that rule into the test plan keeps the coverage honest and the cycle time reasonable.
Flyback and clamp diodes are another weak point. A probe can confirm the diode is present and reads correctly in one direction, yet a slow or leaky part can still stress the driver over time. The test plan should state whether these parts get a value check only or a switching check. That distinction matters for boards that drive inductive loads daily.
Records and Traceability
Every probe result should be stored against the board serial number. The record shows which program revision ran, which measurements failed and what was reworked. When a controller returns from the field, that history is the fastest way to find the cause. It also shows whether the fault is isolated or part of a trend.
Buyers should ask for the program revision alongside the test report. A report without a revision number proves little, because the limits may have changed since. Factories that keep this link intact can answer a field question in hours. Those that cannot often end up rebuilding the test from scratch.
Test data also feeds process improvement. When one net fails more often than others, the cause may sit in printing, placement or reflow rather than in the test itself. Reviewing failures by net and by component type reveals those patterns. The fix then lands in the process, not in the test limits.
Supplier Questions Before Release
Ask how the probe targets were chosen and whether every critical net has one. Ask which defects the program can detect and which it cannot. Ask for the first article report and the program revision. These questions separate a real test plan from a checkbox on a quotation.
It also helps to confirm how the supplier handles rework after a failed probe. A board that is repaired needs a repeat test, and the record should show both results. Without that step, a repaired board can ship with an untested joint. The same discipline applies to any PCB assembly run with mixed technology.
Volume plans belong in the same conversation. If the product will scale, ask when a fixture tester becomes cheaper than probing. A supplier that offers high-volume PCB assembly can usually model that crossover with real numbers. That answer shapes the test strategy for the next two years.
Component sourcing affects test results more than buyers expect. A substitute part with different tolerance may fail a limit that the original passed. Suppliers who manage component procurement well will flag those changes before they reach the line. That warning protects the test program and the delivery date.
Design changes also reset the program. A new layout moves probe targets, so the program needs a fresh review and a new first article. Teams that plan a PCB design and layout revision should tell the test engineer early. Late notice forces rushed edits and weak coverage.
For buyers who want one partner across fabrication, assembly and test, a turnkey PCB assembly route keeps the data in one place. The test program, the inspection records and the build documents then share a single history. That continuity is worth more than a small price difference between quotes.
The practical takeaway is simple. Treat the flying probe program as part of the design, confirm probe access before fabrication, and require the first article report with its revision number. Those three steps cost little at the start and prevent most field surprises on irrigation valve controllers.