COB Packaging on HDI PCB: Features and Proofing Checks
Bare dies bonded straight onto a dense board change what a prototype must prove. Chip on board removes the plastic package, so the PCB surface becomes the package. On an HDI stackup, that shift touches pad finish, wire bond placement, encapsulation and test access at the same time. This guide covers how COB works on HDI boards, where it fits, and what to verify during proofing before volume begins. It is written for engineers and buyers who must approve a first article, not just read a datasheet.
What COB Packaging Does
COB stands for chip on board. A bare semiconductor die is attached directly to the PCB surface with adhesive, then connected to board pads by fine bonding wires. A protective epoxy or resin covers the die and wires. The dark blob on many boards is that encapsulation, not a component. Removing the external package shortens the electrical path and saves height. It also moves mechanical and environmental protection onto the board itself, so the PCB finish and the assembly process carry more of the reliability burden.
The process has three core steps. Die attach places the chip with high positional accuracy. Wire bonding joins die pads to board pads using gold or aluminum wire. Encapsulation then seals the area against moisture, vibration and handling damage. Each step has its own window, and each depends on the one before it. A die placed slightly off center can still bond, but the wire loop may touch the neighboring pad. That is why COB proofing checks placement and bonding together rather than as separate items.
Why HDI Boards Suit COB
HDI boards use finer lines, smaller vias and denser routing than standard boards. That density matters for COB because the die sits close to its supporting parts. Short traces from die pads to decoupling capacitors reduce inductance and improve signal quality. Microvias and buried vias free surface area for the die footprint and its bond pads. The result is a compact module with fewer connectors and shorter loops. For products with tight height limits, this combination often decides whether the design fits at all.
There is a tradeoff. HDI fabrication needs tighter registration between layers, and COB needs a flat, clean bond surface. A small shift in via position or surface finish can affect wire adhesion. Buyers should confirm that the fabricator controls surface finish and planarity on the bond side, not only the routing density. Ask how the shop handles pad finish choice for wire bonding, because not every finish suits gold or aluminum wire. That single question separates a capable supplier from a hopeful one.
Stackup and Surface Choices
The stackup decides how flat the bond area stays after lamination and reflow. Thin dielectric layers and controlled copper balance help limit local warpage under the die. If the board bows, the die attach adhesive cures unevenly and wire bonding becomes harder. Engineers should keep copper distribution reasonably even around the die site and avoid large open areas next to dense routing. These choices cost little at layout and are expensive to fix after tooling.
Surface finish is the next decision. Bond pads need a finish that stays solderable and bondable through assembly. Some finishes suit wire bonding well, while others need a different pad treatment. The fabricator and the assembly house should agree on the finish before the first panel is built. Buyers should request the finish on the drawing, not in a side message, so the production lot matches the approved sample. For related process detail, see our notes on SMT PCB assembly.
Proofing Checks That Matter
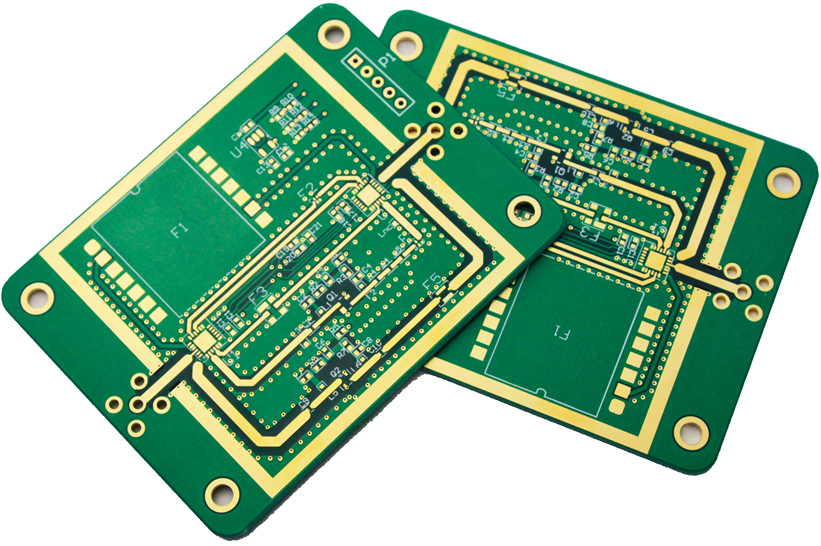
Proofing is where COB designs usually fail first. The prototype must confirm die attach accuracy, wire bond pull strength and encapsulation coverage. It must also confirm that the HDI routing supports the die site without opens or shorts under the blob. Standard electrical test cannot probe under the encapsulant, so test access must be planned at layout. Add test pads on outer layers and keep them clear of the die area. A prototype that cannot be tested tells you very little about yield.
Component and material choices deserve the same attention. The die, adhesive, wire and encapsulant must be compatible with each other and with the board finish. Ask for the material set and confirm it before the pilot run. Where parts come from several sources, a documented incoming check helps. Our component procurement process covers traceability from reel to board, which matters when a bare die has no package marking to identify it later.
Applications and Fit
COB on HDI boards appears in camera modules, wearables, portable audio and compact sensors. LED lighting also uses the approach, with multiple chips mounted on one substrate for a small, bright source. Industrial control modules use it where space is tight and vibration is present. Medical devices use it where a small, sealed assembly helps. In each case the driver is the same: less height, fewer joints and a shorter path from die to circuit.
Fit matters more than fashion. COB suits high-volume products where the die is stable and the process is tuned. It suits designs that can tolerate rework limits, because a failed die under encapsulant is often a scrap board. For low-volume or frequently revised designs, a packaged part may cost less overall. Engineers should compare total cost, including yield loss and test difficulty, before committing. Rapid iteration is easier with packaged parts, while rapid PCBA prototyping can still validate a COB design when the process is set up early.
Assembly and Quality Control
COB assembly sits inside the wider SMT flow. Solder paste printing, placement of surrounding parts and reflow all happen before or around the die process. Order matters, because reflow temperatures can affect adhesive and encapsulant if the sequence is wrong. The assembly house should document the sequence on the process sheet. Buyers should confirm that the die area is protected during later steps and that cleaning does not damage the bond wires. These details are easy to miss in a quotation.
Quality control for COB relies on inspection plus sample testing. Visual checks look for wire sweep, voids and incomplete coverage. Bond pull and shear tests on samples confirm the wire and die attach strength. Electrical test confirms function where test pads allow. Records should link each lot to its material set and process settings. Our quality management system keeps these records with the lot, so a field question can be traced back to the build that produced the board.
Scaling to Volume Production
Volume changes the risk profile. A process that works on ten boards may drift on a thousand, because adhesive age, wire tool wear and encapsulant viscosity all move over time. The factory should define windows for each and check them on a schedule. First article approval should include the die attach program, the bond recipe and the cure profile. Buyers should ask which parameters are recorded per lot and which are checked only at setup. The answer shows how much control actually exists.
Volume also exposes supply risk. Bare dies come from wafer lots, and a change in lot can shift bond pad metallurgy. Encapsulant batches can change flow behavior. A supplier that qualifies alternates and checks incoming material reduces the chance of a mid-run surprise. For programs with steady demand, high-volume PCB assembly planning should include die and material lead times, not just board fabrication slots. That planning keeps the line running when one input is delayed.
What Buyers Should Verify
Before releasing a COB HDI order, confirm four things in writing. The surface finish on the bond side must be stated on the drawing. The test access plan must be agreed, including pads that remain reachable after encapsulation. The material set for die attach, wire and encapsulant must be fixed and recorded. The process sequence must show where reflow sits relative to die attach and cure. Each item is simple to check and costly to discover late.
Then ask for the first article report. It should show placement accuracy, bond test results on samples, encapsulation coverage and electrical test outcome. It should also list any deviation and how it was closed. A report that only says pass or fail is not enough for a COB build, because the process has several independent windows. The takeaway is direct: treat COB on HDI as a process qualification, not a part substitution.
Approve the material set and test access first, then release volume only after the first article report shows each window under control.