Rapid PCB Prototype Delivery: How Fast Can It Be?
Prototype speed is usually quoted as a single number, yet that number hides the work behind it. A two-layer board can leave the factory in a day, while a ten-layer board needs lamination cycles that cannot be compressed. The real question is not how fast any board can ship, but how fast your board can ship without skipping a check. This review sets out where the hours go and what a buyer can verify before placing an order.
Delivery time starts with the design file, not with the machine. A clean Gerber set, a confirmed stackup and an approved material list remove most of the waiting that buyers blame on the factory. When those inputs arrive incomplete, engineering questions and revisions consume days before production begins. Engineers and buyers who plan the file handover carefully usually find that the quoted lead time is met or beaten.
Layer Count Sets the Baseline
Layer count is the strongest single driver of prototype lead time. A two-layer board needs imaging, etching, drilling and finishing on one core. A multilayer board adds inner-layer imaging, multiple lamination cycles, controlled depth drilling and stricter registration checks. Each added pair of layers brings another bonding step, and those steps run on a fixed cycle rather than on demand. That is why the fastest schedules cluster at the low end.
As a general guide, simple two-layer prototypes can move through a well-organized shop in about a day. Four-layer boards typically need two days, and six to eight layer boards need roughly three. Boards in the ten to eighteen layer range often need four days or more. Above twenty layers, a week is a realistic expectation for a first article. These figures assume standard FR-4 and a clean file.
Board size and quantity also matter, but less than most buyers expect. Small prototype panels share tooling and travel through plating and etching together, so a handful of boards costs almost the same process time as a few dozen. Very large panels or unusual outlines can slow the line because they need special fixtures. Buyers should state panel dimensions early so the factory can plan the routing step.
Stackup Choices and Material Supply
Material selection changes the schedule in two ways. Common FR-4 laminates sit in stock at most factories, so a standard stackup starts immediately. High-TG laminates, low-loss materials and specialty films are often ordered in, which adds procurement time before the first panel is built. The same applies to heavy copper and aluminum cores, which need different plating and etching parameters. Choosing an in-stock material is the simplest way to protect a tight deadline.
Stackup decisions also affect how many lamination cycles the board needs. A symmetric build with standard prepreg flows predictably and passes registration checks on the first attempt. An asymmetric or unusually thin build may need trial panels and coupon checks before the production lot runs. Engineers should confirm the stackup with the factory during PCB design and layout, because a small change there can remove an entire day from the schedule.
Impedance requirements add a verification step. Controlled impedance traces need coupon testing and, in some cases, a tuned trace width before the lot is released. That work is quick when the stackup is standard and slower when the dielectric is unusual. Buyers should tell the factory about impedance targets at quotation, not after the files are released, so the test coupon is planned into the first panel.
Engineering Review Before Tooling
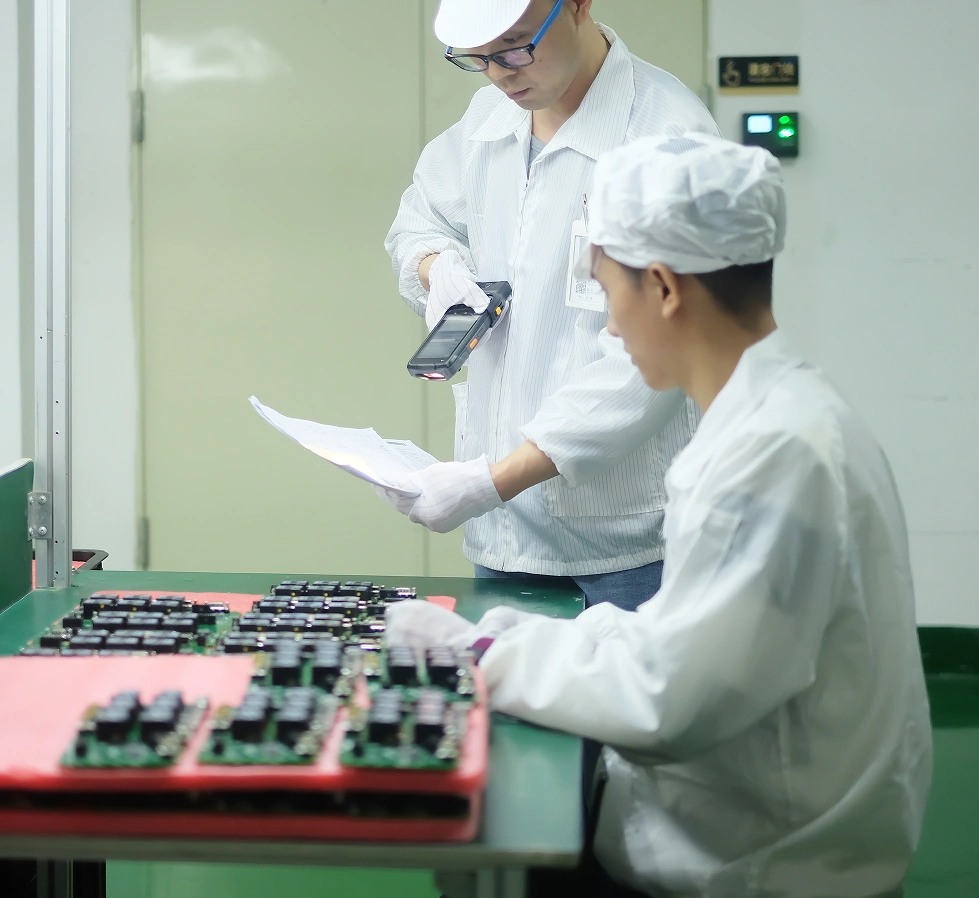
Every fast job passes through a design for manufacturability review. The reviewer checks annular ring, solder mask clearance, drill sizes, copper-to-edge spacing and minimum line width against the factory’s capability. Most issues are minor and can be corrected in the file within hours. A few, such as a missing drill table or an ambiguous outline, need a customer decision and can stall the job. A complete file package prevents that stall.
The review also confirms the fabrication drawing, the surface finish and the tolerance callouts. Ambiguity here is expensive, because the factory must either guess or ask. Guessing risks a scrapped lot, and asking costs a day. Engineers should send one clear drawing with the finish, thickness, copper weight and any special notes stated once. Duplicated or conflicting notes are a common cause of avoidable delay.
Fabrication Steps That Cannot Be Rushed
Once tooling is released, the panel follows a fixed sequence. Inner layers are imaged, etched and inspected, then bonded in a lamination press. Drilling follows, then plating, outer-layer imaging and etching. Surface finish, solder mask and legend come next, and the panel ends with electrical test and final inspection. Some steps run in parallel, but lamination and plating have cycle times set by chemistry and temperature, not by scheduling pressure.
Drilling deserves separate attention on dense boards. Small holes, high aspect ratios and tight registration all slow the drill program and increase bit wear. A board with many small vias may need a slower feed rate and more frequent bit changes, which adds hours. Designers can help by keeping the drill count reasonable and by using standard finished hole sizes wherever the circuit allows.
Test Coverage and Final Checks
Electrical test is not a formality on a prototype. A netlist-driven flying probe or fixture test confirms that the board matches the design before it ships. Test program generation takes time on a new design, especially when the netlist is large or the pads are fine pitch. Factories that generate the program while the panel is in fabrication save hours, and that parallel work is a mark of a well-run prototype line.
Visual and dimensional checks follow test. Automated optical inspection catches mask and trace defects, while a final look confirms the finish, the legend and the outline. Buyers who need traceability should ask which records travel with the boards. A lot record showing the program, the panel number and the inspection result is far more useful than a certificate alone. The practices behind those records are described under quality management.
What Buyers Should Verify
A fast quote means little without a matching process. Buyers should ask how the factory handles engineering questions, whether the quoted time includes test program generation, and what happens if the file needs a change. A supplier that answers these points clearly is usually the one that meets its dates. Vague answers about capacity or priority often precede a missed shipment, so the questions are worth asking early.
Priority handling is another point to confirm. Some factories run prototype orders through a dedicated channel with reserved press and drill time; others simply slot them into the standard queue. The difference shows up when the line is busy. Buyers with a hard deadline should ask for the priority policy in writing, including what triggers a schedule change and how quickly the factory communicates it.
Assembly adds its own timeline when the prototype needs parts placed. Component sourcing, stencil making and programming all take time before the first board is built. Buyers who plan fabrication and assembly together avoid a second wait. Services such as turnkey PCB assembly combine both stages under one schedule, which usually shortens the total path from file to working board.
Planning a Realistic Schedule
The fastest realistic schedule comes from a clean file, a standard stackup and an in-stock material. Add a day for each unusual requirement, such as a specialty laminate, a tight impedance target or a dense drill pattern. Add more when assembly is involved, because parts must arrive before the line can run. A schedule built this way is honest, and it gives the factory room to do the checks that protect the design.
Prototypes are the cheapest place to find a mistake. A board that ships a day later but passes test is worth more than a rushed panel that fails in the lab. Engineers should treat the first article as a learning step and keep the lot records for comparison. When the design moves toward volume, those records support a smoother transfer into high-volume PCB assembly without repeating old problems.
Component supply can quietly break a fast schedule. A part on allocation or a long lead-time connector may arrive after the bare board is finished. Buyers should confirm availability before release and approve alternates in advance. Early work on component procurement keeps the assembly date tied to the board date rather than to a late shipment. That single step prevents many missed prototype deadlines.
The practical takeaway is simple. Ask for a lead time that names each stage, from file review to shipment, and check that test and inspection are inside it. Confirm the material is in stock and the stackup is standard. Then hold the schedule against the lot record when the boards arrive. A supplier that can explain its timeline in stages is usually the one that can deliver a working prototype on the date it promised.