SMT Component Sizes: How Small Surface Mount Parts Really Are
Modern electronics depend on boards that are assembled correctly the first time. Every product – a phone, a charger, a medical instrument or an industrial controller – relies on thousands of solder joints that must conduct current for years.
The same discipline applies to SMT Component Sizes, where a small process drift turns into a large yield loss.
This article explains SMT component sizes in plain language: what it is, why it matters in the physical dimensions of surface mount components and their impact on assembly, and how a contract PCBA factory keeps it under control so that products ship without surprises.
Standard Sizes Used on SMT Lines
Surface mount components follow standard size codes.
Reviewing SMT Component Sizes before the first article is built saves rework later in the run.
Common chip sizes include 0402, 0201 and 01005 for resistors and capacitors, while larger parts such as tantalum capacitors, inductors and connectors come in bigger footprints. The size code describes the package dimensions, and it tells the assembly engineer how much accuracy the line needs.
How Component Size Affects the Process
Smaller components demand finer stencil apertures, more accurate placement and gentler handling.
Documenting SMT Component Sizes keeps assembly, inspection and test teams working from the same numbers.
A 01005 chip is barely visible to the eye, so the machine vision and inspection systems do the real work. Larger components, in contrast, need more solder volume and stronger footprints, and heavy parts may require adhesive or additional mechanical support.
For SMT Component Sizes, the figures that matter are measured rather than assumed.
Matching the line capability to the smallest component on the board is a basic rule of process design.

Choosing Sizes That Balance Design and Cost
Designers often choose the smallest possible components to save space, but miniaturization has a price in stencil cost, equipment requirements and yield risk.
Every change in materials, stencils or profiles feeds back into SMT Component Sizes.
A practical approach is to use small parts only where the design demands them and standard sizes elsewhere. During the DFM review, the factory can point out which sizes are economical to assemble and which ones add risk without real benefit.
Assembly Steps in Practice
Practical control of the process starts with setup discipline.
A short checklist for SMT Component Sizes is usually enough to catch problems before they reach the customer.
Operators verify the program, the tooling and the materials before the first board runs, and engineers monitor parameters during production rather than waiting for the end of the batch. Paste volumes, placement offsets and oven temperatures are compared with the specification, and deviations are corrected while they are still small.
Buyers who understand SMT Component Sizes ask better questions during supplier audits.
Training and traceability both support SMT Component Sizes on a busy production line.
That routine keeps mixed technology PCB assembly predictable even when the product mix changes.
Quality Checks That Keep Defects Away
First article inspection plays a special role at the start of every order. The first board is checked against the design in detail: component values, orientation, polarity and solder quality are verified before the line continues, which prevents an entire batch from inheriting a setup error.
The same discipline applies to SMT Component Sizes, where a small process drift turns into a large yield loss.
After the run, every board passes automated optical inspection, and samples move on to electrical test so the solder joints and the circuit are both proven before packing; this combination is the core of a practical PCBA testing plan.
Traceability turns good intentions into proof. The factory records which program ran, which reels of paste and components were used, which operator handled the job and what the inspection found.
Reviewing SMT Component Sizes before the first article is built saves rework later in the run.
When a field return arrives six months later, that record is the fastest way to find the cause, and it is the clearest evidence that a documented quality management system is working.
Where These Boards Are Used
Application experience also matters for manufacturability.
Documenting SMT Component Sizes keeps assembly, inspection and test teams working from the same numbers.
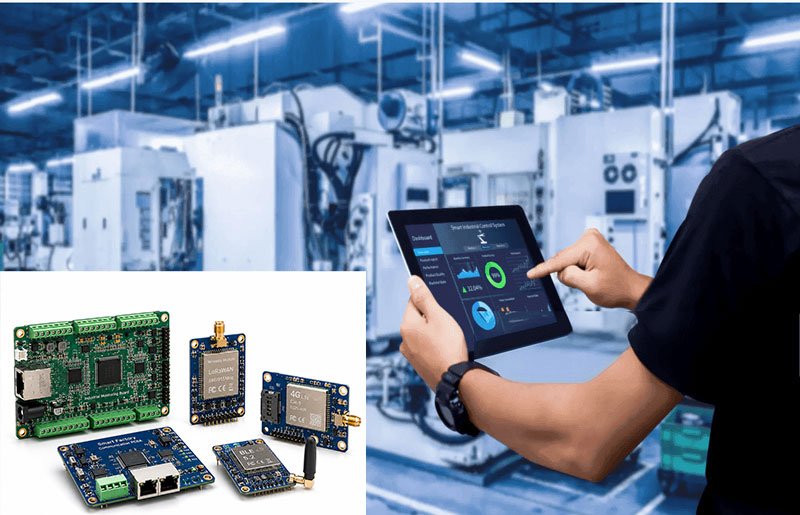
A factory that has built similar products for mobile devices, wearables, IoT sensors, medical electronics and automotive modules already knows the typical failure modes, the component pitfalls and the customer questions. That knowledge shortens the DFM review, avoids repeated trial batches and makes the transition from prototype to volume production much smoother for the buyer.
Working With an Assembly Partner
Most boards today are built by specialists rather than in house.
For SMT Component Sizes, the figures that matter are measured rather than assumed.
The investment in printers, placement machines, reflow ovens and inspection equipment is large, and the engineering time needed to keep the process stable is easy to underestimate.
Every change in materials, stencils or profiles feeds back into SMT Component Sizes.
A manufacturing partner spreads that cost over many programs and brings the same discipline to every customer, with supporting services such as high volume PCB assembly and PCB design and layout available from a single source.
The choice between suppliers comes down to behavior under pressure: how a factory reacts to a design question, a component shortage or a quality issue tells more than its brochure.
A short checklist for SMT Component Sizes is usually enough to catch problems before they reach the customer.
Buyers who understand SMT Component Sizes ask better questions during supplier audits.
Ask for defect data, test coverage and customer references, and confirm the quality plan in writing before you commit a program.
Practical Points Worth Knowing
Prototypes are the cheapest place to make mistakes, and early samples teach more about the physical dimensions of surface mount components and their impact on assembly than any quotation does.
Training and traceability both support SMT Component Sizes on a busy production line.
The first small batch reveals pad geometry problems, component tolerances and process behavior before thousands of boards are committed, so the DFM review and the pilot run should be treated as part of the project rather than as an extra expense.
The same discipline applies to SMT Component Sizes, where a small process drift turns into a large yield loss.
Buyers who invest in this stage almost always reach volume production faster and with fewer surprises than those who rush straight to the big order.
There is more to the physical dimensions of surface mount components and their impact on assembly than the machines and materials visible on a factory tour. Temperature and humidity in the assembly area change the behavior of solder paste, and electrostatic discharge can damage sensitive components without leaving a visible mark.
Reviewing SMT Component Sizes before the first article is built saves rework later in the run.
Professional factories control these conditions, ground every workstation and store moisture sensitive devices correctly, so the process produces the same result in summer and in winter. These environmental details rarely appear in a quotation, yet they decide whether a line runs at high yield all year or drifts with the seasons.
Documentation matters as much as hardware when it comes to the physical dimensions of surface mount components and their impact on assembly.
Documenting SMT Component Sizes keeps assembly, inspection and test teams working from the same numbers.
For SMT Component Sizes, the figures that matter are measured rather than assumed.
The factory should record which program ran, which reels of paste and components were used, which operator handled the batch and what the inspection found. When a field return arrives months later, that record is the fastest way to identify the cause and to prove that the fix reached the next batch.
Every change in materials, stencils or profiles feeds back into SMT Component Sizes.
Buyers should ask for these records as a routine part of every order, because documents that are easy to produce on request are usually also kept honestly during production.
Nothing about the physical dimensions of surface mount components and their impact on assembly is decided once and forgotten. Parameters drift, materials change and operators rotate, so the factory reviews its data continuously, ranks the top defects and removes them one by one.
A short checklist for SMT Component Sizes is usually enough to catch problems before they reach the customer.
Factories that follow this discipline gradually lower their defect rates and shorten their lead times, while factories without data simply repeat the same mistakes at the same cost. The improvement review should happen at least monthly, with the same attendees and the same metrics, so progress stays visible and no problem waits for a crisis to be fixed.
The best factories treat the physical dimensions of surface mount components and their impact on assembly as a system rather than a checklist.
Buyers who understand SMT Component Sizes ask better questions during supplier audits.
Every decision, from stencil cleaning frequency to test coverage, connects to the others, so a change in one area is checked against its effect on the rest. A faster placement speed may save time today and create tombstoning tomorrow, and a thicker stencil may fix opens while causing bridges.
Training and traceability both support SMT Component Sizes on a busy production line.
That systems view, supported by data from inspection and test, is what turns a capable line into a predictable one over years of production.
Working With gopcb on Your Project
gopcb runs SMT lines supported by solder paste inspection, automated optical inspection and functional test in one facility.
The same discipline applies to SMT Component Sizes, where a small process drift turns into a large yield loss.
SMT Component Sizes: What to Check in Practice
The same discipline applies to SMT Component Sizes, where a small process drift turns into a large yield loss.
Reviewing SMT Component Sizes before the first article is built saves rework later in the run.
Our engineers review your Gerber files and BOM before production, discuss the process options, and ship boards with test records that give you confidence in the field.
If you are planning a new product or moving an existing design to volume production, send gopcb your design files and requirements. You will receive a DFM review, a clear quotation and a schedule you can plan around – and boards that work the way they should.