Reading an X-Ray Image of a BGA Solder Joint
An X-ray image of a ball grid array shows the joints as overlapping circles, and the judgement is made from the shape, the brightness and the uniformity of each one. The technique is powerful and it has limits that should be understood before it is relied on.
What the Gray Level Means
Brighter means more material along the path of the beam. A joint that is thinner or that has a void shows as a lighter or a darker region, and the effect is a sum along the whole path rather than a slice.
The overlap is why a two dimensional image is ambiguous. Our X-ray notes describe the technique in detail.
Ball Diameter and Shape
A ball that is smaller than its neighbours or that is not circular suggests a partial joint or a missing ball. The comparison is between balls in the same image rather than against an absolute size.
Consistency across the array is the practical criterion. Our joint criteria notes describe the acceptance that follows.
Voiding and How It Is Judged
A void appears as a darker region inside a ball. The usual measure is the total void area as a percentage of the ball area, and the limit is set by the product rather than by a general rule.
Many small voids and one large void behave differently. Our voiding notes describe the distinction.
Head in Pillow and Marginal Cases
A ball that has not fully reflowed leaves a gap that a two dimensional image may not resolve, because the ball and the paste are superimposed. An oblique view or a computed tomography scan is needed.
The limit of the technique should be stated in the procedure. Our inspection notes describe the alternative techniques.
Stacked and Shielded Packages
A package on package or a package with a heat spreader places more material in the beam path, and the lower joint becomes difficult to resolve. The inspection plan has to account for it.
Our reballing notes describe the rework that follows a rejection.
Setting the criteria
The criteria should be set from samples with known defects rather than from the image alone. A reference set makes the judgement repeatable between operators.
The reference set should be kept with the program. Our AOI notes describe the equivalent practice for optical inspection.
Verification
The verification is a reference sample set with documented defects, a written criterion for diameter, shape and void, and a destructive microsection on a sample to confirm that the images were read correctly.
Our quality notes describe how the records are kept.
Process Control and Verification
The process window is set by the narrowest step in the flow, so an improvement anywhere else shows up as margin rather than as yield until that step is addressed. A short note on the drawing about handling, storage or packaging is often worth more than an extra decimal place on a tolerance.
Where a value sits close to a process limit, the drawing should say so, since the shop can then open the process window rather than working to a nominal figure that carries no tolerance. A stack-up that is drawn rather than described removes most of the ambiguity from a quotation, and it lets the fabricator price the board against the dielectric and copper weights that will actually be used.
Where the requirement is not written down, the shop supplies its own default, and the default is chosen for the process rather than for the design. The measurements that matter are the repeatable ones: conductor width and spacing, annular ring, finished hole size, plating thickness and surface finish are all verifiable on a coupon that travels with the panel.
Running a first article through the same checks as the production panel confirms that the two agree, and that comparison is the cheapest form of process control available at prototype stage.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
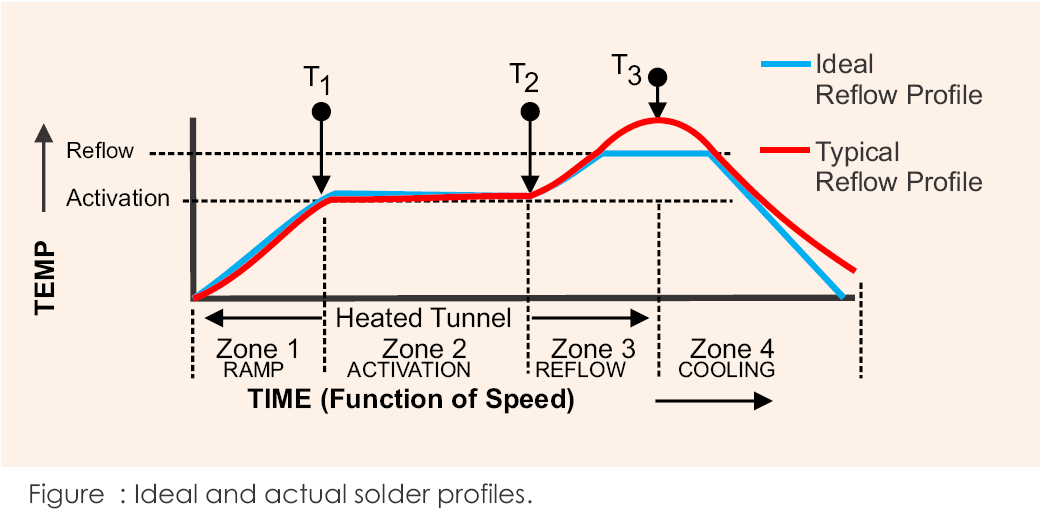
A parameter that is set once and never re verified drifts, and the drift is usually discovered by a defect rather than by the record. The tooling, the material and the profile form one system, and a change to any of them should be assessed against the other two before it is released.
Where the process window is narrow, the measurement resolution has to be better than the window, or the data cannot distinguish a good part from a marginal one. A record that identifies the operator, the date and the settings is worth more than a record that identifies only the result.
FAQ
Can X-ray confirm a good joint? It can confirm that the ball is present, round and free of large voids. It cannot confirm the interface on its own, which is where the destructive sample comes in.
Is 3D X-ray necessary? It is necessary where an oblique or stacked joint has to be resolved, and it is a cost that should be justified by the product.
What does gopcb provide for BGA inspection? We provide a reference sample set with documented defects, written criteria for ball diameter, shape and void, an oblique or computed tomography view where a two dimensional image is ambiguous, and a destructive microsection on a sample to confirm that the images are read correctly.