Board Handling and Packaging After Reflow
A board that has been through reflow is a finished assembly, and everything that happens to it afterwards either preserves or degrades it. Handling and packaging are the last chance to do that well.
Where the Damage Comes From
Flexing during handling, contact with a component, static discharge and moisture during storage are the four main sources. Each has a different control and each is easy to overlook at the end of a line.
The flexing damage is often invisible until a thermal cycle. Our strain notes describe the measurement.
Stacking and Board Support
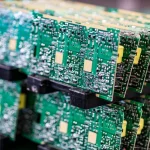
Stacking boards directly on each other puts the weight on the tallest component. Trays keep the boards apart and they should be used as soon as the assembly leaves the line.
Where boards are stacked, the load should be spread and the height limited. Our board support notes describe the deflection that results.
<img src="https://www.gopcba.com/wp-content/uploads/2024/10/HDI-PCB-min.jpg" alt="Boards in an ESD tray after reflow” />
ESD Control After Assembly
A populated board is more sensitive than a bare one because it carries devices. The trays, the bags and the work surfaces all belong to the same controlled area.
A board sliding in a plastic bag is a charge event. Our floor control notes describe the arrangement.
Moisture During Storage
A board that absorbs moisture releases it at the next reflow, which is where popcorning appears. The storage conditions and the duration should be stated for the assembly rather than for the components alone.
Where the storage life is exceeded, a bake is required before the next thermal step. Our bake schedule notes describe the cycle.
Labelling and Traceability
The label should identify the assembly, the revision, the lot and the date. A board separated from its label is a board that cannot be recalled.
The label has to survive the environment it will see. Our quality notes describe the acceptance that applies to it.
Shipping and Vibration
A package in transit sees vibration, and the response depends on how the boards are supported inside it. A large board supported only at the ends behaves differently from one in a fitted tray.
The packaging should be chosen with the transport in mind. Our vibration notes describe the test that confirms it.
Verification
The verification is a tray that separates boards, an ESD controlled area that continues past the line, a storage duration stated for the assembly, and a label that identifies the lot after the board has left the building.
Our fabrication notes list the points to confirm.
Process Control and Verification
Keeping a sample from the panel turns a dispute into a measurement, because the same coupon can be re-examined by both parties without rebuilding the batch. Reviewing the design before the data is released is cheaper than correcting it after the panel is in the tank, because every step downstream inherits the decision made at the front end.
Documenting the assumption is part of the design work, and a short note on the drawing prevents a question that would otherwise arrive a day later and cost a day of schedule. The process window is set by the narrowest step in the flow, so an improvement anywhere else shows up as margin rather than as yield until that step is addressed.
A short note on the drawing about handling, storage or packaging is often worth more than an extra decimal place on a tolerance. Where a value sits close to a process limit, the drawing should say so, since the shop can then open the process window rather than working to a nominal figure that carries no tolerance.
A stack-up that is drawn rather than described removes most of the ambiguity from a quotation, and it lets the fabricator price the board against the dielectric and copper weights that will actually be used. Where the requirement is not written down, the shop supplies its own default, and the default is chosen for the process rather than for the design.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
A parameter that is set once and never re verified drifts, and the drift is usually discovered by a defect rather than by the record. The tooling, the material and the profile form one system, and a change to any of them should be assessed against the other two before it is released.
Where the process window is narrow, the measurement resolution has to be better than the window, or the data cannot distinguish a good part from a marginal one. A record that identifies the operator, the date and the settings is worth more than a record that identifies only the result.
FAQ
Can boards be stacked without trays? Only where nothing protrudes and the load is small. In practice a tray costs less than the damage it prevents.
Does a sealed bag remove the moisture risk? A sealed bag with desiccant controls it for a stated period and it does not control it indefinitely.
What does gopcb provide after reflow? We provide ESD trays used as soon as the board leaves the line, a documented stacking limit, a storage duration stated for the assembly with a bake cycle if it is exceeded, and a label that carries the assembly, revision, lot and date through to shipment.