78-Layer PCB Backplanes: Where Manufacturing Meets Its Limit
A 78-layer PCB backplane is the product that shows where board manufacturing currently stops. Industry information published on 23 August 2026 described the next generation of orthogonal accelerator architecture, in which compute tray boards rise from twenty six to thirty layers, the number of interconnect switch trays doubles from nine to eighteen, and the orthogonal backplane reaches seventy eight layers by laminating three twenty six layer sections together, with line widths and spacing entering the twenty five micrometre range.
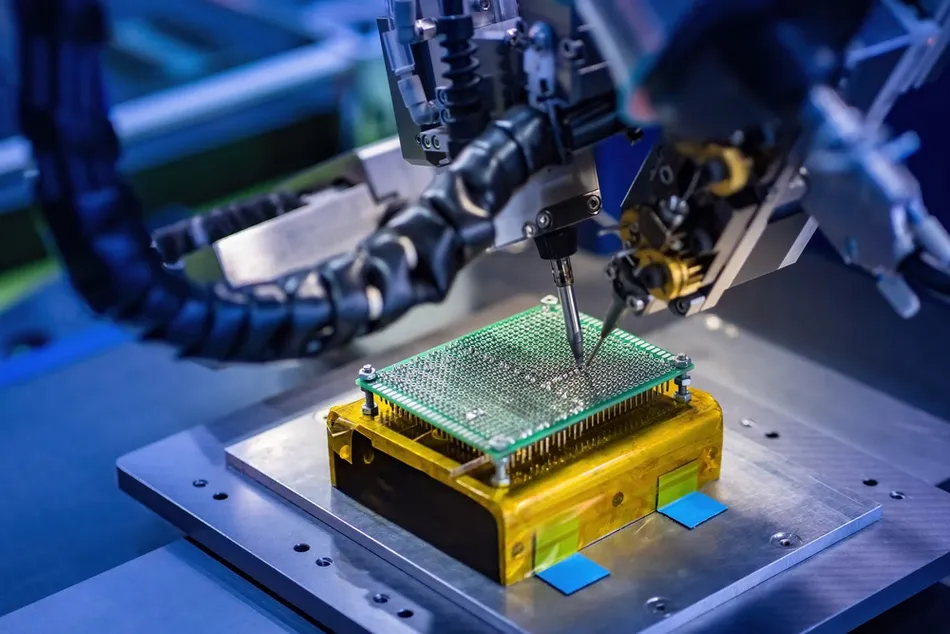
Samples had shown progress, but volume yield remained under pressure, and investment was accelerating in vertical continuous plating, three dimensional back drilling, combined drilling and inspection, and precision laser machining. Those process names indicate the direction: high end board manufacturing is moving toward the precision culture of semiconductor packaging rather than the tolerance culture of traditional fabrication.
Why Layer Count Is Not the Only Difficulty
Difficulty does not rise linearly with layers. Each lamination cycle introduces material movement, and the accumulated misregistration across many cycles determines whether a via lands inside its target pad. On a large backplane, a local misalignment can scrap a board that already contains an enormous amount of work.
Thickness adds to the problem. A seventy eight layer stack is physically deep, so drilling is high aspect ratio, plating must reach the centre of a long barrel, and layer to layer alignment has to hold across a panel whose dimensions change during processing. Every one of those steps has a tolerance that contributes to the final result.
Laminating Three Sections Together
Building seventy eight layers in a single sequence would be impractical, so the stack is produced as separate sections that are laminated afterwards into one board. This approach keeps each lamination cycle manageable, but it creates a new interface where the sections join.
Alignment between sections must be precise enough that vias crossing the boundary still hit their targets, and the joining lamination must not distort the sections already built. The process requires measurement and compensation at each stage rather than a single reference, and it is one of the reasons only a small number of factories can attempt this class of product.
Twenty Five Micrometre Features
Line width and spacing at twenty five micrometres is at the edge of what subtractive etching can achieve, because side etch consumes a significant part of the tolerance. Producing such features reliably requires modified semi-additive processing or equivalent techniques, together with imaging capable of resolving them across a large panel.
The combination of very fine lines and very high layer counts is what makes this product unusual. Fine lines are commonly produced on thin, small boards; high layer counts are commonly produced with coarser features. Delivering both on one large panel is where the manufacturing difficulty concentrates, and it is why yield rather than capability defines who can supply.
Plating Deep Holes
Plating a high aspect ratio hole requires the plating solution to reach the middle of the barrel and deposit copper evenly along its length. Vertical continuous plating improves distribution compared with older equipment, but the process still has to be controlled carefully to avoid thin deposits in the centre.
Thin plating shows up as a reliability problem rather than an immediate defect, since a barrel that is marginally thin may pass electrical test and fail later under thermal cycling. This is why plating thickness measurement and cross sectioning remain part of production control on very high layer count boards, even though they consume expensive panels.
Back Drilling at Depth
Back drilling removes the unused portion of a via so that it does not behave as a resonant stub at high frequency. On a thick board the depth control is demanding, because the drill must stop within a narrow window without touching the layers the signal uses.
The operation also consumes machine time, which limits throughput. Combined drilling and inspection aims to reduce the risk by verifying depth as part of the process rather than afterwards, and laser methods are being explored for precision work. All of these approaches are attempts to make a fundamentally difficult operation repeatable.
Consistency Across Thousands of Channels
A backplane carries thousands of high speed channels, and the system treats them as equivalent. That means impedance, loss and delay have to be consistent across the whole board, not merely correct on average, because a small number of outlying channels can limit the link.
Achieving that on a large panel requires uniformity of dielectric thickness, copper thickness and line geometry over an area where process conditions naturally vary. Manufacturers manage it by characterising the process across the panel, adjusting artwork to compensate, and measuring coupons at multiple positions rather than assuming homogeneity.
Material Behaviour Under Repeated Lamination
High performance laminates are used on these boards because the channels demand low loss, and those materials tend to be more sensitive to processing than FR-4. Repeated lamination cycles increase the accumulated movement and the risk of distortion.
Designers help by keeping copper balanced and by avoiding unnecessary asymmetry in the stack, since an unbalanced construction will move differently on each side when heated. This is a mechanical requirement with electrical consequences, and it is one of the places where layout and stack up decisions determine manufacturing feasibility.
Mechanical Stability of a Large Board
A backplane is large and thick, and it has to remain flat enough for connectors to mate and for assemblies to be installed. Warpage that would be invisible on a small board becomes a mechanical problem at this size.
Controlling it means balancing copper distribution, managing lamination pressure and cooling profiles, and measuring flatness as a production parameter. Mechanical support in the rack eventually helps, but the board has to arrive within tolerance, and that requirement is part of the fabrication specification rather than an assembly concern.
Yield Economics
When a single board contains seventy eight layers of material and a large panel of processing time, the cost of a scrapped unit is severe. Yield therefore dominates the economics of this product, and a factory that yields a few percentage points better can price more competitively despite identical equipment.
That is why process knowledge rather than capital expenditure defines capability here. It is also why buyers should ask about yield on comparable boards and about the corrective actions taken when a batch fails, since those answers reveal whether the process is understood or merely being pushed. It is the same discipline that process control is designed to enforce in less extreme products.
What Buyers Should Expect to Discuss
Programmes at this level involve the fabricator from the beginning, because the design and the process are developed together. Stack up, drilling strategy, back drilling depth and material combination all need agreement before artwork is released.
Buyers should also expect a longer qualification cycle, intermediate inspection points and a clear plan for what happens if the first build misses the yield target. Suppliers who can describe those stages in detail are demonstrating that they have built this class of product before, and that they understand the difference between a capability statement and a production plan.
Semiconductor-Like Manufacturing
The equipment and discipline required for these boards resemble the semiconductor industry more than traditional circuit fabrication: precision measurement, controlled environments, statistical process control and expensive panels that cannot be reworked.
That shift has implications beyond one product. As boards move closer to packaging in difficulty, the boundary between board making and packaging becomes less distinct, and the manufacturers who invest in precision processes will find their capability transferable to several product families rather than only to the largest backplanes.
Inspection When the Board Is Too Thick to See Through
Inspection is the quiet constraint on very high layer count work. A seventy eight layer board is more than ten millimetres thick, so optical inspection reaches only the outer layers and X-ray must carry the rest of the burden for buried vias, stacked microvias and inner layer registration.
That makes the inspection plan part of the design review rather than a downstream step. Coupons placed in the panel, test structures on each section and electrical continuity nets on every plane pair all give the factory a way to prove the interior is correct without cutting the board open.
For buyers, the practical question is whether the supplier can show data rather than promises. A capable factory will describe which measurements it takes, at which stage, and how it disposes of boards that fall outside the window, because on a board this size scrapping at final test is expensive for everyone.
Where the Limit Moves Next
Each architecture generation has raised the ceiling: sixteen layers, then thirty, forty, and now seventy eight with the largest boards assembled from sections. There is no reason to expect the progression to stop while bandwidth demand continues to rise.
What changes is the cost of each increment. Every step requires better registration, better plating and better measurement, so the number of factories able to participate shrinks as the frontier advances. For buyers that means a small supplier base and long lead times at the top end, and it makes early engagement with a capable manufacturer a strategic decision rather than a purchasing one, as reflected in the manufacturing process for such boards.