Multilayer PCB Manufacturing and Applications
A multilayer board carries three or more copper layers, separated by dielectric material and joined by plated holes. Each inner layer needs its own artwork, its own etch step and its own registration check. The finished board then passes through lamination, drilling, plating and outer-layer processing before it ships. This review follows the work from stack-up planning to final test, so buyers and engineers can see where cost and risk actually sit.
Most design teams reach for a multilayer structure when two layers run out of routing space. A four-layer board can dedicate inner layers to power and ground, which frees the outer layers for components and short signal runs. That change alone can cut noise and simplify layout. The tradeoff is a longer process chain and tighter tolerances at every step. Knowing that chain helps a buyer read a quotation and ask better questions.
Stackup Choices
The stack-up is the first real decision, and it should be fixed before routing starts. Engineers assign signal, power, ground and dielectric layers according to the electrical needs of the product. Symmetry matters because an unbalanced build can warp during lamination. Copper weight and dielectric thickness set the impedance targets that the fabricator must hold. A stack-up agreed early prevents expensive rework later, when traces are already drawn.
Material selection follows the stack-up. Standard FR-4 suits many general-purpose boards and keeps cost predictable. High-Tg laminate may be needed where the assembly sees repeated thermal cycles. High-frequency, low-loss materials enter when signal speeds demand tighter dielectric control. Each step up in material class adds cost and often adds lead time. The right choice is the one that meets the application without paying for margin nothing uses.
Symmetry deserves a closer look because it drives both yield and flatness. A build with heavy copper on one side and light copper on the other cures at different rates, so the panel can bow after cooling. Fabricators often balance copper distribution and adjust prepreg flow to compensate. Buyers should ask whether the proposed stack is symmetrical and how the factory handles copper balance. The answer explains why a cheaper stack sometimes costs more in scrap and rework.
Inner Layer Fabrication
Inner-layer work starts with imaging and etching. The circuit pattern is transferred onto copper and the unwanted metal is removed. Each panel must match the Gerber data, so the film or direct-imaging tool is checked against the design before the lot runs. Line width and spacing are measured, because a small drift here changes impedance and can cause opens. Good fabricators record these readings per panel, not per batch.
Registration is the quiet risk on inner layers. Every layer carries targets that let the next process align it to the others. If those targets drift, the drilled holes may miss the pads after lamination. The defect appears late, when the board is already built. That is why inner-layer inspection matters more than its cost suggests. A quick check at this stage protects the whole lot.
Etch compensation is another detail that separates a careful fabricator from a rushed one. Acid etching removes copper sideways as well as downward, so a trace drawn at the target width comes out thinner. The CAM team adds a small allowance to offset that loss. On fine lines the allowance is tight, and an error shows up as an open or a weak trace. Ask how the factory verifies finished line width after etch.
Lamination Control
Lamination bonds the inner layers, prepreg and copper foil into one solid panel. Temperature, pressure and time must follow a qualified cycle for the material in use. Prepreg has a shelf life and absorbs moisture, so storage and handling affect the result. Voids, resin starvation and delamination are the failures to watch. Each one can pass a visual check and still fail in the field.
Alignment during lamination decides whether vias land correctly. Small shifts multiply as layer count rises, so a six-layer board is less forgiving than a four-layer one. Fabricators use registration coupons and X-ray checks to confirm the stack. Buyers should ask how layer-to-layer registration is verified, especially on fine-pitch designs. The answer tells you more than a capability chart does.
Moisture control starts before the press. Prepreg that has absorbed water can flash to steam under heat and leave voids or measle-like spots between layers. Factories dry material and track humidity in the lay-up room for that reason. A press cycle that looks correct on paper still fails if the prepreg was stored badly. Buyers touring a plant should look at how prepreg is sealed, labeled and rotated through stock.
Drilling and Plating
After lamination, the panel is drilled to create interconnections. Mechanical drilling handles through holes, while laser drilling opens microvias in HDI builds. Hole position, diameter and wall quality all affect reliability. A rough wall or a smear of resin can break the connection after plating. Drill parameters are set per material and per stack, so a change in laminate means a new recipe.
Plating then deposits copper inside the holes and on the surface. The goal is consistent thickness through the barrel and on the surface copper. Thin plating in a deep hole can crack under thermal stress. Thick plating can close small holes and slow etching. Control charts on plating thickness are a useful signal of process health. Ask for them when the board carries fine vias or high layer counts.
Resin smear is the classic drilling failure on multilayer boards. Heat from the bit softens resin, which smears across the copper target and blocks the connection. Desmear chemistry removes it before plating, and the process must be matched to the resin system. A board can pass continuity test and still have a weak barrel that fails after thermal cycling. Buyers should confirm that desmear and barrel inspection are part of the standard flow.
Outer Layers and Finish
Outer-layer imaging and etching form the final traces, pads and features. Line width and copper thickness must match the design, because both affect current capacity and impedance. Solder mask is then applied to protect copper and prevent bridging during assembly. Mask alignment on dense boards is a real challenge. Misregistration can expose a pad edge or cover a test point.
Surface finish protects exposed pads and decides how well solder wets during assembly. HASL, ENIG, immersion silver and immersion tin each suit different needs and budgets. The choice should match the assembly process and the storage life of the board. A finish that is wrong for the application can cause joint defects that appear only at reflow. Confirm the finish in writing before the order is released.
Finish thickness is worth specifying, not just finish type. Thin ENIG can leave nickel exposed and cause solderability problems after storage. Thick gold adds cost with little benefit for a board that will be assembled quickly. Immersion silver tarnishes if packaging and storage are poor, which changes wetting behavior. Buyers should ask how the factory measures finish thickness and how it packs boards for shipment.
Design Choices That Affect Yield
Layout decisions made early show up later as yield. Dedicated power and ground planes give signals a short return path and reduce noise. Controlled impedance traces need a continuous reference plane beneath them. A split plane under a high-speed trace forces the return current to detour, which radiates energy. Designers should check every plane boundary against the signals that cross it.
Via design is another lever. Through holes are cheap and reliable, while blind and buried vias save space at extra process cost. Each via adds a stub that can affect high-speed signals. Thermal vias help move heat away from power components. Trace spacing must satisfy voltage and crosstalk needs at the same time. These choices belong in a design review before tooling begins.
Even though the annular ring is small, it has a big influence on yield. The ring is the copper left around a drilled hole, and it must survive drill tolerance and registration shift. A tight ring saves space but raises the chance of a breakout after drilling. Designers should confirm the ring against the fabricator’s drill capability rather than against a generic rule. That check prevents a design that routes well but cannot be built at volume.
Applications and Test Coverage
Multilayer boards appear wherever density and signal quality matter. Routers, switches and wireless equipment rely on controlled impedance and clean power delivery. Servers and storage systems need many layers to route dense buses. Medical, industrial and automotive products add reliability demands on top of density. Consumer devices push miniaturization furthest. In each case, the stack-up and finish should follow the environment the board will see.
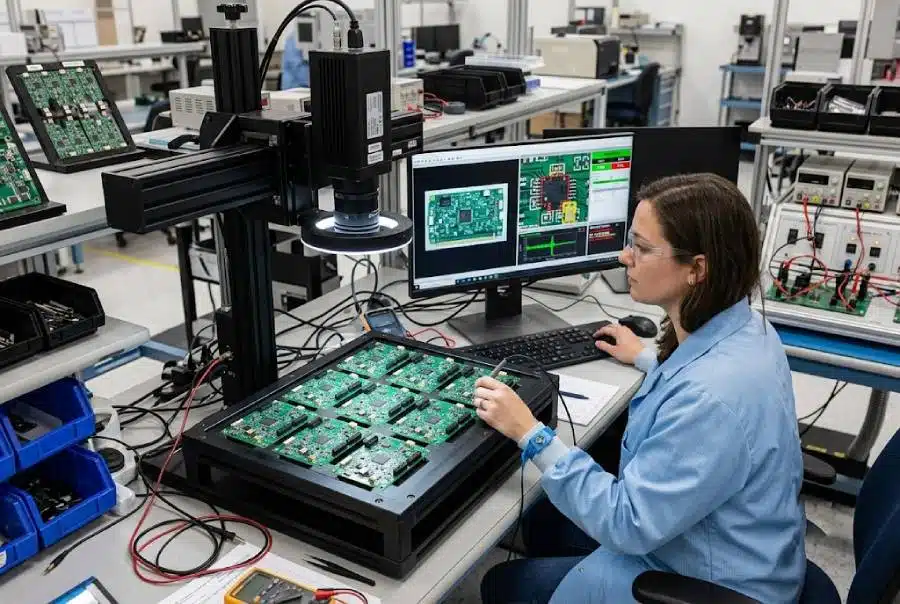
Testing closes the loop. Electrical test verifies continuity and isolation on every net, and it catches opens and shorts before assembly. Automated optical inspection finds surface defects, while X-ray checks hidden joints and via quality. For complex builds, PCBA testing adds in-circuit and functional coverage after assembly. Buyers should confirm which tests run on every lot and which run only on the first article.
Test coverage has limits that buyers should understand. A flying-probe or bed-of-nails test confirms that nets connect as drawn, but it cannot prove that a barrel will survive years of thermal cycling. Coupon testing and microsectioning answer that question, and they are usually sampled rather than run on every board. Ask which reliability checks apply to your build and how often they run. That tells you what the test report actually covers.
Assembly is where the board meets its components. SMT PCB assembly places and reflows fine-pitch parts, and the pad finish and mask alignment from fabrication directly affect joint quality. Early samples reveal pad geometry problems before volume commitment. That is why rapid PCBA prototyping is worth using on new designs. A small pilot lot teaches more than any quotation can about process behavior.
Buying and Verification
Comparing suppliers on unit price alone hides the real cost. Ask about layer-count range, minimum trace and spacing, via capability and impedance control. Confirm the material grades the factory stocks and how it qualifies them. Check whether engineering review happens before tooling, because a question answered early is cheap. Also confirm the test plan and the records that ship with the boards.
Quality records should travel with each lot. Process sheets, plating data and test reports let you trace a field return back to its cause. A supplier with a working quality management system can produce these on request. Full-service partners can also handle PCB assembly after fabrication, which keeps one set of records for the whole build. Verify the scope in writing before you release the order.
The practical takeaway is simple. Fix the stack-up and finish before routing, confirm the fabricator can hold them, and require test records with every lot. Review first-article data against the drawing rather than against a summary. Those steps cost little at the start and prevent the expensive surprises that appear after volume production begins.