PCB Fiducial Checklist: What to Check
Fiducials are small copper or solder-mask-free marks that the placement machine uses to find the board. They cost almost nothing to add at layout, yet a missing or poorly placed mark can stop a whole SMT line. This checklist covers what to verify before you release files, what to ask a supplier, and how fiducial quality shows up in placement accuracy and yield. The goal is a short review that prevents expensive rework later.
Many quality problems blamed on the machine actually start in the CAD data. A fiducial covered by solder mask, placed too close to a panel edge, or hidden under a component gives the vision system nothing reliable to lock onto. Engineers should treat these marks as critical features, not as decoration added at the end. Buyers should confirm that the factory checks them before tooling, because fixing a panel after stencils and programs exist costs far more than a file change.
Role of Fiducials in Placement
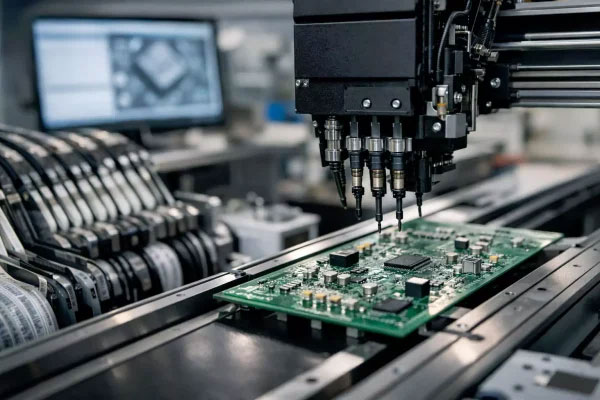
The placement machine measures board position by locating fiducials with a camera. It compares the measured position with the programmed position and shifts the placement coordinates to match. This correction absorbs small errors from panel routing, copper etching and conveyor loading. Without a reliable mark, the machine places components at nominal coordinates and any board shift becomes a placement offset. That offset may pass on one edge and fail on the other, which makes the defect hard to trace.
Global fiducials sit outside the board array and align the whole panel. Local fiducials sit near fine-pitch parts and correct for local distortion across a large board. Both types serve the same purpose at different scales. A panel with only global marks can still show drift at the far corner after reflow expansion. Engineers should decide which level the design needs based on board size, component pitch and panel layout. This decision belongs in the DFM review, not on the line.
Geometry and Contrast Rules
A useful fiducial needs a clear optical contrast against its surroundings. The common approach is a round copper pad with an open area of solder mask around it, so the camera sees a bright circle on a darker field. The pad should be flat and free of plating bumps, because a domed surface reflects light unevenly. The clearance ring must be wide enough that nearby traces or mask edges do not enter the camera window. Check that no silkscreen, via or test point touches the mark.
Size and shape should stay consistent across the panel. Mixing round and square marks, or pads of different diameters, confuses some vision algorithms and slows teaching. Keep the same diameter for all global marks and the same smaller diameter for local marks. Place at least three global marks, ideally at asymmetric positions, so the machine can detect rotation as well as translation. A symmetric pattern can allow a flipped board to align wrongly, which is a costly mistake to catch late.
Placement and Clearance Checks
Distance from the board edge matters. A mark placed too close to the routed edge can be partly removed by the router bit or covered by panel burrs. Keep a margin that survives the full routing tolerance, not just the nominal cut line. The same rule applies near breakaway tabs and V-score lines, where stress and debris gather. Verify the final panel drawing, because the CAD board outline is not the same as the production array.
Component clearance is equally important. A tall part placed next to a fiducial can shadow the camera or block the head during teaching. Keep the area around each mark free of components on both sides where possible. For double-sided boards, confirm that marks on the bottom side are not covered by parts from the top assembly. These details are easy to miss in a dense layout, so a simple visual check of the panel image catches most of them.
Panelization and Tooling Effects
Panel design changes how fiducials behave. A panel with many small boards may need marks on the panel frame rather than on every board, because individual marks become too small to resolve. Conversely, a large board with fine-pitch devices may need local marks in addition to the panel marks. The right balance depends on the array, the machine and the component mix. Ask the factory to confirm the choice against their equipment rather than assuming one pattern fits every job.
Tooling holes and panel edges also affect alignment. If the panel is located by tooling pins, the fiducials correct the remaining error, so both systems should agree. A panel that fits loosely on the pins will move between print and placement, and no mark can fix that. Review the panel drawing together with the assembly drawing, and confirm that the marks stay visible after printing, reflow and any coating step. Coating over a mark is a common cause of alignment failure on later runs.
Inspection and Test Coverage
Fiducial quality should be confirmed at first article, not assumed. The operator teaches the marks, runs a sample board and checks placement accuracy across the panel. If the machine struggles to find a mark, that is a design signal, not a machine fault. Record which marks were used and what offset was applied. These records help when a new batch behaves differently, because they show whether the panel or the process changed. Structured PCBA testing then confirms that the placed parts actually work.
Inspection data closes the loop. If placement offsets appear at one corner, the engineer can check whether the local mark was damaged or covered. If offsets appear across the whole panel, the global marks or the panel location are suspect. Factories that log this data find the cause quickly, while factories without records repeat the same adjustment. Buyers should ask for the first-article report and confirm that fiducial teaching is part of it. That single document reveals more about process discipline than a factory tour.
Supplier Questions and Records
Ask the supplier how they handle missing or weak fiducials before the order starts. A good answer describes a DFM flag, a recommended fix and a re-check after the change. A weak answer suggests the line will improvise, which usually means slower setup and higher risk. Confirm that the factory reviews the panel drawing and the Gerber data together, because marks sometimes exist in one file and not the other. This review costs little and prevents a stoppage at the printer.
Records should travel with the lot. The program version, the marks used, the offset applied and the inspection result all belong in the batch file. When a field return arrives months later, that record shows whether placement was ever in question. Buyers who request these documents as routine get a clearer picture of how the line is run. A supplier with a real quality management system can produce them without effort, while one without records will struggle to explain a defect.
Prototype to Volume Transition
Prototypes are the cheapest place to test fiducial choices. A small batch reveals whether the marks are visible after reflow, whether the panel locates cleanly and whether the machine teaches them without error. Rapid PCBA prototyping lets engineers compare two mark layouts before committing to volume tooling. Fixing a mark in CAD takes minutes, while fixing it after stencils and programs are built takes days. Treat the pilot run as a design check, not just a sample delivery.
When the design moves to volume, the same marks must survive a busier line. Faster changeovers and tighter schedules leave less room for manual adjustment, so reliable marks matter more. Confirm that the panel array, the mark pattern and the machine program are frozen before the first large order. Any later change should be reviewed against its effect on placement accuracy. High-volume PCB assembly rewards this discipline, because a stable setup keeps yield steady across shifts and product mixes.
Working With an Assembly Partner
Most product companies do not run their own SMT line, so the partner’s habits decide the outcome. A partner that reviews fiducials at quotation, flags weak marks and records the teaching result brings discipline to every program. A partner that accepts files without comment shifts the risk back to the buyer. Ask how the factory handles a board with no marks at all, and listen for a concrete process answer. The reply tells you how the line behaves when something is missing.
Process control should be visible in the documents, not only in the brochure. A written specification for mark size, clearance and panel location removes guesswork at setup. SMT PCB assembly depends on this consistency, because every program is taught against the same rules. Buyers comparing suppliers should request a sample first-article report and check whether fiducial teaching appears in it. That simple check separates factories that plan from factories that react.
The takeaway is practical. Add clear, flat, unobstructed fiducials at layout, keep the pattern consistent, and confirm them at first article. Ask the supplier to review the panel drawing before tooling and to keep the teaching record with the lot. These steps cost almost nothing and protect placement accuracy through every batch. When files are ready, send them for a DFM review and confirm the mark pattern in writing before the first panel is built.