PCB Sampling Plan Handover: Passing It On
A sampling plan only works when the next team can read it and run it. Handover means the settings, the material records and the open questions travel with the job. Too often the plan lives in one engineer’s notebook and leaves when that engineer does. This guide explains what a clean handover contains and what a buyer should verify before signing off a program.
The handover sits between the pilot run and volume production. At that point the process has a proven setup, but the evidence is scattered across print reports, oven profiles and inspection logs. Collecting it into one package is the whole task. When the package is complete, a second line or a second shift can repeat the result without guesswork. When it is thin, every later batch becomes an experiment.
What Handover Really Covers
Handover is not a single document. It is a bundle that describes the state of the process at a fixed moment. That bundle includes the approved stencil design, the paste type and storage conditions, the placement programs and the reflow profile. It also lists the inspection criteria and the test coverage agreed for the product. Each item must be traceable to a revision, so nobody runs an old program by mistake.
The bundle also carries the open points. Every build raises questions that were answered verbally or left for later. A good handover writes those down with an owner and a date. A pad that looked marginal, a component with a long lead time, a profile that ran close to its window: all belong in the record. The next team inherits the risk only if nobody wrote it down.
Where the Trouble Starts
Most handover failures begin earlier than the handover itself. A parameter was tuned on the line and never written into the setup sheet. A paste batch was swapped without updating the record. An operator adjusted a profile to clear one defect and the change stayed. None of these acts is unusual, and each one breaks the link between the proven run and the next one.
The second common cause is a gap in ownership. The engineer who built the sampling plan moves to another project, and no one is named to receive the package. Files sit on a shared drive with names that mean nothing to the new owner. Weeks later, production starts from a best guess. A named sender and a named receiver, with a review meeting between them, remove most of this risk.
Building the Package
Start with the design data. The approved Gerber files, the fabrication drawing and the assembly drawing form the base. Add the bill of materials with approved alternates marked clearly. Any deviation approved during the pilot run should be attached to the exact revision it affects. This keeps the design intent visible to everyone who touches the job, and it supports the review covered under PCB design and layout.
Next, record the process settings as they were established. Print speed, squeegee pressure, stencil cleaning frequency and separation speed belong in the record. So do the placement programs, feeder positions and nozzle types. The reflow profile should appear as a chart with the measured thermocouple data, not as a generic curve. The next run then starts from a known point instead of a memory.
Material Traceability
Materials change quietly and shift the process with them. Record the paste lot, the component date codes and the storage history for moisture sensitive parts. Note any approved substitute and the condition under which it may be used. When a field return arrives months later, this record is the fastest route to the cause. Buyers should ask for it as a routine part of every order.
Running the Process as One Chain
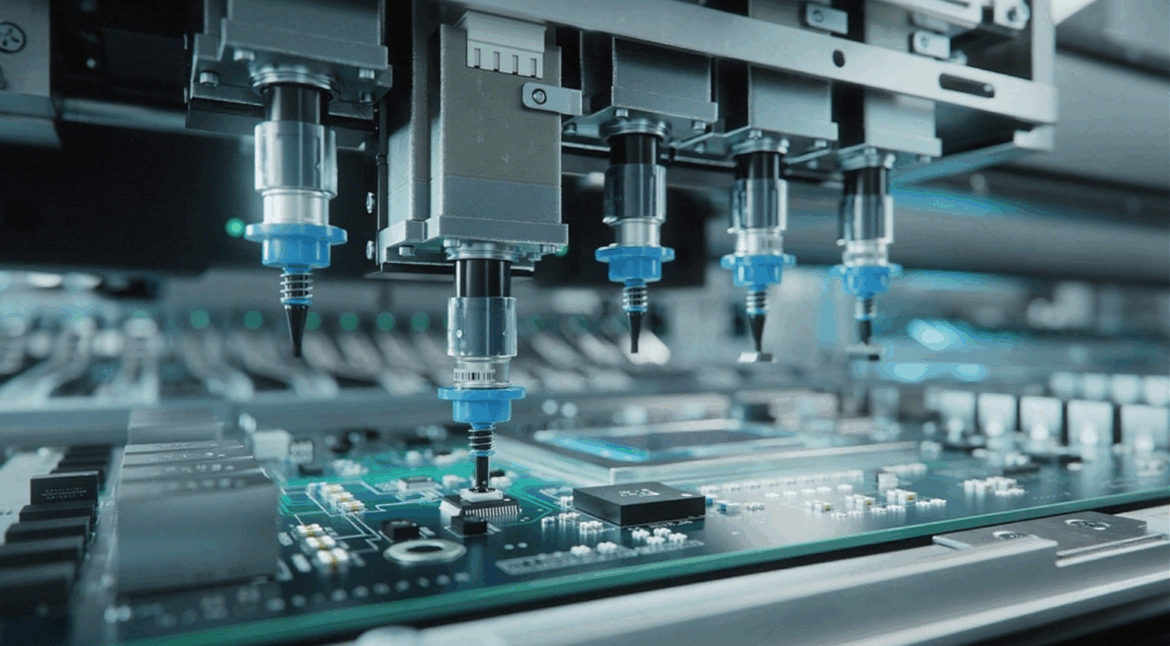
The result depends on the whole chain, not on any single machine. The board design fixes pad sizes and spacing, the printer controls solder volume, the placement machine positions each part and the oven forms the joints. Each step feeds the next, which is why SMT PCB assembly should be reviewed as one process rather than a set of separate operations. A change at one station shows up three stations later.
Pair that view with PCB assembly records so the team shares one reference for every change. A stencil tweak, a new component or a faster placement speed should each be checked against its effect on the rest. A faster placer may save cycle time today and create tombstoning tomorrow. A thicker stencil may fix opens while causing bridges. The handover package is where those tradeoffs are written down.
Checks That Hold Yield Steady
Inspection stops defects from leaving the factory, yet the feedback it provides is where its real worth lies. When a joint fails, the engineer learns whether the paste print, the placement or the profile caused it. Month after month, defect rates fall because inspection and process control are linked in that loop. Solder paste inspection and automated optical inspection should feed the same data set the handover package describes.
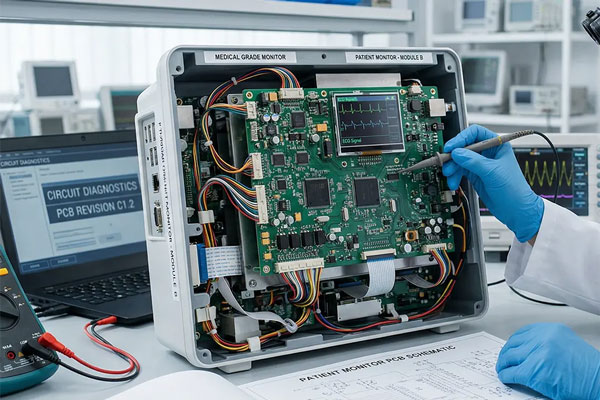
Boards that pass visual checks still need electrical verification. A cracked joint or a wrong component often shows up only under power. Functional test, in-circuit test and burn in each add confidence, and a structured PCBA testing program ties them together. The handover should state which tests run on every board and which run on a sample. It should also name the pass and fail limits, so the next team applies the same judgment.
Documentation and Traceability
Documentation matters as much as hardware. The factory should record which program ran, which reels of paste and components were used, and which operator handled the batch. It should also record what inspection found and what was done about it. When a field return arrives, that record identifies the cause quickly and proves the fix reached the next batch.
During production, records that can be readily provided when asked tend to be maintained truthfully. Ask for them before you need them. A supplier who can show a complete batch record for a recent order is likely to keep the same discipline on yours. A supplier who promises records but cannot show one has not built the habit yet. This check costs a conversation and tells you more than a brochure.
Training and Supplier Control
Every person touching the process needs training, and that rule applies fully to the handover. Before operators make any adjustment to a parameter window, they must understand the reason it exists. On this board, inspectors need to be able to recognize how an actual defect appears. Engineers must be able to explain any change that is observed in the data. It is the knowledge held by people on the floor that converts written procedures into everyday practice.
Suppliers and materials carry risks of their own. Even without any machine warning, the process can shift because of a component’s plating change, a paste batch’s viscosity difference, or a reel kept in humidity. Professional factories qualify their materials, review certificates of analysis, and approve alternates before they are needed. A supply change then stays a planned event rather than becoming a quality incident on the line.
Build In-House or Outsource
A dedicated line only pays for itself when it runs constantly. Keeping process data, calibration records and quality documentation current takes engineering time that is easy to underestimate. Most product companies therefore choose a partner that spreads its equipment over many customers. Services such as turnkey PCB assembly place fabrication, sourcing and assembly under one roof, which simplifies the handover because one team owns the whole chain.
When comparing factories, price per board should never be the only number. The actual cost is determined by process controls, inspection equipment, component sourcing, and communication. A partner that reviews files before production, reports risks honestly and keeps delivery promises will be cheaper over a program than one that quotes low and surprises later. Ask for defect data, test coverage and references, and confirm the quality plan in writing before you commit.
What to Verify Before Sign-Off
Before you accept a handover, check that the package names a revision for every document. Confirm that the process settings match the run that produced the approved samples. Look for measured profile data rather than a generic curve. Check that open points carry an owner and a date. Finally, confirm that the receiving team has read the package and can explain the key parameters back to you.
The lesson worth keeping is that handover rewards preparation. At the outset, defined data, a settled tolerance, a validated first article and documentation are inexpensive, yet they yield large savings afterward. Rework or a field return costs far more than the review that would have prevented it. Treat the package as part of the project schedule, not as paperwork after it.