PCB Sampling Plan Selection: Choosing What Fits
Sampling decisions rarely fail because the statistics are wrong. They fail because the plan does not match the process it is meant to monitor. A sampling plan sets how many boards are pulled, what each sample is checked for, and what happens when a result falls outside the limit. Get those three parts aligned with the actual build, and the plan becomes a working tool rather than a document filed at audit time.
The choice depends on defect history, lot size, inspection cost and the consequence of a missed fault. A mature product with stable yield needs less attention than a new assembly with unproven joints. This guide explains how to match the plan to the product, how to read the results, and what a buyer should verify before approving it. The aim is a plan that catches drift early without adding cost that nothing uses.
What a Sampling Plan Decides
A sampling plan answers a narrow question. Given a lot of boards, how many do you inspect, and how many failures make you reject the lot? The answer sits between two extremes. Inspect everything and you pay for certainty on a process that may already be stable. Inspect almost nothing and you accept risk you cannot measure. The plan is the negotiated middle, and it should be written down before the first panel is printed.
The plan also fixes the acceptance number, which is the count of defects allowed before the lot is held. That number is not a target. It is a trigger. When a lot reaches it, production stops and the cause is investigated. Engineers should treat the acceptance number as a signal about process health, not as permission to ship a known number of bad boards. That distinction matters when a supplier reports results.
Reading the Process First
Before choosing sample sizes, look at what the line can actually hold. Solder paste volume, placement accuracy, reflow profile and inspection limits each contribute to the final result. A process with tight control on all four can run a lighter plan. A process with known variation in one area needs sampling that targets that area directly. The plan follows the process, not the other way around.
Historical data is the honest starting point. If the last ten lots showed a stable defect pattern, the plan can reflect that pattern. If defects cluster around one component type or one pad geometry, the sample should include those features deliberately. Random sampling alone can miss a repeatable fault, because the fault is not random. Good plans combine random pulls with targeted checks on known risk points.
Sample Size and Lot Risk
Larger lots carry more risk per accepted defect, so the plan has to scale with quantity. A small pilot batch can be inspected heavily at modest cost, because the total number of boards is low. A high-volume run cannot afford the same intensity, so the plan shifts toward process monitoring and periodic pulls. The tradeoff is real, and it should be stated openly in the quotation rather than discovered later.
Buyers moving toward high-volume PCB assembly should ask how the plan changes as volume grows. A plan that works at one hundred boards may be too heavy or too light at ten thousand. The supplier should be able to explain the shift, name the inspection stages, and show the records that prove the plan ran as written. A plan nobody can demonstrate is only a promise.
Matching Checks to Defect Types
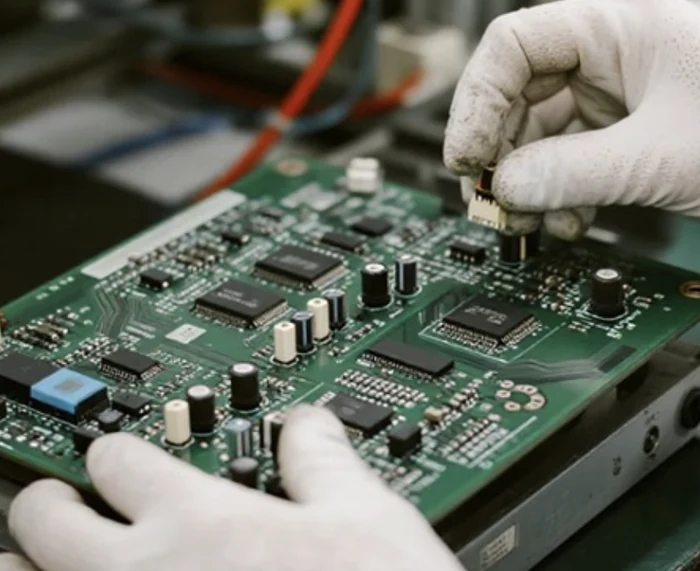
Not every check belongs in every sample. Visual inspection catches missing parts, wrong orientation and obvious solder defects. Automated optical inspection catches finer geometry issues at speed. Electrical test proves connectivity and function. Each method answers a different question, so the plan should assign each sample to the method that answers the question it needs answered.
Functional failures often hide behind passing visual checks. A cracked joint or a wrong component value may look correct and still fail under power. That is why the sampling plan should include electrical verification on a defined share of boards, not only on the first article. The split between visual, optical and electrical checks is a design decision, and it should be justified by the defect history of the product family.
First Article and Ongoing Samples
The first article sits outside the sampling plan in one sense and inside it in another. The first board is checked in full against the design, so it confirms the setup rather than estimating lot quality. Once the setup is proven, ongoing samples estimate whether the process still holds. Confusing these two roles is a common mistake, and it leads to plans that either over-inspect the first board or under-inspect the run.
A clear first article report should list component values, orientation, polarity and solder quality. It should also record the machine programs and settings used. When the ongoing plan later flags a defect, that report is the baseline for comparison. Without it, engineers cannot tell whether the process drifted or the setup was wrong from the start. The first article protects the whole batch from inheriting a setup error.
Records That Support the Plan
Sampling produces data, and data is only useful if it is kept. The factory should record which program ran, which paste and component reels were used, which operator handled the job and what inspection found. That record offers the quickest way to find the cause when a field return comes in months later. It also shows whether a corrective action reached the next batch or stopped at the report.
A documented quality management system turns these records into routine practice rather than a response to complaints. Buyers should ask for sample results as a normal part of every order. Records that are easy to produce on request are usually kept honestly during production. Records that appear only after a problem are a warning sign worth noting during supplier comparison.
Reaction When a Sample Fails
The value of a sampling plan depends on what happens after a failure. A failed sample should trigger a defined sequence: hold the lot, identify the defect type, trace it to a process step, correct the step and re-inspect before release. If the sequence is vague, the plan becomes a scorecard with no consequence. Engineers should confirm the sequence in writing before production starts.
Repeat failures deserve a different response from single ones. One isolated defect may point to a handling issue. The same defect appearing across consecutive lots points to a process cause that sampling alone will not fix. At that point the plan should shift from detection to investigation, with the acceptance criteria tightened until the root cause is removed and the data confirms the fix.
Buyer Checks Before Approval
Before approving a plan, confirm the sample size, the acceptance number, the inspection methods and the reaction sequence. Ask how the plan changes with lot size and how results are reported. Request a sample report so you can see the format and the level of detail. These questions cost little now and prevent disputes later, when a rejected lot or a field return forces both sides to reconstruct what happened.
Design data also feeds the plan. Pad geometry and spacing set the risk profile that sampling must cover, so the review should start with PCB design and layout. Component sourcing affects risk too, because a part from an unqualified source can shift the process without warning. Linking the plan to component procurement controls keeps material changes visible before they reach the line.
Most product companies build through a partner rather than in house. The equipment investment is large, and the engineering time to keep process data current is easy to underestimate. A partner spreads that cost across many programs and brings the same discipline to each one. Services such as turnkey PCB assembly can cover fabrication, assembly and test under one roof, which keeps the sampling plan consistent from lot to lot.
The practical takeaway is simple. Write the plan around the process you have, tie each check to a defect type, and define the reaction before the first lot ships. Review the results monthly and adjust the sample size as the data justifies. A plan that is reviewed and revised stays useful. A plan copied from a template and never revisited becomes paperwork that protects nobody and hides the drift it was meant to catch.