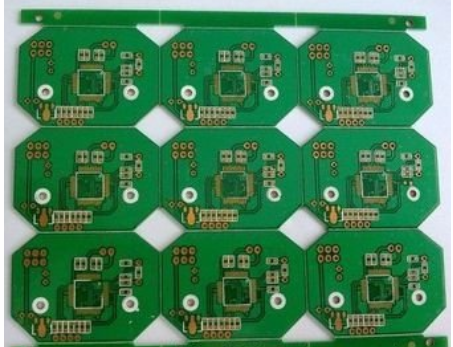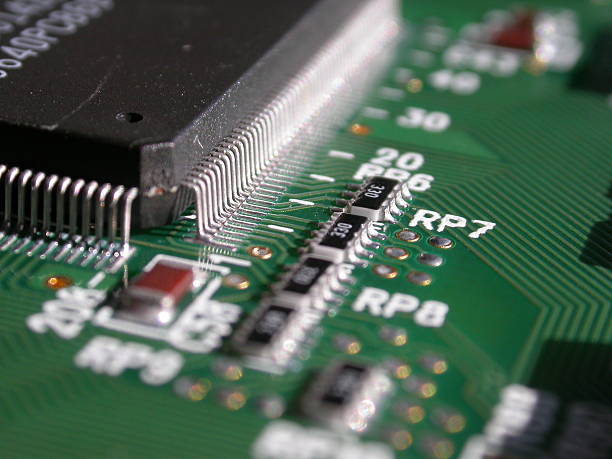
RF PCB Manufacturing for Wireless and Radar Systems
Wireless links and radar front ends share one demand: the board must carry a signal without distorting it. A small change in dielectric thickness or copper width shifts impedance, and the loss shows up as reduced range or a noisy return. This is why RF work is judged on process control rather than on equipment lists. The sections below explain how a build is planned, where yield is lost, and what a buyer should verify before release.
RF boards differ from digital boards in one practical way. The trace is not just a connection; it is an electrical element whose behavior depends on geometry and material. Every process step that alters width, thickness or dielectric spacing changes that behavior. Engineers and buyers therefore need a shared set of measured limits, not a general promise of quality. The discussion that follows stays on the decisions that actually move performance.
Signal Behavior Drives the Stackup
Controlled impedance starts with the stackup, not with the etcher. The designer sets trace width, dielectric height and copper weight so the target impedance can be reached with the chosen material. The fabricator then has to hold those values within a window across the panel. If the stackup is chosen for cost alone, the process window narrows and every later step becomes harder to control.
Material choice follows frequency and environment. Low-loss laminates reduce attenuation at high frequency, but they often behave differently during drilling and lamination. Standard FR-4 costs less and works for many lower-frequency designs. The tradeoff is real, and it should be settled with loss data and thermal requirements in hand. Choosing the most expensive laminate by default is not engineering.
Grounding and return paths belong in the same review. A well-chosen material cannot rescue a layout with broken return paths or long stubs. The fabricator can only build what the artwork defines, so stackup, routing and ground plane decisions should be reviewed together. This is where PCB design and layout work and fabrication planning meet.
Fabrication Control on the Floor
Line width and spacing must be held across the whole panel, not just at the center. Imaging, etching and plating all affect the final geometry, and each step has its own drift. A fabricator that measures test coupons on every lot can see that drift before it reaches the customer. Coupons are the cheapest early warning available in an RF build.
Copper thickness affects both loss and impedance. Plating variation between panels or between areas of one panel changes the cross section of the trace. The same applies to dielectric thickness after lamination. Press pressure, heat ramp and flow all influence the final spacing between layers. These are process variables, and they need recorded targets rather than operator judgment.
Via structures add another layer of risk. Blind and buried vias help density, but they demand tight control of hole position, wall quality and plating. A rough hole wall or uneven plating raises insertion loss and can create reflections. Drilling parameters should be qualified on the actual laminate, because a recipe proven on FR-4 may not transfer cleanly to a low-loss material.
Surface Finish and Solderability
Surface finish protects the copper and sets contact behavior. ENIG gives a flat surface and good shelf life, which suits fine-pitch components and many RF interfaces. Hard gold plating offers wear resistance where connectors mate repeatedly. Each option has cost and process implications, and the choice should match the mating cycles and storage conditions of the product.
Finish quality also affects assembly yield. Thin or porous nickel under gold can cause solderability problems later, and contamination on pads shows up as poor wetting. A fabricator that controls the plating bath and inspects coupons catches these issues early. Buyers should ask which finish was specified and how it was verified, not simply accept a default.
Once the bare board is accepted, assembly introduces its own variables. Paste volume, placement accuracy and reflow profile all influence joints on high-frequency connectors and small passives. For mixed RF and digital boards, SMT PCB assembly planning should begin while the bare board is still in fabrication, so stencil and panel decisions support both stages.
Test Coverage That Means Something
Electrical test for RF boards goes beyond continuity. Insertion loss, return loss and characteristic impedance are the parameters that describe real performance, and they need suitable fixtures and calibration. A vector network analyzer is only useful when the test setup is stable and the reference planes are known. Without that discipline, the data looks precise but means little.
Physical checks support the electrical results. Material thickness, copper adhesion, board flatness and dimensional accuracy all influence how the finished board behaves in a housing. Flatness matters especially for radar modules, where a slight warp can change antenna spacing. These checks are inexpensive and should be routine on every lot.
Environmental testing answers a different question. Temperature cycling, humidity exposure and vibration simulate the conditions a wireless or radar unit meets in service. The results show whether the design and the process hold together over time. A structured PCBA testing plan ties electrical, physical and environmental checks into one record set for each build.
Matching the Build to the Application
Wireless infrastructure boards usually prioritize signal integrity and channel isolation. Dense routing and multiple antennas make crosstalk control important, and the stackup must support consistent impedance across many traces. Automotive radar boards add thermal and vibration requirements, so material choice and via reliability carry more weight. The same fabricator may build both, but the process settings differ.
Satellite and navigation equipment pushes accuracy further. Phase stability and low loss matter, and the board must remain stable across temperature. These designs often justify premium laminates, but only when the layout and the process can use them. A premium material built with loose process control delivers little benefit over a standard one.
Prototype runs are the right place to test these assumptions. A small batch reveals how the chosen material behaves in drilling, lamination and assembly before volume is committed. Buyers who validate early avoid the expensive discovery of a stackup that cannot be built repeatably. For projects that need both fabrication and assembly under one schedule, turnkey PCB assembly keeps the process data in one place.
Questions for a Supplier Audit
Ask how impedance is verified and on what coupon. Ask which laminate is used and whether the fabricator has qualified its drill recipe on that material. Ask for the finish specification and the plating control method. These questions separate a supplier that understands RF work from one that treats it as a standard board with a different name.
Ask about first-article records. The lot should have a documented stackup, measured trace geometry, impedance results and finish inspection. When a repeat order arrives, those records become the baseline for comparison. A supplier that cannot produce them is asking the buyer to trust memory instead of data.
Ask how deviations are handled. A process drift that is caught and closed before shipment costs little. The same drift discovered in the field costs far more. A written deviation process, with clear approval steps, tells you whether the factory treats quality as a system. It also shows whether engineering has authority to stop a lot.
Finally, ask who reviews the design files. Early review of stackup, routing and finish can remove risks before tooling. That review is where PCB assembly and fabrication constraints get reconciled, and it is usually the cheapest engineering hour in the project.
Cost, Yield and Repeatability
Price per board is a poor measure on its own for RF work. A low quote that ignores impedance control will produce scrap, and scrap is paid for in schedule and rework. The real cost includes material, process control, test and the engineering time needed to close issues. Buyers should compare quotes on the scope of control, not just the number.
Yield improves when process data is reviewed regularly. Trends in line width, plating thickness or impedance reveal drift before it becomes a failure. Factories that rank their defects and remove them one by one gradually shorten lead times. Factories without data repeat the same problems at the same cost, and the customer absorbs the delay.
Repeatability is the outcome that matters most for wireless and radar programs. A board that performs well once is useful for a prototype. A board that performs the same way in the thousandth unit is what supports a product. That consistency comes from recorded parameters, calibrated equipment and trained operators working to agreed limits.
Before releasing any RF build, confirm the stackup, the impedance targets, the finish and the test plan in writing. Keep the first-article data with the lot record, and compare each repeat order against it. That simple discipline protects performance and gives the buyer a defensible basis for accepting the shipment.