Silver Copper Brazing: Solder Stop Techniques for Silver-Copper Brazing
Silver-copper brazing alloys are used where a joint has to combine high electrical conductivity with a melting point above that of solder. The eutectic alloy of silver and copper melts at about 780 degrees Celsius, flows well on copper and on many plated surfaces, and produces a joint that is stronger and more heat resistant than any soft solder. The difficulty is that the same properties that make it useful also make it hard to keep it where it is wanted.
Controlling the flow of the braze is the central problem. In a conventional soldering process the flux and the solder mask define the extent of the joint. At brazing temperature both of those are destroyed, so the definition has to come from geometry, from the surface condition of the parts and from the design of the assembly itself.
Why Soft Solder Mask Cannot Be Used
A polymer solder mask decomposes well below the brazing temperature. The resin breaks down, evolving gas and leaving a residue that contaminates the alloy and prevents wetting in exactly the region where it was supposed to stop the flow. What remains is a carbonaceous layer that has to be removed before the joint can be inspected or reworked.
The same applies to the fluxes used with soft solder. They are consumed long before the braze reaches its melting point, and their residues inhibit wetting rather than promote it. Brazing therefore relies on a reducing atmosphere or on a vacuum, or on a flux designed for the temperature, and the region around the joint has to be prepared differently from a conventional board.
Defining the Joint by Geometry
The most reliable way to stop the braze is to give it nowhere to go. The joint is designed as a lap or a butt between two surfaces whose area defines the extent of the flow, and the surrounding volume is filled with a material that the alloy will not wet or with a gap that the alloy cannot bridge. A step machined into one of the parts, a groove, or a shoulder limits the spread as effectively as any mask, and it survives the temperature.
Clearances matter in both directions. A joint gap that is too small does not fill completely, while one that is too large allows the alloy to flow away from the joint under gravity. For a lap joint the gap is usually in the range of fifty to a hundred and fifty micrometres, achieved by the fit of the parts and by a controlled quantity of alloy placed at the joint before heating. Measuring the gap on a sample after brazing shows whether the design and the fixturing achieve it.
Stop-Off Materials
Where geometry alone is not enough, a stop-off material is applied to the areas that must remain free of alloy. The traditional materials are ceramic based, such as aluminium oxide or boron nitride suspensions, which tolerate the temperature and are not wetted by the alloy. They are applied by brushing or by screen printing before the assembly is heated, and they are removed afterwards by abrasive or chemical means.
The removal step is the disadvantage. A stop-off that is not completely removed leaves an insulating residue on a surface that may later have to be soldered or plated, and removing it can damage a delicate feature. The choice of stop-off therefore depends as much on what happens after brazing as on the fit at the joint, and for a part that will be plated, a material that dissolves in a compatible etchant is preferred.
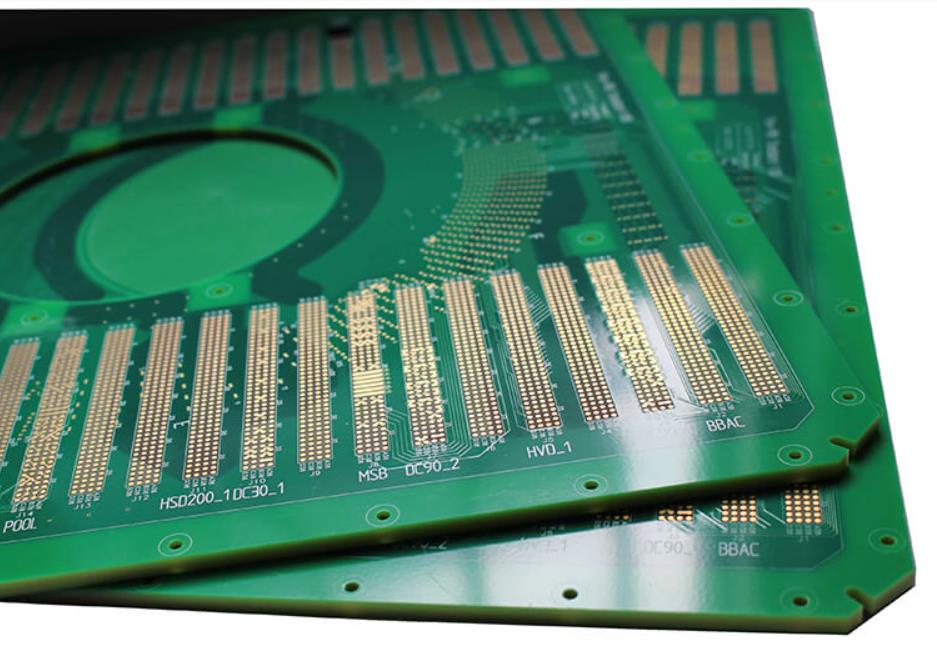
Surface Condition and Wetting
The alloy flows where the surface is clean and wets, and stops where it is not. That gives a second control mechanism, but it is a fragile one because the difference between a clean surface and a contaminated one is small and difficult to measure. Oxide on copper forms quickly at elevated temperature, and a surface that is clean at the start of the cycle may be oxidised by the time the alloy melts unless the atmosphere prevents it.
For that reason the process is normally run in a reducing atmosphere, in vacuum or in an inert gas with a tightly controlled oxygen content. Hydrogen and nitrogen mixtures are common, and the dew point is specified because moisture in the atmosphere oxidises the parts. Where a flux is used, it is a brazing flux designed for the temperature, and its activity is matched to the oxide that forms on the specific base metals rather than chosen generically.
Heating Method and Its Effect on Flow
The way the assembly is heated determines whether the alloy reaches the joint before it flows elsewhere. A slow furnace cycle allows the whole assembly to reach temperature together, which limits the temperature gradient and lets the alloy fill the joint by capillary action. A localised method such as induction or resistance heating produces a steep gradient, and the alloy tends to flow towards the hotter region.
Whichever method is used, the alloy should be placed so that it has to pass through the joint rather than across the surface. A preform shaped to match the joint, or a wire bent to follow it, keeps the molten alloy in contact with the surfaces that have to be joined. Placing a pellet of alloy beside the joint and relying on gravity is a common error, because the alloy then spreads across the flat surface rather than into the gap.
Inspection and Verification
Inspection of a brazed joint combines a visual check for flow and fillet shape with a cross section for fill and for porosity. A joint that has filled with a continuous fillet around its perimeter is generally sound, while one with an incomplete fillet indicates that the alloy was insufficient or that the gap was too large. X-ray radiography shows internal voids, and it is the practical method for joints that cannot be sectioned.
Where the joint must conduct current or heat, the resistance or the thermal resistance is measured on a sample and compared with the calculated value. Mechanical tests such as a peel or a shear test give the strength, and the fracture surface shows whether the failure was in the alloy or at the interface. Recording all three, together with the atmosphere and the temperature profile of the run, is what allows a brazing process to be repeated rather than rediscovered, in the same way that a controlled solder process is defined by its profile and its atmosphere.
Process Control and Verification
Related reading: our fabrication notes, board quality and design release notes cover the same ground.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
FAQ
Can a brazed joint and a soldered joint share the same assembly? Yes, provided the soldering is done first and the braze temperature does not remelt it. Silver-copper braze is far above any soft solder, so the sequence is fixed.
Is a stop-off always necessary? No. Where the geometry defines the joint, a stop-off adds a process step and a removal risk without adding control.
Why does the alloy flow away from the joint? Usually because the gap is too large or because the surface near the joint is cleaner than the joint itself, so the alloy prefers to spread rather than to fill.