PCBA Manufacturer Selection: A Practical Evaluation Framework
Search for a contract electronics partner and the first results are usually ranking tables. They are easy to read and almost useless, because PCBA manufacturer selection depends far more on your product than on someone else position in a list. The right question is not who is best but who is best for this board.
A useful evaluation framework looks at four things: technical capability, product coverage, quality and delivery performance, and engineering responsiveness. Weighted sensibly, those four dimensions separate suppliers that can support a programme from suppliers that can only quote it.
Why Ranking Tables Mislead
A ranking compresses every supplier into a single score, which hides the specific capabilities that decide whether a project succeeds. A factory that assembles consumer boards beautifully may have no experience with automotive traceability or with a flexible circuit that has to survive bending.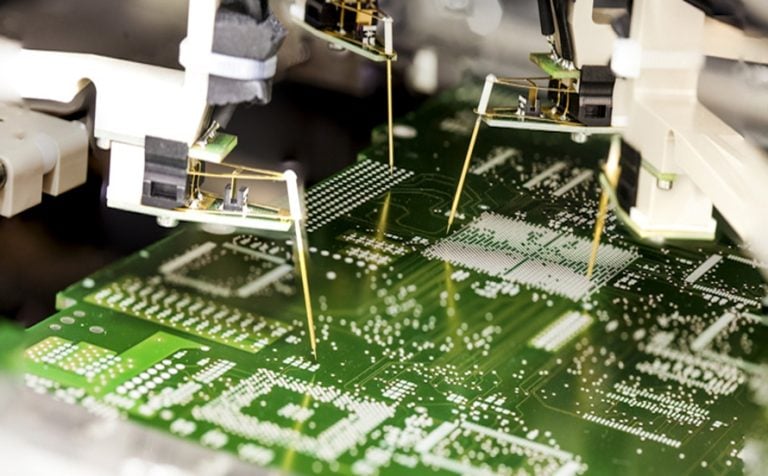
Rankings also age quickly. Capacity expands, certifications are added and quality systems improve or degrade, while a published list stays fixed. Treat any ranking as a starting point for shortlisting, never as a substitute for evaluation.
Start With the Application, Not the List
The application determines which requirements are non negotiable. Consumer and development work prioritises speed and flexibility, automotive work prioritises traceability and wide temperature performance, and medical work prioritises validation depth and change control.
Match those priorities against the supplier’s real workload rather than the brochure. A factory that runs automotive programmes daily has the habits that automotive work requires; one that has done it twice will spend your project learning them.
Technical Capability: What to Measure
Technical capability should be measured in numbers. Minimum line width and spacing, ball grid array pitch, layer count actually produced, smallest laser via and the largest copper weight processed are all concrete, comparable and difficult to overstate convincingly.
Ask for the numbers achieved in routine production rather than the best ever recorded on a demonstration build. The difference between those two answers tells you how much margin the process really has when normal production conditions apply.
Line Width, Ball Grid Array and Layer Count
These three parameters predict most assembly problems. Fine lines make routing possible, but they also demand better registration during fabrication. Dense ball grid arrays make connectivity possible, but they require reliable paste printing, accurate placement and inspection that can see beneath the package.
Layer count sits behind both. Higher counts mean more lamination cycles and more registration exposure, which is why a supplier that builds sixteen layer boards routinely is a different proposition from one that has built them occasionally.
Mixed Technology and Flex Assembly
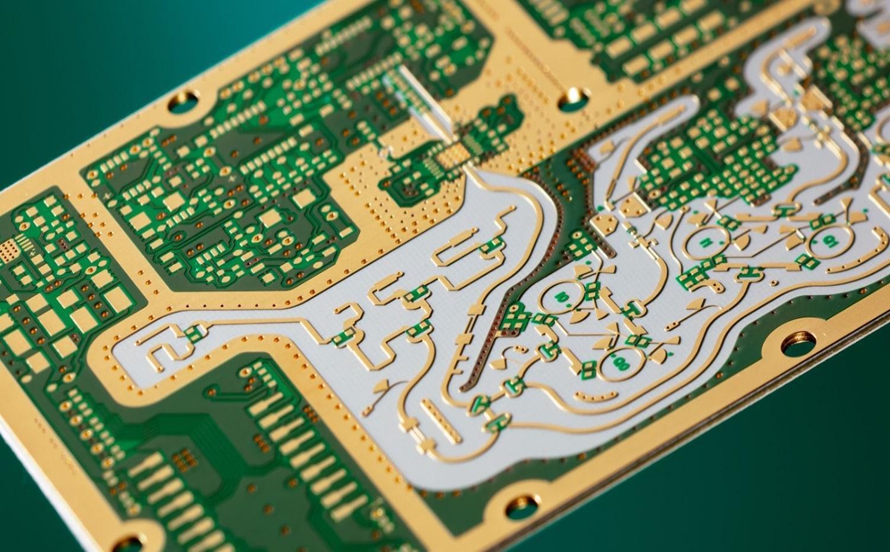
Modern products rarely use a single technology. Boards mix surface mount and through hole parts, rigid and flexible sections, and sometimes cable assemblies in the same unit. Each combination adds handling and fixturing requirements.
Genuine PCBA capability therefore includes flex assembly, mixed technology processes and the tooling that supports them. Suppliers who only run one line type will either decline the work or subcontract it, and subcontracting is where traceability usually breaks down.
Certification: Necessary but Not Sufficient
Certificates answer a narrow question: has an auditor confirmed that a system exists? They do not confirm that the system is followed on a Tuesday afternoon when a line is behind schedule and a shipment is due.
Use certification as a filter, then look for evidence of daily practice. Which measurements are recorded per lot, how non conforming material is quarantined, and who has authority to stop a line are all questions a genuine quality culture answers instantly.
Quality Systems in Daily Operation
Practical quality shows up in the inspection strategy. Paste volume measurement feeds the printer, optical inspection catches placement defects and X-ray reveals joints that cannot be seen. Functional testing then confirms behaviour rather than appearance.
That sequence should be described in process control terms, not as a list of equipment. Suppliers who explain how a defect is detected, contained and investigated are describing a system; those who list machines are describing a purchase history.
Delivery Performance and Ramp Speed
Ask for quoted cycle times at three volumes: prototype, small batch and production. Then ask what happens to those times when order volume triples. A supplier with genuine capacity can answer that question with a plan, and a supplier without it will answer with reassurance.
Ramp speed matters more than steady state speed for most products, because the first months of a programme decide the customer experience. A partner who can double output without changing process or plant has removed a large risk from the schedule.
Engineering Response Time
Response time is measurable and rarely measured. Send a realistic technical question before awarding work and note how long the answer takes and how specific it is. A vague reply in three days tells you more than an enthusiastic reply in three hours.
Design for manufacturability review belongs in this category. A supplier who identifies a stack up problem, a panel utilisation improvement or a solderability risk before production has saved money that no price negotiation could recover.
Supply Chain and Bill of Materials Support
Assembly cost depends heavily on components. A partner who can source parts, propose approved alternatives and manage long lead items removes a substantial workload from the buyer, provided the substitution process is transparent.
Look for documented component procurement procedures, including how an alternative is validated before it reaches the line and how the customer is notified. Quiet substitution is the most expensive kind of efficiency.
Prototype Versus Volume Pricing
Prototype pricing includes setup, tooling and process development, so it is normally several times the volume price. That is expected. What deserves scrutiny is how the price changes when volume rises, and whether the savings come from genuine efficiency or from reduced inspection.
A supplier who quotes across the whole range, from prototype to production, gives a clearer picture than one who quotes only the volume that suits the factory. The full picture is what allows a realistic budget to be built.
Verification Steps Before Awarding Work
Verification should include a factory visit where possible, a review of process flow for the specific product, sample test reports covering impedance, thermal cycling or reliability as applicable, and a small pilot order that exercises the real process.
The pilot order is the most informative step. It tests communication, engineering support and delivery under real conditions, and it costs far less than discovering a mismatch midway through a production programme.
A Simple Scoring Model
Weight technical capability at around thirty percent, quality and delivery at twenty five, product coverage at twenty and engineering service at fifteen, then leave the remainder for commercial terms. Score each supplier on evidence rather than impressions.
The output is not a winner but a shortlist with known weaknesses. That is more useful, because it tells the buyer which risks need contractual attention and which supplier is a reasonable fit for the first production order.
Red Flags in a Supplier Conversation
Watch for capability claims without numbers, certification presented as the whole answer, unwillingness to discuss yield and an eagerness to accept any specification without review. These are signs of a supplier who intends to sub contract the difficult parts.
Also treat unexplained speed with caution. A quotation produced in twenty minutes for a complex assembly either reflects a great library of past work or reflects no analysis at all, and the difference appears later at your expense.
Where Small Batch Support Fits
Most programmes begin small. Engineering builds, qualification lots and early customer samples are usually measured in tens or hundreds of units, and a supplier who cannot serve that phase rarely earns the production order that follows.
Partners that offer low volume assembly alongside volume capability allow a product to be qualified on the same process that will produce it at scale, which removes an entire category of transfer risk.
Documentation and Reporting Expectations
Reporting should be agreed before the first order, not requested afterwards. First article inspection reports, material certificates, inspection data and test results are all routine deliverables, but only if the customer states which are required and in what format.
Suppliers appreciate the clarity as much as buyers do. A defined reporting package removes ambiguity from acceptance and gives the factory a documented definition of what finishing a job actually means.
When to Consider a Second Source
A single supplier simplifies coordination but concentrates risk, particularly for a component or process that is hard to replace. Introducing a second source early, while quality and documentation expectations are still being defined, is far easier than doing it under pressure.
The practical approach is to qualify a second partner on a lower volume product first. That builds familiarity without disrupting the main programme, and it produces a fallback that has real experience of your standards rather than a theoretical one.
What Changes as Volumes Grow
Requirements shift as a programme matures. Prototype work rewards responsiveness, while volume work rewards stability, and a supplier has to be good at both to remain useful across a product life cycle.
Choosing a partner is therefore a long term decision rather than a transaction. Board level testing and fabrication data that accumulate over months become an asset, and rebuilding that history with a new supplier costs time that most programmes cannot spare.