HDI PCB Applications: From Phones to Servers and Vehicles
The clearest way to understand HDI PCB applications is to notice what they have in common. Every one of them involves a device that must be smaller, faster or denser than the previous generation, and every one of them reaches the point where ordinary through hole routing can no longer solve the layout problem.
High density interconnect answers that problem with blind and buried vias, finer lines and stacked build up layers. What changes between markets is not the principle but the constraint that matters most: space in a phone, loss in a server, temperature in a car and traceability in a medical device.
What Makes a Board HDI
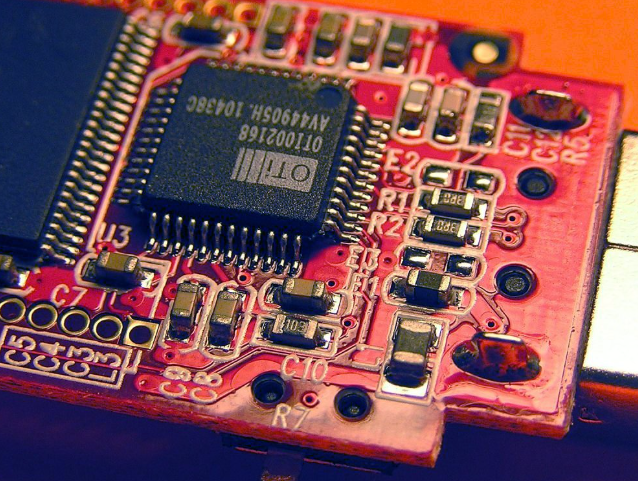
A conventional multilayer board connects layers with holes drilled through the entire stack. HDI boards use laser drilled microvias that go only where they are needed, which frees routing channels and allows components with fine pitch to escape into the inner layers.
That change is what makes dense packages practical. Fine line traces and small diameter vias let a designer place more function in the same area, or the same function in a smaller area, which is the requirement that drives adoption in almost every market.
Blind, Buried and Stacked Vias
Blind vias reach an inner layer from an outer layer, while buried vias connect inner layers without appearing on the surface. Their value is routing capacity: signals can change layers without consuming space on every layer above and below.
Stacked and staggered structures extend the idea by placing microvias on top of one another through successive build up layers. They increase density further, and they also increase process risk, because each additional lamination cycle must register accurately against the previous one.
Counting the Build Up Stages
HDI is usually described by its stage or order count. A first order board has one build up layer on each side, a second order board has two, and higher orders continue the pattern until any layer interconnect is achieved.
Each stage adds laser drilling, plating and lamination cycles, so cost rises faster than area does. This is why suppliers ask what the design genuinely needs rather than quoting the highest available capability; a second order construction is often enough where a fifth was requested by habit.
Consumer Electronics Sets the Pace
Smartphones drove HDI into the mainstream because they combined a shrinking enclosure with an expanding feature set. Main boards now carry dense radio sections, power management and sensor interfaces in a volume that once held a battery and a single chipset.
This market also established the production volumes that made laser drilling economical. When millions of boards per month require microvias, equipment costs are amortised quickly, and the process knowledge built here becomes the foundation for other industries later.
Foldables and Rigid Flex HDI
A folding device combines HDI density with flexible construction, because part of the board has to cross the hinge. Rigid flex with HDI sections allows the processor and dense circuitry to sit in a rigid area while a thinner flex section carries signals across the fold.
The manufacturing challenge is the junction. Bonding flexible material to a rigid HDI stack without losing registration or flatness is difficult, and the process window is narrow. Suppliers who build flexible circuit assemblies regularly understand these constraints better than general purpose fabricators.
Radio Boards in Base Stations
Telecommunications equipment uses HDI for the radio section, where a large antenna area and a dense processing section have to be combined on one board. Higher order constructions allow the filter, amplifier and control circuitry to be integrated close to the radiating elements.
Frequency raises the stakes. Loss and impedance consistency become part of the specification, which means the HDI process has to be controlled on materials that behave differently from standard FR-4 and on geometries that are less forgiving of variation.
Memory Interfaces in Servers
Server memory interfaces place long parallel buses on the board at very high signalling rates. HDI allows the routing to escape dense processor packages and reach memory devices without excessive layer count or stub length.
Layer counts in these designs commonly exceed ten now, and the impedance window is tight enough that etch variation and dielectric thickness both matter. The boards are not small, so uniformity across a large panel becomes as important as the peak capability.
Optical Modules and Special Substrates
Optical modules and radio frequency products often use alternative base materials such as PTFE laminates or ceramic filled substrates. These materials have electrical advantages that matter at high frequency, but they behave very differently during drilling and lamination.
Ceramic substrates also extend the operating temperature range, which is why they appear in automotive and industrial products as well as in communication equipment. Advanced PCB capability in this context means handling unusual materials without losing the process control that HDI depends on.
Automotive Radar and Domain Controllers
Automotive electronics adopted HDI as advanced driver assistance systems moved from distributed sensors to domain controllers. Radar modules need dense signal processing close to antenna arrays, while the controller needs high layer count boards that consolidate data from cameras, radar and vehicle networks.
Both sit inside a vehicle environment rather than a data centre. Vibration, thermal cycling and humidity are continuous conditions rather than occasional events, so the mechanical and material choices carry as much weight as the electrical ones.
Wide Temperature and Vibration Requirements
Operating ranges that extend from minus forty to well over a hundred degrees Celsius force attention onto expansion behaviour. Materials expand at different rates, and a stack that is electrically elegant can still crack at a plated via after repeated thermal cycles.
Vibration adds fatigue loading to solder joints and connectors. Designers respond with better pad geometry and mechanical support, while process control on plating quality protects the via structures that carry current through the changing stack.
Medical Instruments and Wearable Pumps
Diagnostic imaging, portable monitors and insulin delivery systems all use HDI for the same reason phones do, but under stricter documentation. The board must be smaller and denser while remaining traceable and cleanly manufactured.
Flexible and rigid flex HDI often appears in probes and wearable devices, where the electronics must follow a curved surface or survive repeated handling. Reliability testing then has to demonstrate behaviour over a product lifetime rather than a warranty period.
Industrial Control and Servo Drives
Industrial equipment uses HDI where a control board has to sit close to power electronics without being disturbed by them. Compact servo drives and robot joint controllers combine dense logic with significant current in a small volume.
Anti vibration design, wide temperature tolerance and electromagnetic compatibility all shape these boards. The layer structure often separates noisy power routing from sensitive control routing, which is a design decision that depends on the fabricator being able to build the stack as drawn.
Specialist Materials Beyond Standard Laminate
Not every HDI application uses FR-4. High frequency laminates, ceramic filled materials, metal core constructions and flexible films each bring advantages that matter in particular products, and each brings a different manufacturing behaviour.
Drilling parameters, lamination profiles and surface treatment all change with the material. A factory that runs a wide material set has the data to choose sensibly; one that does not will either refuse the work or learn the parameters on the customer project.
Cost, Stage Count and Where the Money Goes
The largest cost drivers in an HDI order are the number of build up stages, the panel area consumed and the yield achieved. Material is significant but rarely dominant, which is why a design review that removes an unnecessary stage often saves more than a material substitution.
Small board sizes improve panel utilisation, and a well planned layout and stack up can fit more parts per panel. These are engineering decisions, and they are best made with the fabricator before the design is released rather than negotiated after quotation.
Questions to Ask an HDI Supplier
Ask which stage counts are in routine production rather than occasional. Ask how microvia quality is verified without destroying the panel, and how registration is measured between build up layers. Ask what the minimum line width and via diameter are in practice.
Then ask how the factory proves the result. Board level testing and coupon measurements should be routine, with data kept per lot. Answers that include numbers and methods indicate a process that is genuinely understood, rather than one that is merely listed on a capability sheet.
Where HDI Demand Goes Next
Every market described here is growing at once, and they are converging on similar requirements. A vehicle controller now resembles a server board, a medical device resembles a consumer product in size, and a robot combines all of the above in one assembly.
For manufacturers, the outcome is that HDI capability is a common foundation rather than a specialised offering. The manufacturing process behind it has to be repeatable across very different products, which is the real test of a supplier in the years ahead.