FPC Structure Design: Layers, Coverlay and Stiffeners
A flexible circuit is often treated as a flat cable with chips on it. In practice, FPC structure design decides almost everything about the finished part: how many times it can bend, how much current it can carry, whether it survives reflow and how much space it consumes inside a product.
The stack is built from a small number of elements that are combined in many ways. Base film, copper foil, adhesive or adhesiveless construction, coverlay, stiffener and via system are the vocabulary, and the application decides which combination is appropriate.
What a Flexible Circuit Is Made Of
The base film provides mechanical support and electrical insulation. Polyimide dominates because it tolerates soldering temperatures and holds its dimensions through processing, while polyester appears in low cost products that never see a reflow oven.
Copper foil provides the conductors, and its type matters more than its thickness in dynamic applications. Vias connect layers where needed, and a protective layer covers the finished traces except where components or connectors must be attached.
Base Film and Copper Foil
Polyimide is available in a range of thicknesses, commonly between twenty five and a hundred micrometres for flexible circuits. Thinner film bends more easily, but it also provides less mechanical protection and is harder to handle during manufacture.
Copper selection follows the application rather than the specification sheet. Rolled annealed foil has a grain structure that resists fatigue and is used wherever the circuit moves repeatedly, while electrodeposited foil is adequate and cheaper for static applications.
Coverlay and Its Openings
Coverlay is a film of polyimide with an adhesive layer, laminated over the finished conductors to protect them from contamination and mechanical damage. Where a component or connector must be soldered, the coverlay is opened, and the accuracy of those openings affects assembly yield.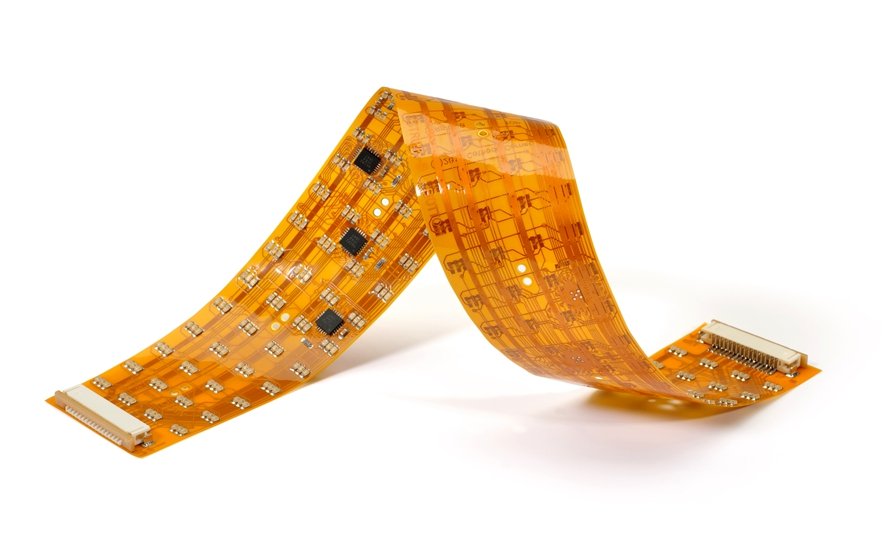
Openings that are too small leave adhesive on the pad and interfere with soldering. Openings that are too large expose nearby traces to solder bridging. The tolerance window is therefore a manufacturing concern that should be agreed with the fabricator rather than fixed by the designer alone.
Stiffeners and Bending Zones
A flexible circuit cannot support a connector or a heavy component on its own, so a stiffener of polyimide, FR-4 or metal is bonded to selected areas. Stiffeners create the rigidity needed for reliable soldering and mechanical retention.
Their edges are critical. A stiffener that terminates abruptly close to a bend concentrates stress at the transition and shortens the fatigue life of the part, which is why the distance from reinforcement to motion is treated as a controlled dimension.
Vias in Flexible Material
Vias connect the conductors on different layers. Because the base film is thin and compliant, they are usually formed by laser or by mechanical drilling with parameters adjusted for the material rather than copied from rigid board work.
Plating quality matters even more here than in rigid boards. A via in a moving circuit sees mechanical load as well as electrical current, so incomplete fill or thin plating becomes a fatigue crack rather than a simple open circuit.
Single Sided and Double Sided Constructions
A single sided circuit has conductors on one face and is the simplest and cheapest option. It suits connections where signal count is low and no shielding or reference plane is needed, such as a speaker link or a simple sensor lead.
A double sided circuit doubles the routing capacity and allows a ground plane to be added, which improves signal behaviour and mechanical balance. Most modern flex assemblies in phones and cameras use at least two conductive layers.
Multilayer Flex and Its Limits
Multilayer flexible circuits stack several conductive layers with thin dielectric between them. They support dense routing, controlled impedance and shielding in a single thin assembly, and they are common in advanced camera modules and dense sensor packages.
The limits are mechanical and economic. Each additional layer reduces flexibility, increases lamination complexity and raises cost. Designers who genuinely need four layers should use four, but designs that add layers out of caution usually lose more in bend performance than they gain in routing freedom.
Rigid Flex Constructions
Rigid flex combines rigid sections for components with flexible sections for movement, producing a single board that needs no connecting cable. This removes connectors, reduces assembly steps and improves reliability in products that fold or articulate.
Manufacturing difficulty comes from the bond between the two material systems and from keeping the mixed stack flat through multiple lamination cycles. Suppliers who build flexible circuit assemblies as a core business manage that complexity routinely; others treat it as an exception.
Adhesive Versus Adhesiveless
Older constructions bond copper to film with an acrylic adhesive. That layer is thicker, can creep under repeated load and may delaminate after thermal cycling, all of which reduce fatigue life in dynamic applications.
Adhesiveless laminates deposit or cast copper directly onto the film, producing a thinner stack with better dimensional stability and improved bend performance. They cost more and demand tighter process control, which is why the choice is usually made by application rather than by price.
Shaped and Curved Routing
Flexible circuits are often cut into shapes that follow the geometry of the product, with slots, tabs and cutouts that guide the part into position. This is a genuine advantage, because the circuit can be designed to fit an enclosure rather than requiring the enclosure to accommodate a rectangle.
Shaped contours also reduce weight. Slots that remove material from non functional areas lower mass and increase local flexibility, provided the remaining route does not concentrate stress where the part moves.
Impedance Control in a Flex Design
High speed signals increasingly cross flexible sections, which means impedance must be held through a structure that changes thickness. A trace over a bonded stiffener behaves differently from the same trace over bare film, and a bend changes the geometry again.
Managing this requires a clear stack up and layout decision about which layers form the reference and where the transitions occur. When it is handled during design, the result is predictable; when it is ignored, the link works on the bench and fails in the field.
Thermal Behaviour and Heat Spreading
Flexible circuits have limited ability to spread heat, because the copper is thin and the film is a poor conductor. Where a flex carries power or supports a dissipating component, heat has to be managed deliberately rather than assumed to disappear.
Wider copper areas, additional metal layers and thermal vias all help, as does mechanical contact with a housing that can act as a heat sink. The flex and HDI capability of the fabricator determines how much of that can be built without harming flexibility.
Design Rules That Protect Bend Life
Conductors should cross bend lines at right angles, and the bend radius should be generous relative to the stack thickness. Traces that must turn within a moving region should do so gradually, with widened transitions rather than sharp corners.
Ground planes need the same attention. A solid copper plane in a dynamic bend cracks before the signal traces do, so many designs use cross hatched or parallel finger structures that move with the conductors while still providing a reference.
Common Fabrication Mistakes
Most flex failures originate in decisions that were never discussed. Coverlay openings sized without reference to the assembly process, stiffeners placed for mechanical convenience, panel layouts that ignore material grain direction and vias placed where the part will bend are all common causes.
These are avoidable through an early review. A short conversation between designer and fabricator before release costs hours; discovering the same problem after qualification costs weeks and a new tooling cycle.
Specifying a Flex Design to a Supplier
The specification should state the dynamic areas, the expected bend radius and the required number of cycles. It should identify the copper type for those areas, the stiffener requirements, the coverlay type and the impedance targets with tolerances.
It should also state the assembly process, because reflow compatibility influences material selection. Suppliers who provide manufacturing process and assembly support together can validate those assumptions before tooling is committed.
How Flex Structures Are Tested
Verification for a flexible structure includes more than continuity. Impedance measurement on production coupons, cross sections through vias in flexible material, peel strength checks and dynamic bend testing on representative samples all describe whether the structure behaves as designed.
Those results need to be linked to the lots they came from, which is where board level testing and fabrication records meet. Without that link, a failure discovered during assembly cannot be traced back to the process change that caused it.
Matching Structure to Application
A wearable sensor, a folding phone hinge, a robot joint and a vehicle battery harness all use flexible circuits, but they demand different structures. The differences lie in copper type, layer count, stiffener strategy and the amount of protection the environment requires.
Getting that match right is the whole point of structure design. The right answer is rarely the most advanced construction available; it is the simplest structure that survives the conditions the product will actually see, and proving that before production is what separates a reliable product from an expensive experiment.