PCB Component Sourcing for Reliable Parts Procurement
Component sourcing decides whether a PCB build starts on time or stalls at the line. A missing part or a suspect reel can stop a whole production run. The work begins with the BOM, long before any purchase order is issued. Buyers and engineers need a clear view of part status, approved alternates and supplier records. This guide covers the decisions that shape reliable electronic parts procurement.
Sourcing is not a separate purchasing task that runs after design. It connects engineering, quality and production planning from the first prototype. Each part on the BOM carries a lifecycle status, a package, a tolerance and a supply risk. Someone must check those details against the design intent. When this review happens early, the assembly team receives parts that fit the process and the schedule.
Reading the BOM Correctly
The BOM lists every component the board needs, including part numbers, manufacturers, quantities and specifications. It also carries approved alternatives and supplier references. A complete BOM lets purchasing act without guesswork and lets engineering confirm intent. Weak BOMs invite wrong parts, duplicate orders and late changes. Reviewing the document before release is the cheapest check available to any project team.
Part numbers alone are not enough. The same value can exist in several packages, voltage ratings and tolerance grades. A resistor specified for one footprint may not fit another. Engineers should confirm that the BOM matches the schematic and the layout. Buyers should confirm that each line has a real, orderable part behind it. Both checks take minutes and prevent costly rework.
Version control is the next layer of BOM discipline. Designs change during prototyping, and a BOM that lags behind the schematic sends the wrong parts to the line. Each revision should carry a clear identifier and a date. Purchasing should work only from the released revision, never from an emailed spreadsheet. When a change is approved, the old revision should be withdrawn so nobody orders from it by habit.
Active and Passive Components
PCB components divide broadly into active and passive types. Active parts need power and can amplify, switch or process signals. Integrated circuits, microcontrollers, processors and transistors fall into this group. Passive parts do not provide gain and usually need no external supply. Resistors, capacitors and inductors are the common examples. The split matters because each group carries different sourcing risks.
Active components often have longer lead times and narrower second-source options. A single microcontroller can hold up an entire build. Passive parts are usually easier to find, but they still face allocation during demand spikes. Package size adds another constraint. A 0603 part has a nominal footprint of 0.06 by 0.03 inches, so a substitution in another size will not fit the pads.
Common Parts and Their Roles
Most boards carry a familiar set of parts. Resistors limit current and set voltage division. Capacitors filter, decouple and stabilize supply rails. Diodes steer current and protect circuits from reverse polarity or transients. Transistors switch and amplify. Connectors link the board to cables, modules and equipment. Oscillators provide timing, and relays or transformers handle isolation where the design needs it.
Each part type brings its own sourcing question. A capacitor may need a specific dielectric and voltage rating, not just a capacitance value. A diode may need a particular recovery speed. A connector may need an exact mating height. Buyers who treat these as interchangeable values invite field failures. The BOM should state the critical parameters so purchasing cannot substitute on price alone.
Qualifying Alternative Parts
Approved alternatives reduce the risk of shortages and line stops. They are most valuable for critical active parts and long-lead items. The alternative must be technically verified before it enters the BOM. Package dimensions, pin configuration, electrical limits and thermal behavior all need checking. Firmware compatibility matters too, especially for memory and controllers. An unverified alternate is a risk, not a safeguard.
Qualification should happen during design, not during a shortage. Engineers can compare datasheets and confirm footprint compatibility while the layout is still open. Once approved, the alternate sits in the BOM with its own part number and supplier. Purchasing can then switch without a new engineering cycle. This preparation keeps rapid PCBA prototyping moving when a primary part goes on allocation.
A qualified alternate also needs a bench check before it ships in volume. A small sample should be built and tested against the original part. The check should cover function, timing and thermal behavior under load. Results belong in the part record, not in someone’s memory. When a shortage forces the switch, the team already knows the alternate works. That record turns a panic decision into a planned one.
Supplier Selection and Monitoring
Supplier choice shapes quality, traceability and delivery performance. Buyers should evaluate authenticity controls, quality systems, technical support and supply capacity. Delivery history and industry experience add useful weight. A structured evaluation reduces procurement risk and supports stable supply over time. Price alone tells very little about the true cost of a part.
Long-term relationships improve continuity when demand shifts. Strategic sourcing should consider capacity, geographic spread, responsiveness and inventory position. Regular BOM reviews catch obsolete or constrained parts before they reach the line. End-of-life notices, manufacturer changes and lead-time trends belong in that review. Teams that monitor these signals avoid surprises that a purchase order cannot fix.
Counterfeit risk deserves its own check. Parts bought outside authorized channels may look correct and fail in the field. Buyers should ask where the stock originated and whether traceability runs back to the manufacturer. Incoming inspection can confirm marking, packaging and basic electrical behavior on a sample. A cheap reel that cannot be traced is expensive once boards fail. The sourcing record should show the channel for every critical part.
Procurement Challenges to Plan For
Environmental compliance belongs in component selection, not in a late audit. Many parts must meet RoHS and similar requirements, and evidence should be collected at purchase. Technology changes add pressure, because packages and processes evolve while older parts disappear. Supply and demand swings affect price and availability with little warning. Design requirements add a final constraint, since a part must fit electrically, mechanically and thermally.
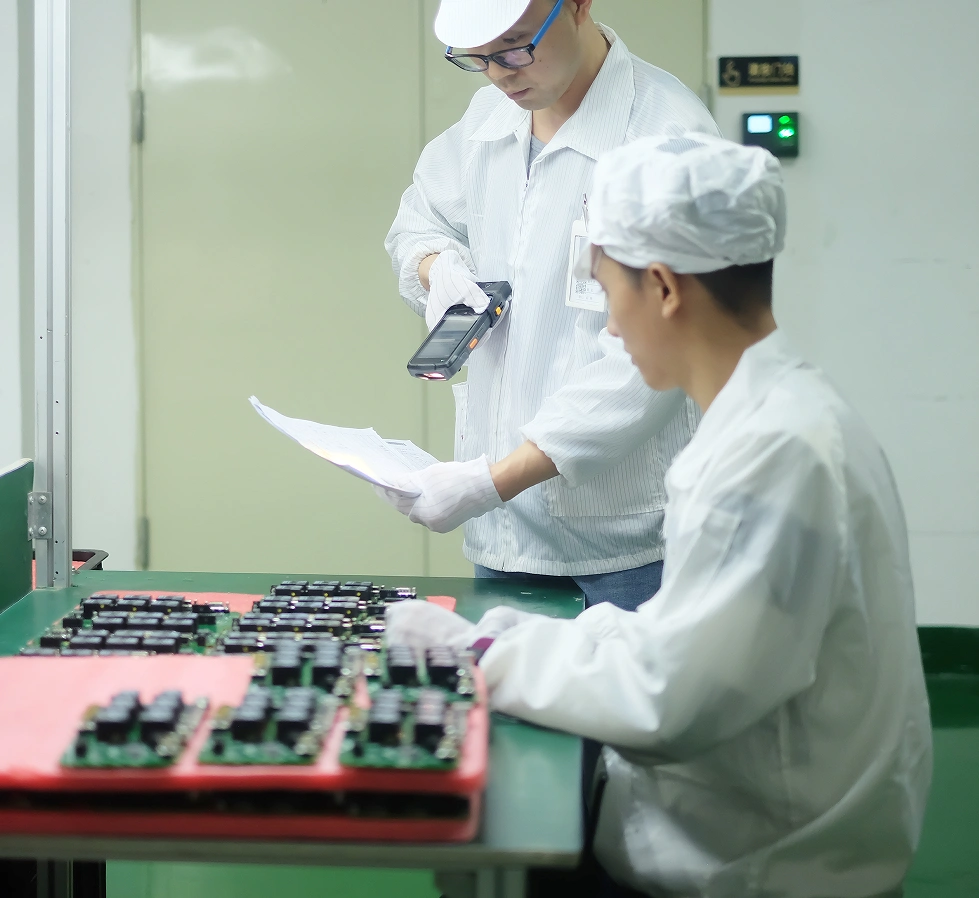
Close coordination between engineering, procurement and manufacturing keeps these risks manageable. DFM and DFA reviews can expose assembly problems before tooling is built. Qualified alternates and monitored critical parts soften supply shocks. Compliance records should travel with the lot. When these practices run together, a shortage becomes a scheduling question rather than a quality incident.
Moisture sensitivity is a common failure mode that sourcing teams often miss. Parts in moisture-sensitive packages absorb water during storage and can crack during reflow. The BOM and the part record should note the sensitivity level and the floor life. Dry storage and baking schedules belong with the material plan. A reel that sat open over a weekend can ruin a batch. Buyers should confirm that storage rules are written down and followed.
Integrating Sourcing With Assembly
Component sourcing works best when it sits beside fabrication and assembly. One partner can coordinate material purchase with the production schedule and hold parts until the line is ready. That link matters for prototypes and for repeat orders alike. It also shortens the loop when a part needs replacement. Buyers gain a single point of contact for the whole build.
Integrated sourcing supports SMT PCB assembly by matching reels and trays to the placement program. It supports inspection because the approved part list is fixed before the run. It supports test because the expected behavior of each part is known. For projects that need the full scope, turnkey PCB assembly covers fabrication, procurement, assembly and test under one schedule. Buyers can also review PCBA testing coverage before release.
Documentation ties the whole chain together. The factory should record which program ran, which reels were used and what inspection found. If a field return arrives months later, that record is the fastest route to the cause. Buyers should ask for these records as a routine part of each order. Production records tend to be maintained truthfully when they can be readily supplied upon request.
Prototypes remain the cheapest place to find sourcing mistakes. A small pilot batch reveals footprint conflicts, tolerance issues and process behavior before volume is committed. The first article should confirm that every part fits, functions and survives test. Teams that invest here reach volume faster and with fewer surprises. Sourcing discipline at this stage pays back across the whole program.
For a complete manufacturing scope, our PCB assembly service links procurement with fabrication and test. Send the BOM and design files for a review, a clear quotation and a delivery date you can plan around. Confirm part status, approved alternates and compliance evidence before the order is placed. Those three checks carry a build from first article to final carton with fewer interruptions.