Glass Transition Temperature: PCB Laminate Properties That Affect Manufacture
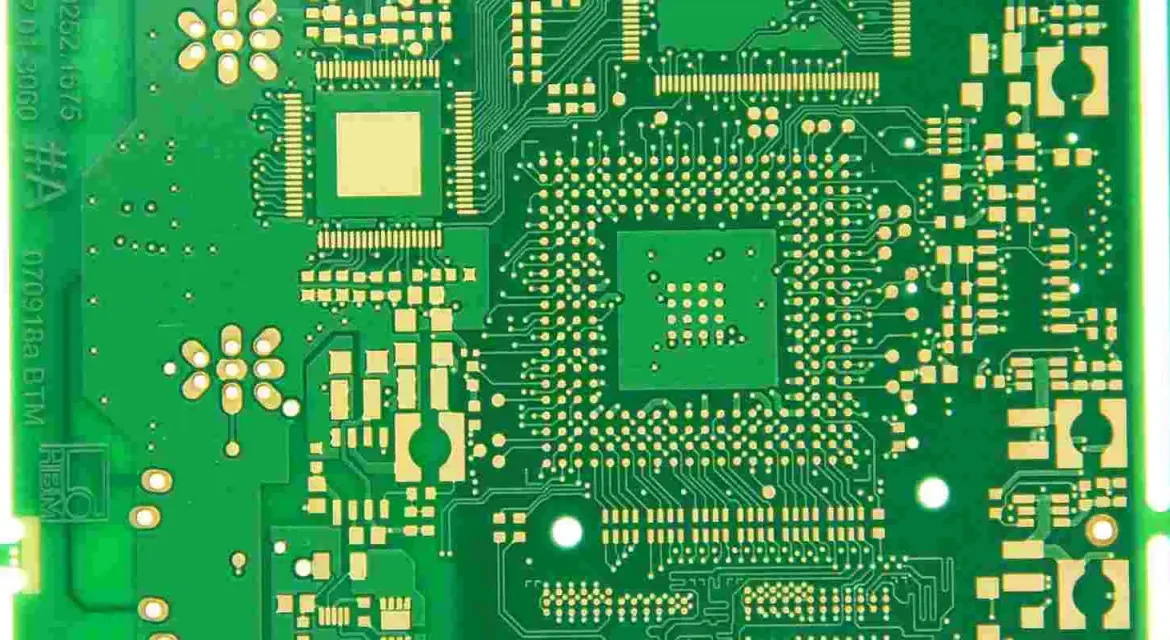
A printed circuit board starts as a stack of materials that have to keep their dimensions through heat, pressure and chemical processing, and the properties that make that possible are not the ones a designer normally thinks about. Understanding them explains why some designs are routine and others are difficult to build.
What the Laminate Has to Do
The laminate has to bond to copper, resist the chemicals of the process, keep its dimensions through several thermal excursions and remain electrically insulating over the life of the product.
Those requirements are met by a composite: a glass fabric for mechanical strength, a resin for bonding and insulation, and fillers for specific properties. The balance between them is what distinguishes one grade from another. Our laminate material notes describe the properties.
Glass Transition Temperature
The glass transition temperature is the point at which the resin changes from a rigid solid to a softer state, and it is the parameter most often quoted. Above it the material expands faster, its modulus falls and its resistance to chemical attack decreases.
The relevance to the process is the assembly temperature, which is above the transition point of a standard laminate. A material with a higher transition temperature stays rigid through reflow, which reduces the movement of the board and the stress on the joints.
Thermal Expansion and Its Consequences
The expansion of the laminate along the thickness direction is much larger than in the plane, because the glass fabric restrains it in the plane. That difference is why a plated hole in a thick board experiences significant stress during assembly.
The expansion in the plane matters for the position of features, which is why a board that is heated during processing can end up slightly larger than it was drawn. The expansion is accounted for in the registration budget rather than corrected afterwards.
Dielectric Constant and Loss
The dielectric constant determines the impedance of a controlled line for a given geometry, and its variation with frequency determines how much the impedance changes across a band. The loss tangent determines how much of the signal is absorbed by the material.
Both are specified at a frequency, and quoting them without one is meaningless. A material with an excellent loss tangent at ten gigahertz may behave differently at one gigahertz. Our high frequency laminate notes describe the choices.
Moisture Absorption
The resin absorbs a small amount of moisture from the air, and that moisture turns to steam during reflow. In a well-made board the steam escapes slowly; in a board with a defect it accumulates and causes delamination.
The moisture content is controlled by baking before assembly and by dry packing for storage. A board that has been stored in a humid environment without packaging should be baked before it is assembled.
Mechanical Strength and Handling
The laminate’s flexural strength determines how much a thin board can be handled without damage, and its peel strength determines how well the copper adheres. Both fall when the material is hot.
That is why handling a board above its transition temperature is discouraged: the copper adhesion is at its weakest and the material is at its most compliant, so a small force produces a permanent deformation.
Halogen-Free and Other Specifications
Halogen-free materials avoid a class of flame retardant that has environmental restrictions, and they are required for some markets. Their process behaviour differs from standard materials, particularly in drilling and in the adhesion of the mask.
The specification should be stated on the drawing rather than assumed, because the shop will otherwise use what it stocks. A change of material after the stack is released changes the impedance of every controlled line.
Choosing a Material for the Application
The choice follows from the temperature the assembly will see, the frequency the signals carry, the mechanical environment and the regulatory requirements, in that order. Each of those rules out a class of materials.
Availability should be confirmed at the same time, because a material that meets every requirement and is on allocation will cost more in schedule than in price. Our cost reduction notes describe how the choice affects the price.
Process Control and Verification
Keeping a sample from the panel turns a dispute into a measurement, because the same coupon can be re-examined by both parties without rebuilding the batch. Reviewing the design before the data is released is cheaper than correcting it after the panel is in the tank, because every step downstream inherits the decision made at the front end.
Documenting the assumption is part of the design work, and a short note on the drawing prevents a question that would otherwise arrive a day later and cost a day of schedule. The process window is set by the narrowest step in the flow, so an improvement anywhere else shows up as margin rather than as yield until that step is addressed.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
A parameter that is set once and never re verified drifts, and the drift is usually discovered by a defect rather than by the record. The tooling, the material and the profile form one system, and a change to any of them should be assessed against the other two before it is released.
Verification and Records
Where the process window is narrow, the measurement resolution has to be better than the window, or the data cannot distinguish a good part from a marginal one. A record that identifies the operator, the date and the settings is worth more than a record that identifies only the result.
Points to Confirm at First Article
The acceptance criteria should be written before the work starts, so that the decision is made by the specification rather than by the person inspecting.
Documented Process Control
Where an operation cannot be verified afterwards, it has to be controlled during the operation, and that control has to be visible in the record. Sampling is a compromise between cost and confidence, and the sample size should follow from the failure rate that has to be detected.
FAQ
Is a higher glass transition temperature always better? It is better for the assembly process and for the dimensional stability, and it costs more and is harder to drill. Where the product will not see a high assembly temperature or a hot environment, the standard material is adequate.
Does the dielectric constant change with the stack? It is a property of the material rather than of the stack, but the effective dielectric constant of a line depends on the geometry around it, which is why the impedance calculation uses the stack rather than the material alone.
What does gopcb confirm about a laminate? We confirm the grade and manufacturer, the glass transition temperature, the dielectric constant and loss at the frequency of interest, the thickness tolerance and the availability. Where the specified material is not in stock we propose an equivalent and quote both rather than substituting silently.