PCB Solder Mask Color Selection Guide for Engineers
Solder mask color looks like a cosmetic choice until the first inspection shift struggles to read a joint. The same discipline applies to PCB solder mask color, where a small process drift turns into a large yield loss. Green remains the default for good reasons, but red, blue, black, and white each change how a board is inspected, handled, and sold. This guide explains what each color does to the process, so engineers and buyers can choose with evidence rather than habit.
Color is a pigment added to the same resin family, so the basic electrical role stays the same. The mask still covers traces, blocks solder bridges, and limits oxidation on copper. What changes is how light behaves at the surface, how the coating cures, and how easily a defect is seen. Those three effects drive most of the real cost difference between colors. Reviewing PCB solder mask color before the first article is built saves rework later in the run.
What Solder Mask Color Changes
The pigment load in the mask affects cure behavior and surface finish. Darker colors absorb more energy during exposure and heat, so the lamination and curing windows need checking. Lighter colors reflect more light, which helps some inspection steps and hurts others. None of this is a defect in the material itself. It is a process shift that the factory must plan for before the panels enter the line.
Visual contrast decides how quickly an inspector or a camera finds a problem. A joint that stands out against the mask is easier to judge than one that blends into it. This matters most at automated optical inspection, where the lighting recipe is tuned per color. Changing the color mid-program forces a new recipe and a fresh validation. For teams starting a build, rapid PCBA prototyping is a practical way to test a color choice before volume.
Color also sets buyer expectations about the product. A black board reads as premium, a white board reads as lighting, and a green board reads as standard. Those expectations are legitimate inputs, but they should never override the technical checks. The useful order is to settle function first, then confirm the color supports inspection and handling, and only then discuss appearance. Documenting PCB solder mask color keeps assembly, inspection and test teams working from the same numbers.
Green as the Baseline
Green has dominated for decades because the whole supply chain is tuned around it. Material is widely stocked, cure windows are well understood, and inspection recipes exist on almost every machine. That maturity lowers risk on a new build. It also means a green board is rarely the reason a project slips. When schedule matters more than appearance, green is the safe starting point for a first article.
Green also gives reasonable contrast against bare copper and solder, which helps manual rework and final visual checks. The color is easy on the eye during long inspection shifts, a small point that matters on high-volume lines. None of this makes green technically superior in insulation or thermal terms. It simply means fewer unknowns. Engineers who need a documented baseline can treat green as the reference and measure every other color against it.
One practical check on green is registration, not shade. The mask must clear every pad and via without exposing copper that should stay covered. A green panel that passes registration on one lot can fail on the next if the exposure energy drifts. Ask the fabricator how it monitors exposure dose and how often it checks registration against the artwork. Those two records matter more than the color name on the order.
Red for Visibility
Red mask creates strong contrast with metallic joints, so misplaced parts and bridges stand out during assembly. Inspectors often spot incomplete joints faster on red than on darker surfaces. The material offers stable insulation and temperature behavior similar to green, which suits many industrial and consumer builds. Automotive modules sometimes use red for clear identification inside a housing. The gain is mostly in inspection speed, not in electrical performance.
Outdoor products need a caution here. Some red pigments fade under prolonged strong sunlight, so the surface can shift in tone over years. That fading is usually cosmetic, but it can confuse visual checks and upset a customer. If the board sees direct sun, ask the supplier for a UV-resistant grade and confirm it in writing. Then verify the choice during SMT PCB assembly so the first lot matches the drawing.
Red also changes how a camera sees the legend. White ink on red can bleed at the edges if the print is thin, and the contrast that helps manual inspection may confuse a fixed lighting recipe. Run the first panel through the actual AOI program before release. If the recipe needs retuning, do it on the pilot lot rather than on a full run. That single step catches most red-specific inspection surprises early.
Blue for Readability
Blue mask with white silkscreen gives some of the best legend readability available. Technicians can find connectors and test points quickly on a dense board. That is why medical instruments, test equipment, and industrial controllers often specify blue. Insulation and chemical resistance are close to green, and the color itself does not meaningfully change heat dissipation. The benefit is clarity for the people who service the product.
Blue does bring process questions on some special flows. Coating thickness and cure settings may need extra verification, and the legend ink must bond well to the surface. A short conversation with the fabricator before release prevents most of these issues. For designs that combine color with higher layer counts, the same review applies to PCB assembly planning, where the stackup and the mask are confirmed together.
Blue is also less forgiving of surface scratches than green in some lighting. A scuff that disappears on green can read as a bright line on blue and fail a visual standard. Define what counts as a cosmetic defect before the lot runs, and put that definition on the drawing. Buyers who skip this step often argue about appearance after delivery. A written cosmetic limit removes that argument and keeps both sides judging the same surface.
Black for Concealment
Black mask hides internal copper patterns, which suits products where layout confidentiality or a clean look matters. Security devices and premium consumer goods use it for exactly that reason. The surface also resists UV aging better than many lighter colors, which helps outdoor enclosures. The tradeoff is heat. A black surface absorbs more radiant energy, so thermal margins deserve a second look on power boards.
Handling is the other cost. Scratches, dust, and fingerprints show clearly on black, so the line needs stricter discipline from lamination through packing. Inspection lighting must be set carefully, because dark surfaces hide shallow voids that lighter masks reveal. High-speed and sensitive designs may need a different stackup entirely, and PCBA testing should confirm performance rather than appearance alone.
Black also makes via holes and bare copper edges harder to see, which slows manual review of coverage. Inspectors rely on angled light and magnification to judge mask thickness near pads. If the factory has not run black recently, ask for a sample panel under its normal inspection setup. A quick look under real lighting tells you more than a color swatch. That check costs one panel and prevents a full lot of rework.
White for Reflection
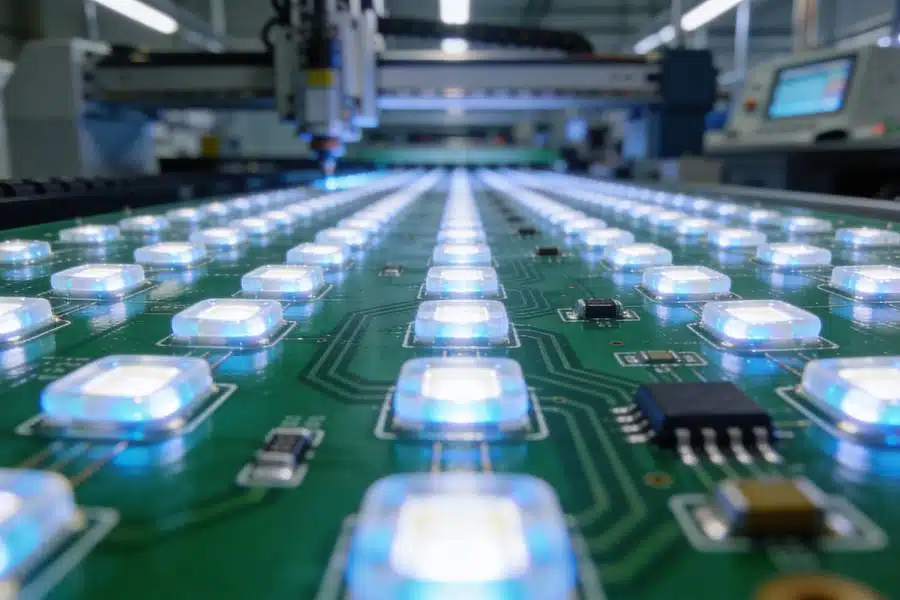
White mask reflects light, which is why LED boards rely on it. The surface bounces emitted light outward and supports more uniform output across the panel. Combined with dark silkscreen, white also gives crisp legends for control panels and displays. Purity and stability matter here, because a mask that yellows over time changes the light color and the product look. Ask how the grade holds up under the intended drive conditions.
White shows contamination easily. Dust, flux residue, and handling marks are visible, so cleaning and glove rules need to be tight. In harsh environments, the board may need periodic cleaning to keep its appearance. These are manageable requirements, but they belong in the process plan rather than in a late complaint. Buyers comparing quotes should confirm that the supplier has run white before and knows its cure window.
Yellowing is the failure mode to watch on white. Heat and light during service can shift the tone, and a board that starts bright can drift toward cream. That shift changes reflected light and can spoil the look of a finished fixture. Ask for the cure window and the storage conditions the material needs. Then confirm the first lot against a retained sample, so any drift shows up before the customer sees it.
Matching Color to Process
Each color carries its own coating, exposure, and cure settings, and the fabricator must confirm compatibility before tooling. A material that cures well in green may need a different energy dose in black. Legend adhesion also varies with surface energy. Raise these points at the DFM review, not after the panels are etched. A supplier that answers with process data is easier to trust than one that answers with a color chart.
Inspection and test plans should follow the color choice. Cameras need a lighting recipe tuned to the surface, and manual stations need the right lamps. Where the product also needs sourcing and box build, a turnkey PCB assembly partner can align mask, legend, and test in one scope. That single point of contact shortens the feedback loop when a first article shows a contrast problem.
Buyers should also check how the supplier records the mask grade. The order should name the material, the color code, and the finish, not just the word black or blue. Ask whether the supplier keeps a retained coupon from each lot. That coupon settles disputes about shade and coverage months later. A supplier that keeps these records is easier to audit and easier to hold to the agreed specification on repeat orders.
The buying takeaway is simple. Choose the color that supports inspection, environment, and appearance in that order, then confirm the process window with the factory in writing. Record the material grade and the agreed settings on the drawing. That record turns a cosmetic preference into a controlled specification, and it protects both the engineer and the buyer on every repeat order.