Panelization and Depaneling: Design Rules and Cost
Panelization is the arrangement that lets an assembly line handle a small board, and depaneling is the step that returns it to a single unit. Both are decided at layout, and both cost money if the arrangement is chosen after the artwork is finished.
What the Panel Carries
Beside the boards themselves the panel carries the rails, the fiducials, the tooling holes, the test coupons and the clearance that the conveyor and the placement head need. Each of those consumes area that could have held product.
Panel utilization is therefore a design decision rather than a purchasing one. Our layer count notes describe the other decision that is made at the same review.
Rail Width and Fiducials
The rail has to be wide enough for the conveyor fingers and stiff enough that the panel does not sag in the reflow oven. Fiducials belong on the rail as well as on each board where the placement accuracy justifies it.
A fiducial that is covered by the stencil is not a fiducial. Our silkscreen notes describe the keep out that protects it.
Breakaway Tab Design
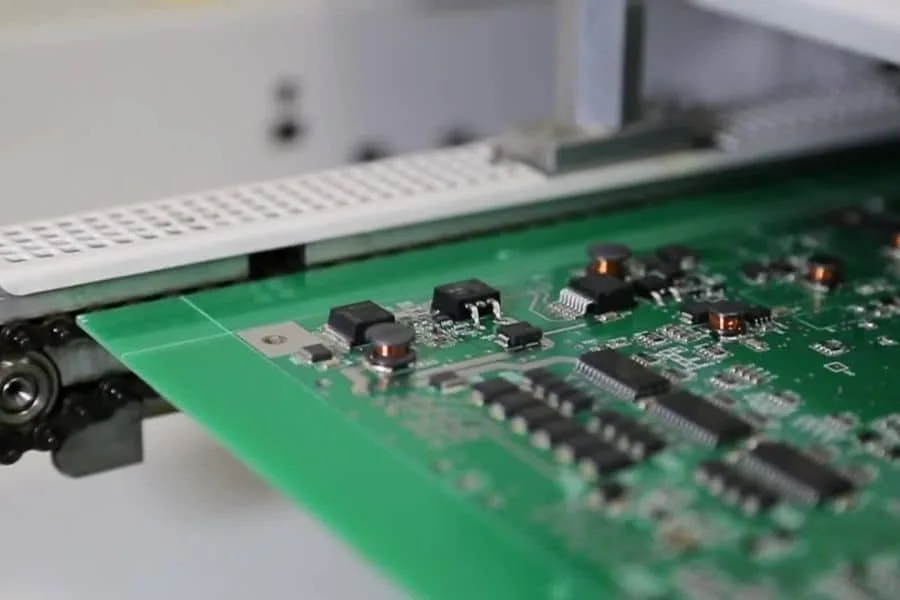
A breakaway tab is a deliberate weak point, and its width sets the force needed to separate the board. Too wide and the separation damages the laminate; too narrow and the board moves during assembly.
The tab should be placed where the resulting nib does not interfere with a connector or a screw boss. Our tab design notes describe the routing relief that controls it.
Board Spacing and Routing Channels
Board spacing has to cover the router diameter and the tolerance of the placement of every board on the panel. A spacing that suits the nominal artwork will not suit the worst case panel.
Where the board outline tolerance is tight, the spacing is what absorbs it. Our outline tolerance notes set out the figure.
Depaneling Methods
Routing, laser cutting, punching and hand breaking all remove the tabs, and each imposes a different stress. Routing leaves a smooth edge but generates dust; laser leaves a clean cut but a heat affected edge.
The method should be chosen against what the board carries near the edge. Our board failure notes describe the damage that shows up later.
Panel Utilization and Cost
Panel utilization is the area of product divided by the area of the panel, and it is the number that decides the fabricated price per board. A change of orientation that adds one more board per panel is often worth more than a change of material.
It is also the number that decides how many placements the line performs per panel. Our cost driver notes describe the trade.
Tolerances That Decide Assembly Yield
The placement of the board within the panel, the tab width and the panel warp are the three that most often reach the assembly line. Each should carry a stated tolerance rather than an implicit one.
Where the panel is warped, the printing step suffers first. Our warpage notes describe the control that keeps it flat.
Process Control and Verification
Running a first article through the same checks as the production panel confirms that the two agree, and that comparison is the cheapest form of process control available at prototype stage. Keeping a sample from the panel turns a dispute into a measurement, because the same coupon can be re-examined by both parties without rebuilding the batch.
Reviewing the design before the data is released is cheaper than correcting it after the panel is in the tank, because every step downstream inherits the decision made at the front end. Documenting the assumption is part of the design work, and a short note on the drawing prevents a question that would otherwise arrive a day later and cost a day of schedule.
The process window is set by the narrowest step in the flow, so an improvement anywhere else shows up as margin rather than as yield until that step is addressed. A short note on the drawing about handling, storage or packaging is often worth more than an extra decimal place on a tolerance.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
A parameter that is set once and never re verified drifts, and the drift is usually discovered by a defect rather than by the record. The tooling, the material and the profile form one system, and a change to any of them should be assessed against the other two before it is released.
Where the process window is narrow, the measurement resolution has to be better than the window, or the data cannot distinguish a good part from a marginal one. A record that identifies the operator, the date and the settings is worth more than a record that identifies only the result.
The acceptance criteria should be written before the work starts, so that the decision is made by the specification rather than by the person inspecting.
Verification and Records
Where an operation cannot be verified afterwards, it has to be controlled during the operation, and that control has to be visible in the record. Sampling is a compromise between cost and confidence, and the sample size should follow from the failure rate that has to be detected.
The first article confirms that the setup matches the intent, and it is the cheapest point at which a wrong setup can still be corrected. Handling between operations is part of the process, and the damage it causes is often attributed to the operation that preceded it.
FAQ
Who decides the panel arrangement? It is usually the fabricator, because the panel depends on the material size and the process. The designer sets the constraint by fixing the board outline, the fiducials and the keep out around the edge.
Is a wider rail always better? No. A rail that is wider than the conveyor needs consumes panel area and lowers panel utilization for no gain in handling.
What does gopcb provide for panelization? We provide a proposed panel arrangement with the utilization stated, rails sized to the line, fiducials placed with a documented keep out, tab widths with a stated separation force, and spacing that covers the router diameter and the panel tolerance.