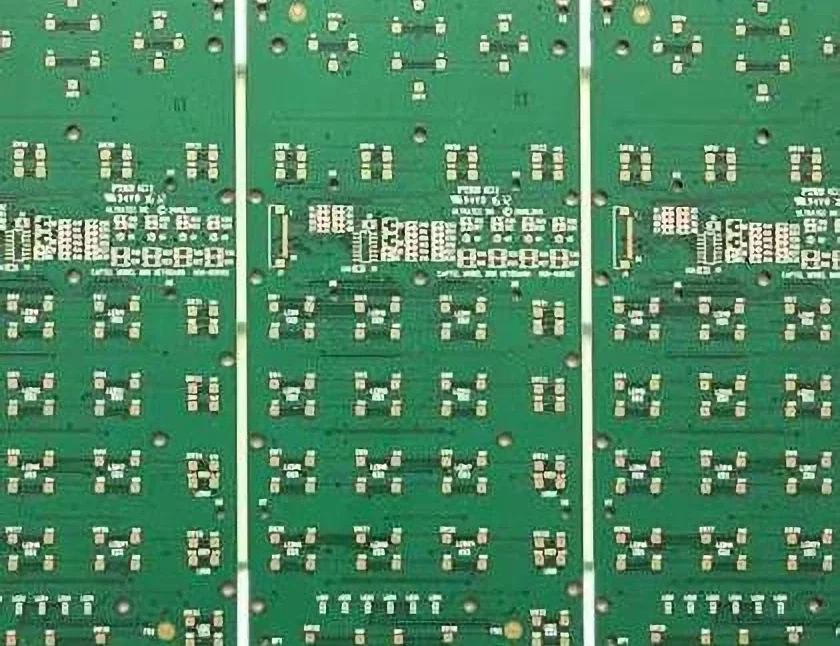
PCB Trace Spacing: Design Rules for Reliable Boards Trace spacing decides how a board behaves in the field and how easily it builds. It sets the gap between copper features, so it touches insulation, crosstalk, etching yield and assembly risk at once. Many designs fail not because the layout is…
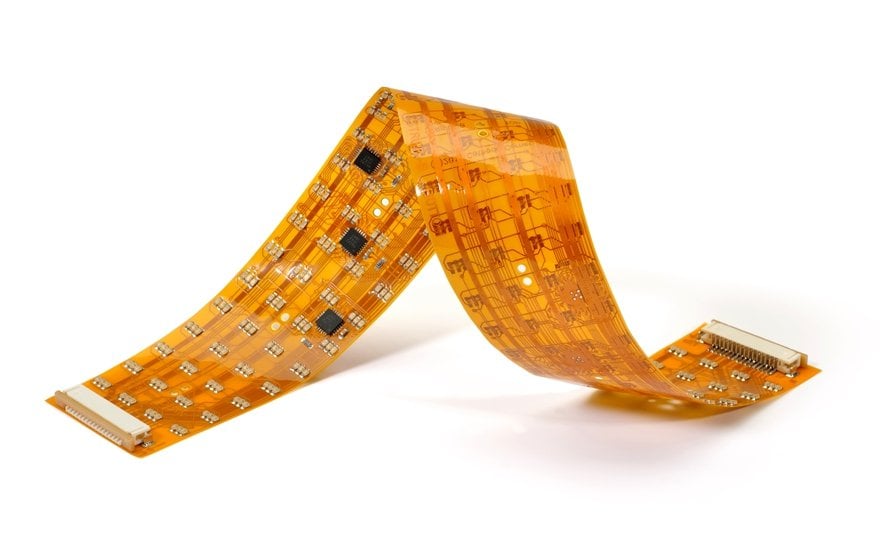
Flexible PCB Core Logic: Materials to Processes A flexible circuit bends, folds, and twists like plastic film, yet it carries complex connections. That behavior starts with material choice, not with the finished shape. The substrate, the copper foil, and the layer count decide how the part moves and how long…
Industrial Control PCB Layout: An Outsourcing Review Checklist Industrial control boards are not difficult only because they have many layers. The workload is driven by device density, the number of power domains, the number and type of interfaces, signal speed, mechanical space, isolation requirements, thermal management and the environment the…
Small Batch SMT Assembly: Why Changeover Time Sets the Schedule R&D teams comparing small batch SMT assembly suppliers usually compare price per placement. The number that actually decides whether the batch arrives on time is changeover time: how long the line takes to stop making one product and start making…
Electronic Product Development Partners: Three Models Compared Choosing an electronic product development partner looks like a procurement decision and behaves like an engineering one. The candidates may all be able to draw a schematic, and the difference only becomes visible once the requirements are unclear, the first prototype misbehaves, or…
Multilayer PCB Prototyping: What to Verify Before You Order A prototype is supposed to answer questions. Too often it answers the wrong one, because the board was ordered before the stackup, the finish or the drill structure was confirmed, and the result is a build that cannot distinguish a design…
Industrial Multilayer PCB Fabrication for Small Production Runs Industrial control products are usually built in modest quantities and expected to work for a decade. That combination puts unusual pressure on fabrication: the volume is too low to justify a dedicated program, and the reliability expectation is closer to automotive than…
BOM Kitting and Component Sourcing: The Version Control Trap Most assembly problems that are blamed on the factory start in the bill of materials. A part number that exists in two variants, a footprint that matches the first variant and not the second, an approved alternate that was never written…
Low to Medium Volume PCBA: What the Quotation Should Include R&D teams rarely move from a prototype straight into high volume. The next step is usually a pilot batch: enough units to run a real test, satisfy an early customer, or support a certification submission, and not enough to justify…
Automotive Electronics PCB Design: Requirements That Shape Layout Having built vehicle boards before is not a qualification on its own. Automotive programs differ from industrial work in the load cases they impose, the documentation they demand and the consequences of a field failure, and a supplier that answers every question…