

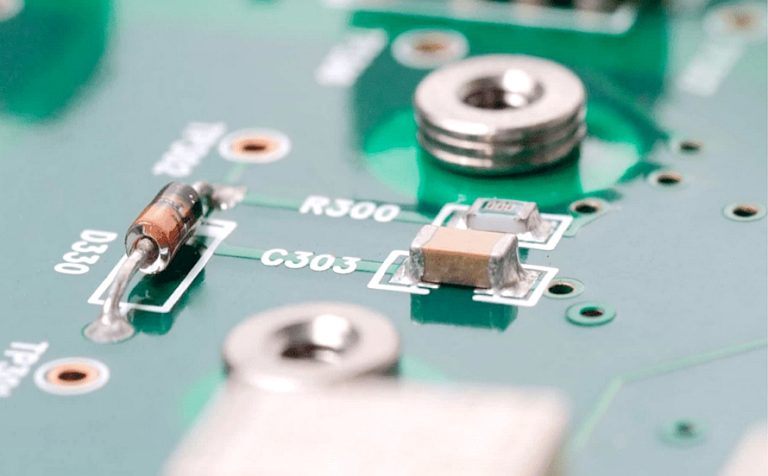
Reflow Soldering: PCB Design, PCB Manufacturing, Process, Profile & Defects
Reflow soldering is one of the most widely used processes for attaching electronic components to a printed circuit board (PCB). The process begins by applying solder paste to the appropriate PCB pads, followed by precise placement of surface-mount components. The PCB is then heated inside a reflow oven, causing the solder paste to melt and form reliable mechanical and electrical connections between the components and the board.
As a critical stage of SMT PCB assembly, reflow soldering directly influences the electrical integrity, mechanical reliability, and long-term performance of an electronic product. From tiny 0201 passive components to complex, high-density ball grid array (BGA) packages, properly controlled reflow soldering is essential for modern electronics manufacturing.
A reflow oven is the specialized equipment used to execute this process. Modern ovens contain multiple independently controlled heating zones that gradually raise and lower the PCB temperature according to a predefined thermal profile. This controlled heating process allows the solder paste to melt properly while minimizing thermal stress on components and the PCB.
In this guide, we explain how reflow soldering works, the major process steps, reflow temperature profiles, common technologies, defects, best practices, and the differences between reflow soldering and wave soldering.
What Is Reflow Soldering and How Does It Work?
Reflow soldering is an SMT assembly process that uses solder paste and a controlled heating profile to attach surface-mount devices (SMDs) to PCB pads.
Solder paste consists primarily of fine solder alloy particles suspended in flux. During PCB assembly, a stencil is used to deposit a controlled amount of solder paste onto the designated pads. A pick-and-place machine then positions the components accurately on the printed solder deposits.
The populated PCB subsequently enters the reflow oven. The oven gradually heats the assembly until the solder reaches its melting temperature. The molten solder wets the component terminals and PCB pads, forming solder joints. During the controlled cooling stage, the solder solidifies and creates a permanent electrical and mechanical connection.
Unlike processes involving uncontrolled heating, a properly designed reflow profile gradually changes the PCB temperature. This helps reduce thermal shock and minimizes the risk of component damage, solder defects, and PCB warpage.
The final solder quality depends on several factors, including:
- Solder paste composition and storage conditions
- Stencil aperture design
- Solder paste volume
- Component placement accuracy
- PCB pad geometry
- Reflow oven configuration
- Thermal profile
- PCB material and component thermal characteristics
Step-by-Step Reflow Soldering Process
A reliable reflow soldering result depends on a standardized sequence of processes and strict process control. A typical SMT production line follows the steps below.
1. PCB Cleaning
Before solder paste printing and component placement, the PCB surface should be sufficiently clean and free from contaminants.
Dust, grease, oxidation, moisture, and other contaminants can interfere with solder wetting and contribute to defects such as insufficient solder, poor adhesion, or open solder joints.
Depending on the application and contamination level, cleaning methods may include:
- Ultrasonic cleaning: Uses high-frequency sound waves to create microscopic bubbles in a cleaning solution.
- Aqueous cleaning: Uses water-based cleaning chemistry to remove contaminants.
- Solvent cleaning: Uses suitable solvents to remove oils, flux residues, and other contaminants.
The cleaning method must be compatible with the PCB materials, solder mask, surface finish, and components.
2. Solder Paste Printing
Solder paste printing is one of the most important steps in PCB Manufacturing and SMT assembly.
A stainless-steel stencil containing precisely defined apertures is positioned over the PCB. A squeegee then forces solder paste through the apertures and onto the PCB pads.
Stencil thickness, aperture dimensions, paste viscosity, printing pressure, printing speed, and separation characteristics all affect the amount of solder deposited.
An optimized stencil design helps maintain consistent solder volume and reduces defects such as solder bridges, insufficient solder, and component tombstoning.
3. Component Placement
After solder paste printing, a pick-and-place machine accurately positions SMD components onto the corresponding pads.
The tackiness of the solder paste temporarily holds the components in position before the PCB enters the reflow oven.
Placement accuracy becomes increasingly important as component sizes and pad pitches decrease. Incorrect component placement can result in:
- Component misalignment
- Tombstoning
- Open joints
- Solder bridges
- Polarity errors
- Poor contact between terminals and pads
For high-density assemblies, automated optical systems and machine-vision alignment help maintain placement accuracy.
4. Pre-Reflow Inspection
Before entering the reflow oven, the PCB can undergo inspection to verify that solder paste and components have been placed correctly.
Solder Paste Inspection (SPI) systems measure characteristics such as:
- Solder paste height
- Solder paste volume
- Paste area
- Offset
- Shape and coverage
Automated inspection can identify printing problems before they become permanent soldering defects.
5. Reflow Soldering
The populated PCB enters the reflow oven, where it passes through a series of controlled temperature zones.
The board is gradually heated, held at an appropriate temperature, brought above the solder alloy’s liquidus temperature, and then cooled.
A typical reflow process consists of four major thermal stages:
Preheating Zone
The PCB temperature gradually increases.
The primary purpose is to minimize thermal shock and prepare the PCB, components, and solder paste for subsequent heating.
Soak Zone
The PCB remains within a controlled temperature range for a specified period.
This stage allows the board and components to reach a more uniform temperature while activating the flux contained in the solder paste.
Reflow Zone
The temperature rises above the liquidus temperature of the solder alloy.
The solder particles melt, wet the PCB pads and component terminals, and form the solder joints.
The peak temperature and time above liquidus (TAL) must remain within the recommended limits of the solder paste and component specifications.
Cooling Zone
The temperature is gradually reduced.
The molten solder solidifies and forms the final mechanical and electrical connection. A controlled cooling rate helps reduce thermal stress and can influence the resulting solder-joint microstructure.
After the PCB exits the oven, flux residues may remain depending on the solder paste chemistry. Whether cleaning is required depends on the paste type and the product’s cleanliness requirements.
6. Post-Reflow Inspection and Testing
After reflow soldering, the assembled PCB undergoes inspection and testing to verify solder-joint quality and assembly accuracy.
Common inspection methods include:
- AOI (Automated Optical Inspection)
- AXI/X-ray inspection
- Electrical testing
- Flying-probe testing
- Functional testing
X-ray inspection is particularly useful for hidden solder joints, including those underneath BGA packages and other bottom-terminated components.
Reflow Soldering Temperature Profile
The reflow temperature profile describes the PCB’s temperature change as it passes through the different zones of the reflow oven.
The profile is one of the most important parameters in reflow soldering because excessive or insufficient heating can cause solder defects, component damage, PCB delamination, or poor solder-joint reliability.
Common profile types include the following.
Ramp-Soak-Spike (RSS)
In an RSS profile, the temperature initially rises at a controlled rate, enters a soak period, and then increases toward the peak reflow temperature.
The soak stage helps equalize PCB temperature and activate the flux before the board reaches the reflow stage.
Ramp-to-Spike (RTS)
In an RTS profile, the temperature generally rises continuously from the preheat stage toward the peak temperature without a long soak plateau.
This profile can provide a relatively straightforward thermal process when it is compatible with the solder paste and assembly requirements.
Custom Thermal Profiles
Different PCBs may require different thermal profiles because component sizes, PCB thickness, copper distribution, solder alloy, and thermal mass vary significantly.
For this reason, manufacturers should develop and verify the thermal profile for the actual PCB assembly rather than relying on a generic oven setting.
Thermal profiles should also be checked periodically because production conditions, equipment performance, and product configurations can change over time.
Common Reflow Soldering Technologies
Different heating technologies can be used in electronic manufacturing.
Convection Reflow
Convection reflow ovens use heated air to transfer thermal energy to the PCB.
This is one of the most common reflow methods because it provides relatively uniform heating and precise temperature control.
Modern convection ovens can use multiple independently controlled zones to create a repeatable thermal profile.
Infrared Reflow
Infrared reflow systems use infrared radiation to heat the PCB and solder paste.
The technology can provide rapid heating, but differences in material emissivity and component geometry can result in uneven heating. Modern production lines therefore often favor controlled convection systems for complex assemblies.
Vapor-Phase Reflow
Vapor-phase reflow uses the condensation of a specialized vapor to transfer heat to the PCB.
Because the condensation temperature is closely related to the working fluid’s boiling characteristics, the process can provide highly controlled thermal transfer and is useful for certain sensitive or complex assemblies.
Nitrogen Reflow
Nitrogen reflow introduces an inert nitrogen atmosphere into the oven.
Reducing oxygen concentration can minimize oxidation during soldering and improve wetting for some solder alloys and surface finishes.
Nitrogen may be particularly useful for demanding assemblies where oxidation control is important.
Best Practices for Reliable Reflow Soldering
Consistent reflow soldering requires careful control of materials, equipment, PCB design, and process parameters.
Optimize Stencil Design
Stencil apertures should be optimized according to the PCB pad geometry, component package, solder paste, and assembly requirements.
Industry guidance such as IPC-7525 can be used when developing stencil designs.
For fine-pitch components, aperture reduction and customized aperture geometries may be required to control solder volume and prevent bridging.
Maintain an Accurate Thermal Profile
The oven should be profiled using appropriate thermocouples and profiling equipment.
Important parameters include:
- Ramp rate
- Soak temperature
- Soak time
- Peak temperature
- Time above liquidus
- Cooling rate
The profile should be validated against the solder-paste manufacturer’s recommendations and component temperature limits.
Verify Component Placement
Pick-and-place machines should be calibrated regularly.
Accurate fiducial recognition, feeder setup, nozzle condition, and machine calibration all contribute to consistent placement quality.
Use High-Quality Solder Paste
Solder paste quality has a direct influence on printing performance and solder-joint reliability.
Manufacturers should control:
- Storage temperature
- Shelf life
- Exposure time
- Mixing conditions
- Paste viscosity
- Moisture exposure
Following the solder-paste manufacturer’s handling instructions is essential.
Control the Production Environment
Humidity, temperature, contamination, and storage conditions can affect solder paste and PCB assembly quality.
A controlled production environment can help maintain repeatable printing and reflow performance.
Common Reflow Soldering Defects and How to Prevent Them
Even experienced manufacturers can encounter soldering defects because reflow quality depends on multiple interacting variables.
Tombstoning
Tombstoning, also called the Manhattan effect, occurs when one end of a small passive component lifts from the PCB pad during reflow.
Potential causes include:
- Uneven heating
- Unequal solder paste volume
- Incorrect pad geometry
- Component placement offset
- Uneven wetting forces
Possible corrective actions include optimizing the pad design, balancing solder paste deposition, improving placement accuracy, and adjusting the thermal profile.
Cold Solder Joints
A cold solder joint can occur when the solder does not achieve adequate melting or wetting.
Possible causes include:
- Insufficient peak temperature
- Inadequate time above liquidus
- Poor thermal transfer
- Oxidized surfaces
- Contaminated pads
The thermal profile, solder paste condition, PCB surface finish, and component terminals should be checked when this defect occurs.
Solder Bridging
A solder bridge forms when molten solder connects two adjacent pads or terminals.
Common causes include:
- Excessive solder paste
- Poor stencil design
- Incorrect component placement
- Insufficient pad spacing
- Poor stencil alignment
Optimizing stencil apertures and printing parameters can significantly reduce the risk of solder bridging.
Solder Balls
Small solder spheres may form around solder joints during reflow.
Possible causes include:
- Improper solder-paste handling
- Excessive heating rate
- Incorrect thermal profile
- Excessive solder paste
- Contamination
Improving solder-paste storage and handling, optimizing stencil design, and controlling the reflow profile can help reduce solder-ball formation.
Voiding
Voids are gas-filled cavities inside solder joints.
Some level of voiding can occur naturally, but excessive voiding can reduce solder-joint mechanical reliability and thermal or electrical performance, especially in power components.
Stencil design, solder-paste selection, reflow conditions, pad design, and component package structure can all affect voiding.
Lead-Free Reflow Soldering for High-Density PCBs
Modern electronics manufacturing increasingly uses lead-free solder alloys to meet environmental and regulatory requirements.
Lead-free soldering can introduce additional process challenges because many lead-free alloys have higher melting temperatures than traditional Sn-Pb solder.
This means manufacturers may need to carefully manage:
- Peak temperature
- Time above liquidus
- Heating rate
- Cooling rate
- Flux activity
- Component temperature limits
- PCB thermal stress
HDI PCB assemblies introduce additional challenges because they typically contain fine lines, microvias, small pads, and high-density component layouts.
Modern HDI designs frequently use small SMD packages, making reflow soldering particularly important. The combination of smaller component packages, tighter pitches, complex thermal distribution, and limited board space requires careful coordination between PCB design and SMT process engineering.
Reflow Soldering vs. Wave Soldering
Reflow soldering is primarily associated with surface-mount technology, while wave soldering is traditionally used for through-hole technology.
| Factor | Reflow Soldering | Wave Soldering |
|---|---|---|
| Basic process | Solder paste is printed onto PCB pads and melted in a controlled oven. | The PCB passes over a wave of molten solder. |
| Primary application | Surface-mount components (SMDs) | Through-hole components (THTs) |
| Automation | Highly automated | Highly automated |
| Thermal method | Controlled heating zones | Contact with molten solder wave |
| Component compatibility | Excellent for SMD assemblies | Excellent for THT assemblies |
| Typical applications | High-density SMT PCB assembly | Through-hole and mixed-technology assemblies |
| Process control | Requires precise thermal profiling | Requires control of solder wave, fluxing, and preheating |
Many modern PCB assemblies contain both SMD and through-hole components. In such cases, manufacturers may combine reflow, selective soldering, and other assembly processes to meet the requirements of the complete product.
Applications of Reflow Soldering in Electronics Manufacturing
As electronic devices become smaller and more powerful, SMT components have become increasingly important. Reflow soldering enables manufacturers to efficiently attach large numbers of compact components to densely populated PCBs.
Common applications include:
Consumer Electronics
Smartphones, tablets, laptops, wearables, smart appliances, and other consumer products rely heavily on SMT assembly and reflow soldering.
Automotive Electronics
Automotive control modules, infotainment systems, driver-assistance electronics, instrument clusters, and other vehicle electronics require reliable PCB assemblies capable of operating under demanding environmental conditions.
Industrial Electronics
Industrial controllers, automation systems, power-control equipment, measurement instruments, and communication equipment commonly use reflow-soldered PCB assemblies.
Medical Electronics
Medical devices often require highly controlled PCB assembly processes because reliability and traceability are important considerations.
Telecommunications and Networking
Routers, switches, communication modules, servers, and other high-density electronic systems depend on precise SMT assembly and reliable solder joints.
How to Choose a PCB Assembly Partner for Reflow Soldering
Selecting an experienced PCB Assembly partner is an important part of achieving consistent reflow soldering quality.
When evaluating a manufacturer, consider the following capabilities:
Modern Reflow Equipment
The manufacturer should have modern reflow ovens with multiple independently controlled heating zones and reliable thermal-profile monitoring.
Automated Inspection
AOI, SPI, and X-ray inspection capabilities can help detect solder-paste and solder-joint defects at different stages of the assembly process.
High-Density PCB Experience
The manufacturer should have experience with fine-pitch components, BGA packages, QFN packages, 0201 components, HDI boards, and mixed-technology assemblies when required.
Process Standards
A qualified manufacturer should operate according to recognized industry standards and quality-management systems appropriate to the target application.
Examples may include:
- ISO 9001
- IPC-A-610
- IPC-7525
- IATF 16949 for applicable automotive manufacturing
- ISO 13485 for applicable medical-device manufacturing
- AS9100 for applicable aerospace manufacturing
Engineering Support
A capable assembly partner should be able to provide DFM feedback, stencil recommendations, thermal-profile development, component placement optimization, and defect analysis.
Why Choose Kingda for Reflow Soldering and PCB Assembly?
Kingda provides integrated PCB Manufacturing and PCB Assembly solutions for customers requiring reliable SMT production.
Our capabilities can support projects involving standard SMT components as well as fine-pitch and high-density assemblies. By combining PCB fabrication, component sourcing, SMT placement, reflow soldering, inspection, and testing, Kingda can help streamline the overall manufacturing process.
Our reflow soldering services focus on:
- Controlled solder-paste printing
- Accurate automated component placement
- Multi-zone reflow soldering
- Thermal-profile verification
- AOI inspection
- X-ray inspection for applicable assemblies
- Electrical and functional testing
- DFM and assembly engineering support
- Prototype and volume PCB assembly
For complex assemblies, proper coordination between PCB Design, PCB fabrication, stencil design, component placement, and reflow profiling can significantly improve manufacturing consistency.
Conclusion
Reflow soldering is a fundamental technology in modern SMT PCB assembly. It enables manufacturers to attach thousands of surface-mount components efficiently while achieving consistent mechanical and electrical connections.
A successful reflow process depends on much more than simply placing a PCB inside an oven. Solder-paste quality, stencil design, component placement, PCB pad geometry, oven configuration, thermal profiling, and inspection all contribute to final solder-joint quality.
For high-density and lead-free assemblies, process control becomes even more important. Small components, fine-pitch packages, BGA devices, HDI structures, and higher lead-free soldering temperatures require close coordination between PCB Design, PCB Manufacturing, and assembly engineering.
By selecting an experienced PCB assembly manufacturer with appropriate reflow equipment, inspection systems, process controls, and engineering expertise, manufacturers can improve assembly consistency, reduce soldering defects, and support reliable electronic products from prototype through mass production.