Rework Site Preparation and Pad Repair
Rework begins with the site, not with the component. A site that still carries the old solder, the old flux and the heat history of the previous assembly will not produce a joint as good as the original, whatever tool is used.
Removing the Old Solder
The old alloy has to be removed completely, because mixing two alloys produces a joint with a melting range and a structure that neither was qualified with. Wick and suction both work and both leave a residue.
The removal should be checked under magnification. Our joint criteria notes describe the acceptance that follows.
Flux and Cleaning
The flux used for removal has to be cleaned off before the new flux is applied, because two chemistries on one site behave unpredictably. The cleaning should be appropriate to the flux.
The residue is often the reason a rework joint voids. Our voiding notes describe the mechanism.
Preheat and Its Purpose
Preheat reduces the temperature the local tool has to supply and it reduces the thermal gradient across the board. A site that is not preheated is heated locally and the gradient is what damages laminate.
The preheat temperature is set below the solder melting point. Our rework heating notes describe the methods.
Laminate Damage
Excessive local heat produces a discoloured or lifted pad and, at the extreme, a blister in the laminate. The damage is cumulative, so the number of rework cycles at one site should be limited.
The limit should be written rather than left to the operator. Our laminate notes describe the behaviour that follows.
Pad Repair
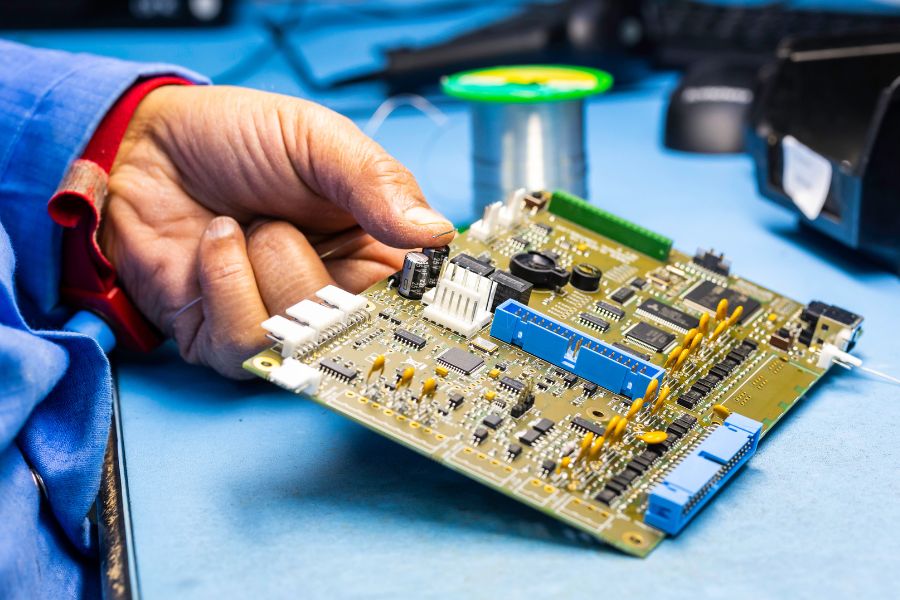
A lifted pad can sometimes be repaired with a bonded replacement or an epoxy and copper repair, and sometimes the repair is not acceptable for the product. The decision should be recorded.
The repaired site has to survive the same thermal exposure as the original. Our thermal cycling notes describe the test that confirms it.
Jumper Wires and Their Control
A jumper is a route, and it should be drawn and recorded rather than improvised. An unrecorded jumper is a defect that appears in the field as an unexplained continuity.
The record belongs with the assembly. Our design release notes describe the change control that covers it.
Verification
The verification is a site inspected under magnification after removal, a preheat temperature recorded, a limit on the number of cycles at one site, and a record of any pad repair or jumper with the person who performed it.
Our quality notes describe how the records are kept.
Process Control and Verification
Reviewing the design before the data is released is cheaper than correcting it after the panel is in the tank, because every step downstream inherits the decision made at the front end. Documenting the assumption is part of the design work, and a short note on the drawing prevents a question that would otherwise arrive a day later and cost a day of schedule.
The process window is set by the narrowest step in the flow, so an improvement anywhere else shows up as margin rather than as yield until that step is addressed. A short note on the drawing about handling, storage or packaging is often worth more than an extra decimal place on a tolerance.
Where a value sits close to a process limit, the drawing should say so, since the shop can then open the process window rather than working to a nominal figure that carries no tolerance. A stack-up that is drawn rather than described removes most of the ambiguity from a quotation, and it lets the fabricator price the board against the dielectric and copper weights that will actually be used.
Where the requirement is not written down, the shop supplies its own default, and the default is chosen for the process rather than for the design.
Checks Before Release
The checks that matter are the ones performed on the product rather than on a sample kept for the purpose, because a coupon that travels with the panel is the only evidence about that panel. Where a requirement can be measured, it should be measured at the point of manufacture and recorded against the board or the lot it applies to.
A parameter that is set once and never re verified drifts, and the drift is usually discovered by a defect rather than by the record. The tooling, the material and the profile form one system, and a change to any of them should be assessed against the other two before it is released.
Where the process window is narrow, the measurement resolution has to be better than the window, or the data cannot distinguish a good part from a marginal one. A record that identifies the operator, the date and the settings is worth more than a record that identifies only the result.
The acceptance criteria should be written before the work starts, so that the decision is made by the specification rather than by the person inspecting.
FAQ
Can the old solder be left in place? It can where the same alloy is used and the joint is reflowed fully, and it should not be where the alloy differs or where the joint is only partially melted.
Is a repaired pad as good as the original? It can be mechanically adequate, and it should be treated as a deviation that is recorded rather than as an equivalent.
What does gopcb provide during rework? We provide a site cleaned of the old alloy and flux before new material is applied, a preheat temperature recorded for the assembly, a written limit on cycles at one site, and a record of every pad repair or jumper with the operator and the method.