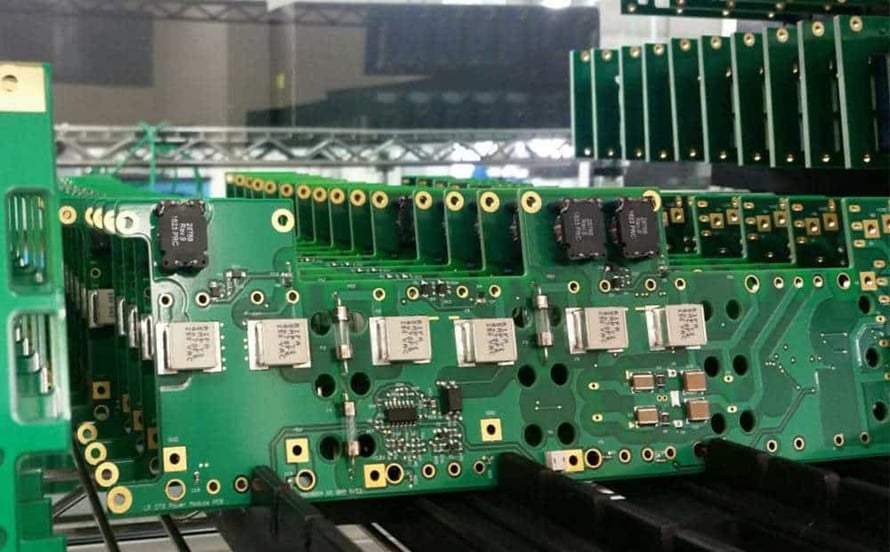
Panel Plating Thickness Distribution: Where the Copper Lands Panel plating is the step in which copper is deposited over the whole surface and through every hole of the panel before the outer layer pattern is defined. It builds the hole wall and the surface copper in one operation, and it…
Rinse Water Recycling: 4 Checks for a Clean Plating Line Rinse water recycling is the practice of treating the water that leaves a rinse stage and returning it to the line instead of sending it to drain. On a plating line it can cut consumption sharply, and it can also…
Nozzle Vacuum Setup: 6 Rules for Reliable Pickup Nozzle vacuum setup is the combination of air pressure, nozzle tip geometry and pickup height that lets a placement head lift a component from its pocket and hold it until the paste is reached. It is a small part of the machine,…
Acid Cleaner Concentration: 6 Rules for a Clean Surface Acid cleaner concentration is the strength of the acidic bath that removes oxide, fingerprints and light organic soil from a panel before plating, coating or lamination. The stage is short and inexpensive, and it is the one that decides whether every…
Shadow Plating and Throwing Power in PCB Plating Shadow plating is the local thinning of electroplated copper in areas that see less current than the rest of the panel. A bath can report a perfect surface thickness on a coupon while the wall of a small via stays barely covered,…
Reflow Thermal Uniformity and Delta T Control Thermal uniformity across a panel decides whether the profile that was validated on a coupon describes the parts that are actually being soldered. A large thermal mass next to a small package can hold a delta T of 15 °C or more, and…
Reflow Cooling Rate: Why the Cooldown Zone Matters Cooling rate is the slope of the temperature curve after the peak, and it is the part of a reflow profile that receives the least attention. The heating zones are specified in detail while the cooldown is often left to whatever the…
Solder Paste Transfer Efficiency in Stencil Printing Transfer efficiency is the number that tells you whether a stencil printing process is behaving: the paste volume deposited in an aperture divided by the theoretical volume of that aperture, expressed as a percentage. A line printing at 70 percent will produce intermittent…
Resin Starved Laminates: 7 Rules Against Fiber Show and Dry Spots A resin starved panel is one where there is not enough resin to fill the space between the glass fibres and around the copper features. The first sign is usually visual: the weave of the glass becomes visible through…
Prepreg Gel Time Control for Multilayer Lamination: 6 Rules Prepreg is glass fabric that has been impregnated with a resin which has been advanced to a partly cured state, known as the B-stage. In that state the resin is dry enough to handle and reactive enough to melt, flow and…