Multilayer FPC Structure: A Design and Manufacturing Guide
A multilayer FPC structure is what turns a flexible circuit from a simple ribbon into a functional assembly. Where a single sided flex carries power and a few signals between two fixed points, a multilayer construction adds power and ground planes, shielding and additional signal layers inside the same thin profile, which is what wearable devices, folding phones, medical instruments and robotic joints actually require.
The market reflects that shift. Global multilayer flexible circuit demand passed twenty billion dollars in 2025 and continues to grow at a rate near fifteen percent a year, led by medical devices, automotive electronics and consumer products. Understanding how the layers are arranged, and which of them limits reliability, is the difference between a flex that survives a hundred thousand bends and one that fails in the field.
The Outer Layer: Coverlay and Conductor
The outer surface is a coverlay laminated over the conductor pattern, usually polyimide between fifty and one hundred and twenty five micrometres thick. It protects the traces, provides mechanical support and, because polyimide tolerates temperatures from well below freezing to beyond two hundred and fifty degrees Celsius, it survives both reflow and the thermal environment of the product.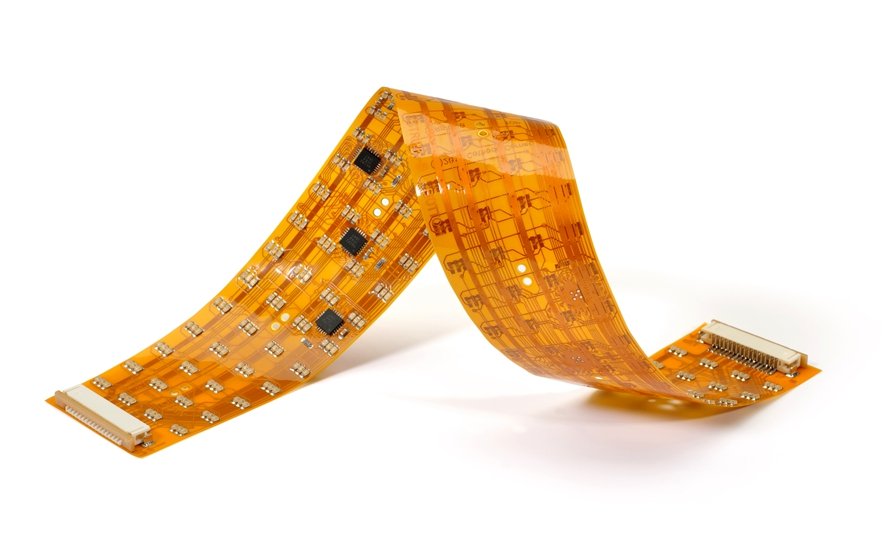
Copper choice on that layer matters as much as the dielectric. Electrolytic copper offers excellent conductivity and suits high frequency transmission, while rolled annealed copper has a grain structure that withstands repeated bending far better. A design that flexes in service should specify rolled annealed foil for the dynamic region and accept the higher cost, because grain boundaries in electrolytic copper become crack initiation sites after enough cycles.
Inner Layers Do the Electrical Work
Inside a multilayer structure the layers divide by function. Power and ground planes distribute current evenly and provide the return path that keeps electromagnetic emissions under control, which matters more in a flex than in a rigid board because the loop area is small and the conductors run close together.
Signal layers carry the differential pairs, clocks and high speed interfaces, typically with line widths around one tenth of a millimetre held to a tolerance of a few micrometres. Where radio frequency signals are present, a dedicated shield layer tied to ground at intervals reduces coupling to and from the outside world. That layer is also what allows a flex to pass near a metal chassis or a battery without picking up noise.
Adhesives, Adhesiveless Construction and Thickness
Older flex constructions bonded copper to polyimide with an acrylic adhesive. Adhesiveless laminates, built by casting or sputtering copper directly onto the film, remove that layer and with it several problems: they are thinner, they tolerate higher temperatures without the adhesive flowing, and they bend more predictably because there is no third material with different mechanical properties in the stack.
Thickness then becomes a design variable rather than a fixed outcome. Each additional layer adds copper, dielectric and bonding material, and the neutral bending axis shifts as the stack grows. For a dynamic application the designer wants the conductors close to that neutral axis so they experience minimum strain, which sometimes means adding a stiffening layer or adjusting the position of the thickest copper rather than simply minimising overall thickness.
Why Bending Is the Limiting Requirement
Flexible circuits fail in bending in a small number of recognisable ways. Copper cracks where the trace crosses the bend perpendicular to it, coverlay delaminates at the edge of the bend region, and plated through holes or vias crack if they sit inside the flexing area. All three are design issues before they are manufacturing issues.
The rules that avoid them are well established. Route conductors parallel to the bend axis wherever possible, keep vias out of the dynamic region or place them so they are not loaded, control the bend radius with the mechanical design rather than leaving it to assembly, and position the coverlay opening so that the transition from stiff to flexible happens gradually. A flex that is expected to survive more than a hundred thousand cycles usually needs those rules applied together, not selectively.
Layer Count and Its Costs
Adding layers solves routing congestion and improves electrical performance, but each layer increases lamination cycles, cost and the difficulty of maintaining registration. In flexible circuits the penalty is larger than in rigid boards, because the material is thin and moves more during processing, and because a misregistration that would be tolerable on a rigid panel can place a via at the edge of its pad on a flex.
Experienced designers therefore start from the requirement rather than the layer count. If the flex needs a controlled impedance path for a high speed interface, it needs a reference plane, and that usually settles the question. If it is carrying power and slow signals across a hinge, a smaller stack with careful mechanical design is normally more reliable than a thicker one. Discussing the stack up with a manufacturer who builds flexible circuit capability during the layout stage avoids building thickness that the product does not need.
Rigid-Flex as an Extension of the Same Idea
Many products no longer separate the flexible interconnect from the rigid board. A rigid flex design laminates rigid sections, which carry the dense components, with flexible sections that cross the moving joint, using the same base materials throughout. That removes connectors, improves reliability and saves the height that a connector pair would occupy.
The trade is manufacturing complexity, because the rigid and flexible regions have different mechanical behaviour under lamination and must be processed so that the transition zone is controlled. Designers must define where the flex region begins, keep the stack symmetrical around the neutral axis in that region, and avoid placing vias or large copper areas at the boundary. Working with a partner who also handles flexible circuit assembly keeps those decisions consistent between the board and the finished assembly.
Applications That Drive the Structure
Wearables use multilayer flex to connect displays, sensors and batteries in a package with almost no spare volume. Folding phones use rigid flex across the hinge, where the circuit must survive repeated opening and closing while carrying high speed display and camera data. Medical devices use it in catheters and imaging probes, where thinness and repeatable flexing are clinical requirements rather than product features.
Automotive applications are growing fastest of all, because cameras, radar modules and battery monitoring systems sit in locations where a conventional harness is bulky, heavy or unreliable. In each of these cases the structure follows the mechanical requirement: how much it moves, how many signals it carries and how much electrical noise it must tolerate. That is why layout decisions and mechanical design are normally reviewed together on a flex programme.
Shielding in a Thin Package
Electromagnetic compatibility is harder to manage in a flexible circuit than in a rigid board, because the conductors are close together and the assembly often sits next to a battery, a display or an antenna. A dedicated ground layer with stitching vias around the perimeter of sensitive regions is the usual answer, and it has to be planned in the stack up because retrofitting shielding to a flex means adding a layer.
The same structure also carries return currents for high speed interfaces. Because flex circuits have limited copper area, a poorly planned return path can raise impedance or create a loop that radiates, which is why designers now treat flex routing as a signal integrity problem rather than a wiring exercise.
Stiffeners and Terminations
Where a flexible circuit connects to a rigid board or is soldered to a component, a stiffener is normally added to provide mechanical support and to control where bending begins. The stiffener material, usually polyimide or a thin metal, changes the local thermal expansion and the soldering behaviour of the region, so its placement interacts with the assembly process.
Terminations deserve attention because they are where flexible circuits most often fail in production rather than in service. Connector pads need adequate support, anchorage and appropriate surface finish, and the transition from the stiffened region into the moving region should be gradual. Deciding this during layout, rather than after the first assembly attempt, is what keeps a flex programme on schedule.
Cost Drivers in a Multilayer Flex
Cost in a multilayer flex is driven by layer count, material choice, registration difficulty and the number of lamination cycles, not by area alone. Rolled annealed copper, adhesiveless laminates and tight tolerance specifications each add cost, and their value depends on whether the product actually needs them.
The most common source of unnecessary cost is specifying flexibility everywhere. A circuit that bends in one small region does not need the same construction across its entire length, and a mixed design, with a dynamic region specified for bending and static regions built for density, is usually cheaper and no less reliable. Reviewing that split with the manufacturer before tooling is the single most effective cost reduction available on a flex programme.
What to Check Before Release
Before a multilayer flex design is released, four questions deserve an explicit answer. Where is the neutral axis in the bend region, and are the critical conductors near it? Does the coverlay opening match the mechanical bend? Are vias and plated holes outside the dynamic area? And does the specified copper type match the number of cycles the product must survive?
If those answers are documented, the remaining risk sits in manufacturing consistency: registration, lamination and plating repeatability across production. That is the part a supplier controls, and it is why buyers should ask for process data on comparable products rather than for the thinnest flex ever produced. A reliable flexible circuit is the product of a well chosen structure and a manufacturer that repeats it consistently.