Many hardware engineers attribute gold thickness uniformity entirely to the PCB manufacturer’s plating process. However, PCB layout, copper distribution, pad geometry, and panelization can also influence the plating environment and amplify local variation.
A design that creates significant differences in exposed surface area, copper distribution, panel position, or solution accessibility may increase the difficulty of maintaining consistent immersion-gold thickness. These risks are often less obvious during prototype production because the sample size is small. Once the design enters high-volume manufacturing, the same structural characteristics are repeated across large numbers of panels, making process variation much more visible.
For this reason, PCB DFM should not focus only on routing, trace width, impedance, and electrical clearance. For ENIG surface finishing, DFM should also consider exposed copper distribution, pad geometry, panelization, tooling areas, and measurement locations.
A well-designed panel can reduce process sensitivity before the boards reach the plating line, making it easier to maintain stable ENIG process control during mass production.
1. How Copper Distribution Can Affect Gold Thickness Uniformity
Immersion gold is a chemical deposition process in which gold is deposited on the exposed nickel surface through a displacement reaction. Therefore, the distribution and geometry of exposed nickel areas, together with solution chemistry, temperature, agitation, mass transfer, and process time, can influence local deposition behavior.
When a PCB contains very large exposed pads in one region and numerous small isolated pads in another, the local surface-area distribution can be significantly different. This may contribute to differences in chemical exchange and local reaction conditions.
However, it is important not to treat copper density alone as a direct predictor of immersion-gold thickness. The actual result depends on the complete surface-finish process, including copper preparation, nickel plating, exposed pad geometry, bath chemistry, fluid dynamics, and panel configuration.
Therefore, PCB DFM optimization should address both copper distribution and the distribution of exposed finish areas.
1.1 Use Dummy Copper to Improve Overall Panel Balance
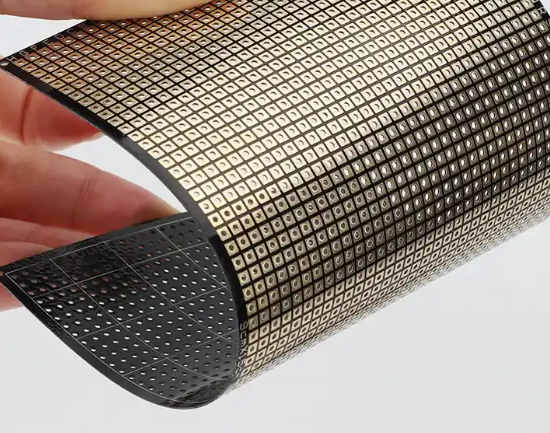
Dummy copper can be used in appropriate areas to improve overall panel copper balance and reduce large differences in copper density during upstream PCB manufacturing processes.
For example, grid-style dummy copper may be added to relatively open areas while remaining covered by solder mask. Such copper does not become an additional ENIG pad because it is not exposed for nickel and gold deposition.
Its primary benefits are related to improving overall copper distribution and manufacturing stability in processes such as copper plating, etching, and lamination. A more balanced panel can also make subsequent surface-finish processing more predictable.
When using dummy copper, designers should consider:
- Keep dummy copper within the PCB manufacturer’s DFM capability.
- Maintain adequate clearance from functional traces, pads, and controlled-impedance structures.
- Avoid creating unintended capacitive coupling or electromagnetic coupling.
- Avoid unnecessarily exposing dummy copper for ENIG.
- Consider the impact of dummy copper on copper balance, thermal behavior, and manufacturability.
- Confirm the proposed pattern with the PCB manufacturer before production release.
Dummy copper should therefore be regarded as a panel and manufacturing-balance tool rather than a universal solution for immersion-gold thickness variation.
1.2 Avoid Excessive Copper-Thickness Differences Within One PCB
A PCB may combine heavy-copper power areas with conventional signal layers. Large differences in copper thickness and copper distribution can create different manufacturing conditions during etching, surface preparation, and plating.
When such structures are unavoidable, critical areas such as BGA pads, fine-pitch pads, and high-reliability soldering locations should receive additional attention during process validation and gold thickness measurement.
The purpose is not necessarily to make every part of the PCB physically identical, but to identify regions where geometry or process conditions may increase variation risk.
2. Pad Size, Geometry, and Layout Optimization
Pad geometry is another important factor in controlling gold thickness uniformity.
Large exposed pads have a different surface-area-to-perimeter relationship from small pads. Local solution exchange, boundary-layer behavior, and the surrounding copper and solder-mask pattern can therefore differ between large and small features.
For very large exposed areas, the center and edge may also experience different local chemical conditions. The actual magnitude of this effect depends on the plating system and process parameters, so it should be verified through measurement rather than assumed from geometry alone.
2.1 Avoid Unnecessarily Large Continuous ENIG Areas
Where electrical and mechanical requirements permit, extremely large continuous exposed areas should be reviewed during PCB DFM.
For example, a large grounding area may sometimes be divided into several functional pad regions with solder-mask separation. This can reduce the size of individual exposed areas and create a more controlled pad structure.
The final design must still satisfy electrical, thermal, assembly, and mechanical requirements. Pad segmentation should not be introduced solely for plating considerations if it negatively affects grounding, current capacity, thermal transfer, or solder-joint design.
2.2 Pay Attention to Isolated Small Pads
Small isolated pads surrounded by large areas of solder mask can have different solution-access conditions from larger, more open pad groups.
These pads should be identified as potential risk locations during design review. If they are critical functional pads, they should be included in the XRF inspection plan during prototype and mass-production validation.
Rather than applying a universal spacing or pad-size rule, the appropriate geometry should be confirmed against the PCB manufacturer’s actual process capability.
2.3 BGA Regions Require Special Attention
BGA arrays are particularly important because the internal pads of a dense array can have different surrounding geometries from pads located around the perimeter.
For this reason, BGA regions should be included in gold thickness measurement plans.
Where practical, designers should also consider:
- BGA position relative to the panel edge
- Local copper density
- Nearby large copper areas
- Solder-mask configuration
- Panel orientation
- Tooling and handling locations
- Accessibility for XRF measurement
The objective is not to claim that a BGA must always be placed at a particular location, but to prevent the BGA region from becoming an unmonitored process-risk area.
3. Panelization and Its Influence on Production Uniformity
Panelization can have a significant effect on how individual PCBs are positioned within a manufacturing panel.
A PCB located near the outer edge of a panel may experience different solution-flow conditions from a PCB located closer to the center. The magnitude and direction of this effect depend on the plating equipment, panel orientation, rack or fixture configuration, agitation, circulation, and chemical process.
Consequently, panel design should be validated rather than assuming that every position on the panel has identical plating conditions.
3.1 Use Process Rails to Manage Edge Effects
A process frame or rail can separate functional boards from the immediate panel boundary and provide space for tooling, handling, and process features.
Where appropriate, additional non-functional structures can be incorporated into the process frame to help manage panel-level manufacturing behavior.
The exact rail width should be determined by the PCB manufacturer’s equipment and tooling requirements rather than applying one universal value to every factory.
Eliminating process rails solely to maximize material utilization can sometimes increase manufacturing sensitivity, particularly when the product already has demanding surface-finish uniformity requirements.
3.2 Evaluate V-Cut and Tab-Routing Structures
V-Cut and tab-routing structures change the physical geometry of the panel and may affect local mechanical behavior, tooling, handling, and, depending on the equipment, the process environment around the boards.
Critical pads should therefore be kept away from areas where panel separation, tooling, or mechanical stress may create additional risks.
For tab-routed or perforated panels, connection points should also be reviewed carefully. Critical BGA or fine-pitch regions should not be placed unnecessarily close to high-stress separation features.
The final arrangement should be verified through the manufacturer’s panelization and process review rather than assuming that every V-Cut or tab location produces the same plating effect.
3.3 Avoid Mixing Highly Different PCB Structures on One Panel
Combining PCBs with substantially different dimensions, copper distributions, thicknesses, or exposed surface areas on one panel can make process behavior more complicated.
For high-volume projects, using boards with compatible specifications within the same panelization scheme can make process control and statistical analysis easier.
When mixed panelization is necessary, the manufacturer should evaluate the complete panel structure during DFM review and verify representative locations through XRF inspection.
4. Tooling and Clamping Locations Must Be Defined in DFM
Tooling and clamping areas should be considered during the panel design stage.
If a fixture or clamp physically covers an active pad, that area may have restricted chemical access or may become unavailable for normal processing. This can result in local surface-finish defects or create an area that cannot be measured reliably.
The process frame should therefore include dedicated tooling areas whenever required.
Before production release, designers and manufacturers should confirm:
- Fixture or clamp locations
- Tooling-hole positions
- Process-frame dimensions
- Product-edge clearances
- Areas unavailable for plating
- XRF measurement accessibility
- Depanelization requirements
These details should be included in the PCB DFM review instead of being determined only after the production panel has been created.
5. Define Gold Thickness Uniformity Requirements in the Specification
A common quality-control problem occurs when a drawing specifies only nominal gold thickness but does not define how gold thickness uniformity should be evaluated.
For example, specifying a nominal thickness range without defining measurement locations, sampling methodology, or allowable spatial variation can lead to different interpretations between the PCB manufacturer and customer.
For high-reliability or high-volume projects, the fabrication specification should clearly define:
- Required nickel thickness.
- Required gold thickness.
- Applicable thickness tolerance.
- Measurement method.
- Sampling plan.
- Measurement locations.
- Criteria for evaluating board-to-board and within-board variation.
- Additional requirements for critical areas such as BGA pads.
Multi-Point XRF Inspection
XRF inspection is commonly used for non-destructive measurement of PCB surface-finish thickness.
A single measurement point should not automatically be treated as representative of the entire PCB.
A risk-based measurement plan may include:
- Board edge
- Board center
- BGA peripheral pads
- BGA internal pads
- Large pads
- Small isolated pads
- Representative panel positions
For critical products, the inspection data can be statistically analyzed to evaluate minimum and maximum values, distribution, and process variation.
If significant differences are found between locations, the sampling scope should be expanded before accepting the entire production lot.
6. DFM Self-Inspection Checklist for ENIG PCB Projects
Before releasing a high-volume ENIG design, engineers can use the following PCB DFM checklist:
- Evaluate copper distribution across the complete panel.
- Identify areas with significant copper-density differences.
- Review large continuous exposed ENIG areas.
- Check isolated small pads and fine-pitch regions.
- Identify BGA regions as high-priority measurement locations.
- Review the PCB position within the panel.
- Confirm process-frame and rail requirements.
- Review V-Cut and tab-routing locations.
- Keep tooling and clamping areas away from functional pads.
- Avoid unnecessary mixing of substantially different board structures on one panel.
- Define gold thickness uniformity requirements in the fabrication specification.
- Define a multi-point XRF inspection and sampling plan.
- Validate the panel design during prototype or pilot production.
- Compare XRF data by board position and panel position before mass production.
7. From Design Optimization to Mass-Production Control
DFM optimization should not stop when the fabrication files are released. A more effective approach is to establish a complete control loop:
Design review → panelization review → prototype validation → XRF inspection → process capability assessment → mass production → SPC monitoring → incoming inspection → failure analysis
During prototype production, representative locations should be measured to determine whether the expected distribution is consistent with actual manufacturing results.
During mass production, the manufacturer can monitor process data and identify trends before variation becomes a large batch-level problem.
If abnormal gold thickness uniformity is detected, the investigation should compare:
- PCB design
- Panel position
- Copper distribution
- Pad geometry
- Surface-finish chemistry
- Equipment conditions
- Process timing
- XRF measurement data
- Production batch records
This approach helps distinguish a design-related issue from a plating-process issue and prevents repeated trial-and-error adjustments on the production line.
Conclusion
Gold thickness uniformity in ENIG PCB production is influenced by more than the immersion-gold bath itself. PCB layout, exposed pad geometry, copper distribution, panelization, tooling, and measurement strategy can all affect how effectively the manufacturing process maintains consistent results.
Effective PCB DFM therefore needs to consider surface-finish manufacturability from the beginning of the design cycle. By balancing copper distribution, reviewing pad geometry, optimizing panel structures, protecting tooling areas, and defining multi-point XRF inspection requirements, engineers can reduce process sensitivity before mass production begins.
For demanding high-volume applications, Kingda can support ENIG PCB projects with DFM review, panelization optimization, surface-finish process control, inspection, and production validation to help establish a more stable and traceable manufacturing process.